


Explore our core range of engineered storage equipment manufactured in our Shandong production facilities, designed for global 3PL, cold chain, and industrial logistics.

Semi-automated deep-lane pallet storage powered by remote-controlled battery shuttles. Maximize space utilization with FIFO/LIFO flexibility.
View Product Details
Direct factory supply of heavy-duty shuttle racking channels engineered with high-rigidity Q355B steel rails for high-throughput logistics hubs.
China Shuttle racking (also known as shuttle racking) Manufacturer, Factory
Multi-tier heavy-duty structural platforms expanding vertical clear space for manual picking, office space, and automated sorting zones.
China Mezzanine Racking (Mezzanine Shelving / Steel Platform Racking) Factories, Factory
Custom structural steel platform framing supporting extreme floor loads from 300kg/m² up to 1,500kg/m² with bolted modular connections.
China Steel Platform Racks (Steel Structure Platforms) Factories, Factory
Maximum density storage for homogeneous batch products. Forklifts enter racking lanes directly on cantilevered support rails.
View Drive In Racking
Nested cart system allowing 2 to 6 pallets deep storage per lane with automatic gravity feeding and front aisle accessibility.
View Push Back Racking
Motorized heavy-duty racking bases sliding on floor rails to eliminate static aisles, doubling warehouse capacity within existing footprints.
View Mobile Racking
Engineered cantilever structures designed for long, bulky, or irregular loads such as steel pipes, timber, aluminum extrusions, and sheets.
View Special Purpose RackingAs global industrial real estate costs escalate and labor availability tightens, modern logistics facilities are undergoing a fundamental architectural evolution from manual and semi-automated storage to fully dynamic 3D omnidirectional automation.
Traditional 2D radio shuttles operate strictly in linear, single-lane tracks, requiring manual forklift intervention to transfer vehicles between storage levels and channels. A modern 4-Way Pallet Shuttle eliminates this physical constraint. By integrating longitudinal and transverse travel mechanisms directly inside the vehicle chassis, a 4-way shuttle navigates across storage lanes, cross-aisles, and vertical elevator shafts independently.
By removing standard forklift aisles and crane operation zones required by conventional AS/RS stacker cranes, 4-Way Shuttle systems achieve up to 90% cubic spatial utilization. Furthermore, because individual shuttles weigh significantly less than multi-ton AS/RS stacker cranes, operational energy consumption drops by 50% to 70%, creating a green, decarbonized warehouse framework.
Traditional stacker cranes tie aisle storage capacity directly to throughput. In a 4-Way Shuttle system, storage capacity (racking racks) and throughput capability (number of shuttles and elevators) are completely decoupled. Facility managers can start with a baseline fleet and dynamically inject additional shuttles into the racking grid as order volumes scale up.
Guake Logistics Technology engineers comprehensive 4-way automated storage platforms built upon four foundational technical pillars: precision kinematics, intelligent energy management, decentralized WCS algorithms, and ultra-tolerant structural racking.
The core mechanism of a 4-way shuttle features a dual-axis wheel assembly powered by high-torque brushless DC servo motors. Directional switching between longitudinal main channels and transverse sub-channels is executed via a synchronized mechanical eccentric lifting structure in under 3.5 seconds. Multi-sensor positioning (laser distance meters, barcode positioning, and photoelectric sensors) guarantees millimeter-accurate stopping tolerances (+/- 2mm) under maximum payload (up to 1,500 kg).
Modern industrial 4-way shuttles utilize high-discharge Lithium Iron Phosphate (LiFePO4) battery packs paired with supercapacitor hybrid energy storage. Integrated kinetic energy recovery systems (KERS) harvest power during deceleration. Automatic sliding contact or non-contact wireless inductive charging stations installed within cross-aisles allow continuous 24/7 operation with 45-minute fast-charging cycles during low-throughput windows.
The intelligence of a China 4-way shuttle cluster lies in its Warehouse Control System (WCS). Utilizing dynamic path planning algorithms (A* and Dijkstra variants), dynamic task allocation, and real-time obstacle avoidance, the WCS coordinates hundreds of shuttles concurrently. Automatic traffic congestion avoidance, cross-aisle balancing, and single-shuttle failure failover routines ensure zero system bottlenecks.
Unlike standard static pallet racking, racking structures engineered for 4-way shuttle operation act as structural guidance tracks for robotic vehicles. Guake enforces strict structural manufacturing tolerances: upright column deflection ratio limits held to under L/200, track rail joint step tolerance < 0.5mm, and overall rack perpendicularity within +/- 1mm per 10 meters of height. This precision prevents wheel wear, shuttle derailment, and sensor misalignment over decades of high-speed travel.
A quantitative breakdown evaluating density, performance, capital investment, and operational resilience across high-density storage technologies.
| Performance / Feature Metric | 2D Radio Shuttle Racking | 4-Way Intelligent Shuttle System | AS/RS Crane System | Selective Pallet Racking |
|---|---|---|---|---|
| Volumetric Storage Utilization | High (75-80%) | Ultra-High (85-92%) | High (70-85%) | Low (35-45%) |
| Pallet Access Selectivity | LIFO / Lane-wise FIFO | 100% Individual Pallet Access | 100% Individual Access | 100% Direct Access |
| System Redundancy (No Single Point Failure) | Low (Forklift dependent) | Ultra-High (Modular Shuttle Swapping) | Very Low (Crane failure halts aisle) | N/A (Manual operation) |
| Energy Efficiency Ratio | Moderate | Extreme (LiFePO4 + KERS + Lightweight) | Low (Heavy moving mass) | N/A (Forklift fuel/electric) |
| Cold Storage Operating Range | -20°C to +45°C | -30°C to +45°C | -25°C to +40°C | Unrestricted |
| CAPEX / Throughput Scalability | Rigid | Fully Decoupled & Infinite Scaling | Fixed Aisle Bound | Linear |
Tailored 4-way automated racking solutions optimized for specific industry parameters, thermal conditions, compliance standards, and SKU velocity profiles.
In low-temperature food and pharmaceutical cold stores, building volume and power costs are premium variables. Guake 4-Way Shuttles utilize specialized low-temperature alloy gears, anti-freezing synthetic lubricants, and internal heating circuits for optical sensors. High cubic density minimizes cold air volume loss, cutting refrigeration compressor power consumption by up to 38%.
High-volume fast-moving consumer goods require intense batch handling. By configuring double-deep 4-way shuttle channels integrated with high-speed vertical reciprocating conveyors (VRCs), facilities can achieve outbound sorting speeds exceeding 250 pallets per hour per elevator bank, providing smooth buffering between production lines and outbound shipping doors.
Strict track-and-trace mandates require total batch isolation and zero contamination risk. Our stainless steel and electrostatic powder-coated shuttle systems interface directly with client SAP/WMS environments via encrypted Wi-Fi 6 / 5G industrial networks, preserving real-time inventory lineage and full auditability.
Located in Linyi, Shandong—China's premier industrial steel fabrication and logistics hub—Guake Logistics Technology leverages localized material vertical integration, robotic manufacturing, and rigorous quality engineering.
Guake directly sources structural carbon steel coils from Tier-1 state-owned steel producers (BaoSteel, Shougang Group). All upright profiles and heavy-duty load-bearing tracks undergo tensile, yield, and impact testing to guarantee compliance with international structural steel standards (ASTM A1011, EN 10025).
Our 20,000+ m² facility operates automated continuous cold-roll forming production lines equipped with inline laser punching systems. Upright profiles receive precise pitch hole patterns (+/- 0.1mm tolerance), ensuring rapid, binding-free installation of rack beams, guide rails, and shuttle track cross-bracing.
Critical structural connections, track joining flanges, and shuttle chassis frames are fabricated using multi-axis ABB robotic welding units. Surface finishing utilizes a 9-stage pre-treatment wash followed by thermosetting electrostatic epoxy powder coating, delivering corrosion resistance tested beyond 500 hours of salt spray exposure.
For international procurement directors, general contractors, and supply chain consultants, evaluating a China 4-Way Shuttle project requires analyzing Total Cost of Ownership (TCO) over a 10-year asset lifecycle.
Partnering directly with a China manufacturer like Guake reduces initial equipment acquisition costs by 35% to 50% compared to European or North American automation integrators without sacrificing component reliability (Schneider electronics, Siemens PLCs, Omron sensors, SEW drive motors).
Automating pallet movement reduces forklift driver headcounts, cuts warehouse damage to racking uprights (as forklifts remain outside storage blocks), and slashes facility lighting and HVAC load. Typical global ROI payback horizons range between 1.8 to 2.8 years.
Guake provides comprehensive Factory Acceptance Testing (FAT) and Site Acceptance Testing (SAT) protocols. Every shuttle system undergoes full-load dynamic cycling, wireless network telemetry validation, emergency stop safety testing, and rail alignment laser verification prior to final sign-off.
Ensuring flawless integration with local building codes, structural engineering standards, and worldwide after-sales field support.
Our structural designs strictly conform to international engineering standards, including European Standard EN 15512, FEM 10.2.09 (Pallet Racking Design), ANSI/RMI MH16.1 (USA), and CE Machinery Directive compliance for electrical vehicles.
Every Guake 4-way shuttle is equipped with an integrated IoT telemetry gateway. Our engineering center in Shandong provides remote diagnostic monitoring, firmware updates, and predictive maintenance alerts to prevent un-scheduled system downtime.
All wearable components (polyurethane drive wheels, sensor heads, relays) utilize modular quick-swap designs. We maintain localized spare parts hubs and partner with local installation crews across North America, Europe, Southeast Asia, and the Middle East.
Technical, operational, and financial answers addressing common search intents for buyers evaluating China 4-way shuttle manufacturers.
A 2-Way Radio Shuttle can only move linearly back and forth along a single dedicated rack channel; moving it to another channel or level requires a forklift operator or stacker crane. In contrast, a 4-Way Intelligent Shuttle possesses dual drive wheel sets allowing it to travel along both longitudinal storage lanes and transverse cross-aisles independently. Combined with vertical elevator lifts, a 4-way shuttle can autonomously navigate across the entire 3D storage matrix without human or forklift intervention.
Standard Guake 4-Way Shuttles are engineered to handle unit pallet loads ranging from 500 kg up to 1,500 kg. Standard pallet footprints supported include 1200x1000mm (UK/Asia standard), 1200x800mm (Euro pallet), and 48x40 inch (GMA North American standard). Custom shuttle chassis can be fabricated for non-standard industrial containers or extra-wide payloads.
Cold-storage version shuttles feature sealed IP65 electrical enclosures, low-temperature resistant Lithium Iron Phosphate (LiFePO4) battery chemistries with internal thermal management wraps, specialized synthetic gear greases, and stainless steel structural hardware. Optical sensors utilize anti-condensation micro-heaters to maintain millimeter positioning accuracy in freezing temperatures.
The system is controlled via Guake's proprietary Warehouse Control System (WCS), which manages real-time shuttle traffic, path optimization, elevator sequencing, and charging management. The WCS seamlessly interfaces with your enterprise Warehouse Management System (WMS) or ERP (e.g., SAP, Oracle, Manhattan, Infor) via standard REST APIs, WebSockets, or Modbus TCP protocols.
The system features built-in dynamic redundancy. If a shuttle reports an error, the WCS automatically routes surrounding shuttles away from the obstructed lane to maintain operational flow. A secondary shuttle can be commanded in manual recovery mode to tow or push the disabled vehicle to an inspection platform located at an outer maintenance bay, preventing facility-wide downtime.
Because the racking structure serves directly as the physical track for high-speed automated vehicles, tolerances are dramatically tighter than static pallet racks. Guake utilizes automated cold-roll forming and robotic welding to maintain track levelness within +/- 0.5mm, rail joints under 0.8mm, and rack verticality within L/200, ensuring smooth wheel travel and zero sensor misalignment over millions of cycles.
Typical factory production lead times for racking structural steel components and shuttle vehicle assembly are 30 to 45 days following approval of CAD layout drawings. Ocean shipping, on-site assembly, and WCS software commissioning generally require an additional 4 to 8 weeks depending on facility scale and regional location.
Discover our comprehensive suite of industrial racking, mezzanine platforms, and automated storage hardware configured directly by Guake Logistics Technology.

Standard high-bay selective pallet racking providing 100% direct selectivity for heavy industrial pallet storage with adjustable beam levels.
Explore Product Catalog
Heavy-duty structural mezzanine systems expanding floor space vertically for small-parts picking, packing zones, or administrative offices.
View Mezzanine Systems
Modular light-to-medium duty steel shelving engineered for rapid assembly, workshop organization, and commercial store inventory.
View Metal Shelving
Unobstructed arm racking system optimized for storing long pipes, timber, metal profiles, and sheet materials safely.
View Cantilever Racking
Precision snap-fit boltless steel shelving units providing versatile hand-load storage across e-commerce fulfillment centers.
View Boltless Shelving
Multi-tier shelf structures designed for high-density carton storage, bin picking, and automated tote handling integration.
View Multi-Layer Shelving
Heavy-duty structural steel platforms creating additional usable floors inside industrial plants without building expansion.
View Steel Platform Racks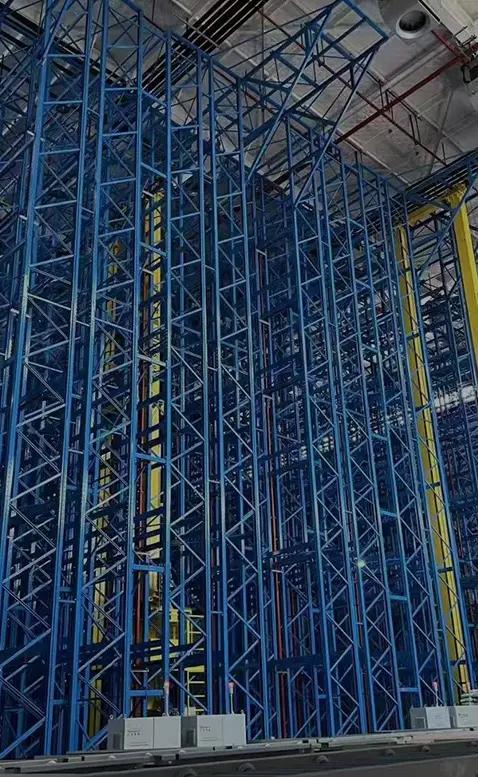
Ultra-tall precision steel racking frameworks custom manufactured to support automated stacker crane AS/RS integration.
Explore AS/RS Racking