


As a primary manufacturer in Shandong, China, Guake Logistics Technology engineers customizable heavy-duty storage configurations built to international structural standards.

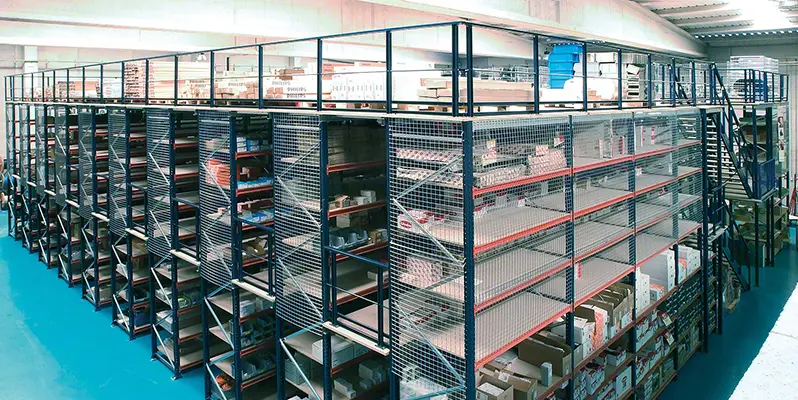
Multi-tier mezzanine shelving & structural steel platform racks manufactured for high vertical expansion.

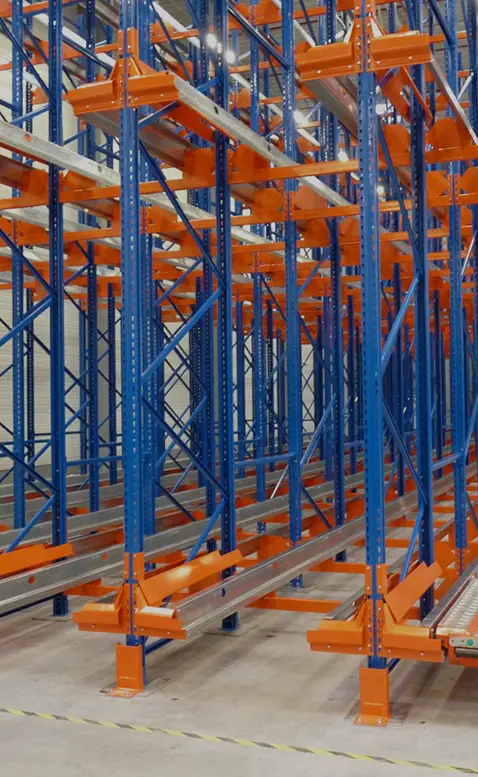
Semi-automated radio shuttle pallet runner system engineered for deep lane high-throughput storage.

Heavy-duty structural steel platforms optimizing overhead space for industrial work floors and logistics.

Motorized mobile base racking systems maximizing storage density while preserving 100% pallet access.

Maximum cubic utilization continuous rail racking ideal for bulk homogeneous inventory and cold storage.

Nested cart dynamic storage operating on inclined rails for 2 to 5 deep pallet LIFO inventory management.

High-density semi-automated channel storage supporting both FIFO and LIFO operational workflows.

Custom cantilever and specialized structural frames engineered for non-standard, long, or heavy items.
Modern industrial logistics faces an unprecedented real estate crisis. As land costs rise and urban cold-chain storage demands expand, traditional static pallet racking systems—which dedicate up to 60% of total floor space purely to access aisles—are rapidly becoming financially inefficient.
A Mobile Racking System (also designated as Electric Mobile Pallet Racking or Motorized Racking) transforms rigid storage design by mounting conventional pallet racks onto heavy-duty motorized carriages. These mobile bases travel along precision-machined floor guidance rails embedded into the concrete slab. By shifting entire rack blocks laterally, only one single working aisle needs to be open at any given moment for forklift access.
As an industry-leading manufacturer, Guake Logistics Technology integrates state-of-the-art automation and IoT architectures into mobile racking design. Here is our technical evolution roadmap driving the smart logistics revolution:
Future-proof mobile carriages feature integrated micro-PLC controllers linked via industrial Wi-Fi or 5G private networks. Real-time telemetry continuously monitors weight distribution, motor thermal loads, rail alignment, and structural vibration profiles.
Transitioning from manual forklift handling to fully automated operations. Mobile rack control cabinets interface directly with Autonomous Mobile Robots (AMRs) and Automated Guided Forklifts via OPC-UA protocols, opening specific aisles autonomously as the AGV approaches.
By combining Mobile Racking with Warehouse Control Software (WCS), systems execute dynamic aisle pre-opening algorithms based on batch picking orders, minimizing waiting times and optimizing internal material throughput speeds.
Multi-channel photoelectric safety light curtains, optical proximity sensors, dynamic emergency stop bumpers, and automated seismic anti-tilt locks protect operating personnel and cargo integrity under high-intensity usage.
In cold-chain applications down to -30°C, the WCS triggers an automated "night-park" ventilation mode, creating uniform air circulation gaps between mobile carriages to prevent cold thermal pockets and save up to 40% in refrigeration power.
Guake’s standardized base chassis allows plug-and-play addition of mobile wheel units and electrical control modules, enabling enterprises to expand rack lengths seamlessly as business throughput scales.
Different industrial sectors require tailor-made storage architectures. Guake Logistics Technology designs specialized mobile racking configurations tailored to vertical-specific challenges:
Refrigerated warehouse space carries the highest cost per cubic meter due to insulation and power overheads. Mobile racking minimizes unconditioned space volume, offering maximum pallet storage within compact freezer shells.
Handling heavy stamping dies, engine blocks, and automotive body parts demands exceptional beam rigidity and high wheel load support on floor guides.
Pharmaceutical storage requires strict batch control, cleanroom environment compliance, and FEFO (First-Expired, First-Out) picking protocols.
Hazardous chemical containment requires explosion-proof electrical fittings, strict aisle isolation, and integrated emergency containment systems.
Headquartered in Linyi City, Shandong Province—China’s premier industrial and logistics hub—Guake Logistics Technology (Shandong) Co., Ltd. operates over 20,000 m² of modern manufacturing facilities. Since 2010, our facility has combined advanced automation with strict raw material control:
We exclusively utilize high-tensile Q235B and Q355B structural steel supplied directly by China's leading state-owned steel mills (Baosteel, Shougang Group). Every steel coil undergoes mill test verification for yield strength and tensile endurance.
Our continuous 18-stage cold-roll forming production lines yield upright profiles with high geometric accuracy, minimizing internal stress vectors and guaranteeing precise beam-connector lockouts under full design loads.
Automated ABB robotic welding stations execute seamless joints across mobile carriage channels and structural guide units, followed by an automatic 9-stage thermosetting epoxy powder coating line for long-term corrosion resistance.
Procurement directors evaluating high-density storage choices must balance Initial Capital Expenditure (CAPEX) against long-term Operational Expenditure (OPEX). Below is an analytical Total Cost of Ownership (TCO) model comparing building expansion versus mobile racking integration:
| Financial & Operational Metric | Option A: New Building Expansion | Option B: Guake Mobile Racking System | Procurement Advantage |
|---|---|---|---|
| Required Facility Footprint | 10,000 m² (Standard Selective) | 5,500 m² (Mobile Racking) | 45% Land Footprint Saved |
| Real Estate & Civil CAPEX | $6,000,000 ($600/m²) | $3,300,000 ($600/m²) | $2.7M CAPEX Reduction |
| Annual Heating/Cooling OPEX | $480,000 / year | $264,000 / year | 45% Energy Cost Saved |
| SKU Selectivity & Direct Access | 100% Direct Access | 100% Direct Access | Parity with Selective Racking |
| Average Project Payback (ROI) | 7 - 10 Years | 14 - 22 Months | Rapid Capital Return |
Overseas racking deployments require strict adherence to local structural engineering codes, electrical safety directives, and on-site assembly standards. Guake provides complete engineering backing for international compliance:
Our mobile racking designs fully meet European Safety Standards EN 15095 for power-operated mobile storage and FEM 10.2.07 design codes, ensuring seamless pass rates during localized safety audits.
Guake dispatches specialized structural installation engineers worldwide to supervise rail alignment, floor flatness verification (TR34/DIN 18202 standards), electrical wiring commissioning, and local labor training.
We furnish finite element structural analysis (FEA) reports signed and stamped by certified Professional Engineers (PE) to satisfy municipal building permits across North America, Europe, Australia, and the Middle East.
Choosing the right racking configuration requires balancing cubic storage density, pallet selectivity, operational flow, and capital investment. Use this engineering matrix to evaluate system trade-offs:
| Racking Architecture | Storage Density | Pallet Access | Inventory Flow | CAPEX Cost | Primary Industrial Use-Case |
|---|---|---|---|---|---|
| Selective Pallet Racking | Baseline (100% Aisles) | 100% Direct | FIFO / LIFO | Lowest | High SKU count, general distribution centers |
| Mobile Racking System | Maximum (+85-100%) | 100% Direct | FIFO / LIFO | Medium-High | Cold storage, expensive land, high density + selectivity |
| Drive-In Racking | Very High (+60-75%) | Per Lane Only | LIFO | Low-Medium | Bulk homogeneous items, seasonal raw materials |
| Push Back Racking | High (+40-50%) | Lane Face (2-5 deep) | LIFO | Medium | Medium SKU counts, fast picking face buffer |
| Radio Shuttle Racking | Very High (+70-80%) | Channel Access | FIFO / LIFO | Medium-High | Deep lane cold storage, beverage bottling plants |
| Mezzanine Steel Platform | Vertical Footprint Boost | Manual / Lift | Flexible | Medium | Small-parts picking, e-commerce, office addition |
Read our latest technical insights authored by Guake’s senior logistics engineering team regarding high-density racking upgrades:
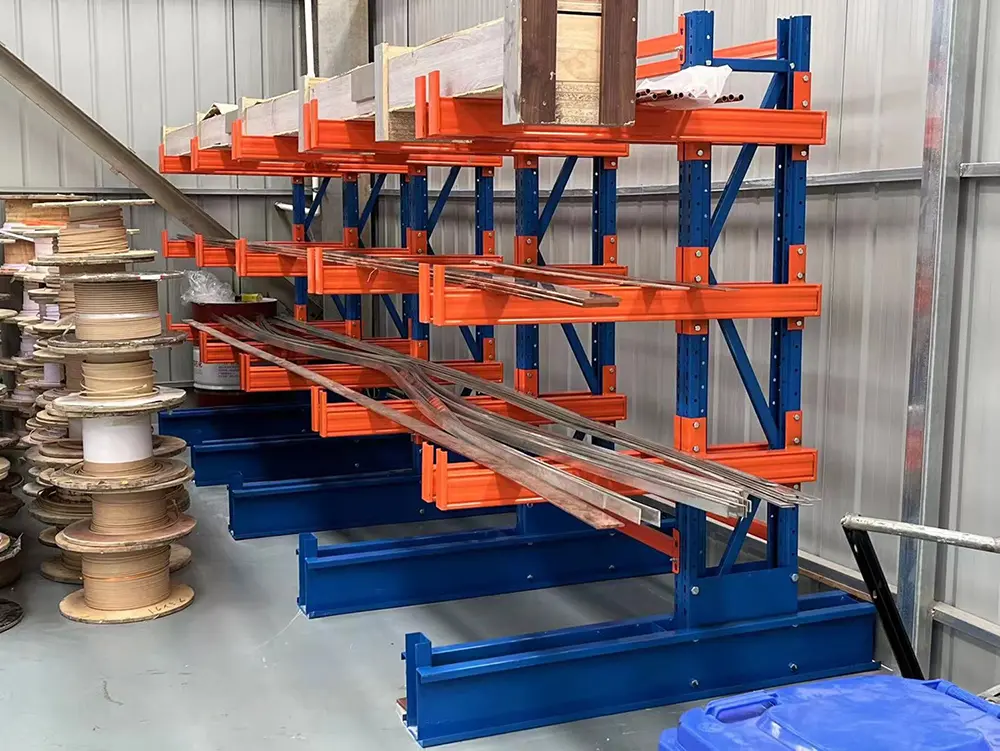
Why logistics operators combine dense pallet lanes with dynamic flow racking to balance storage capacity with picking throughput.
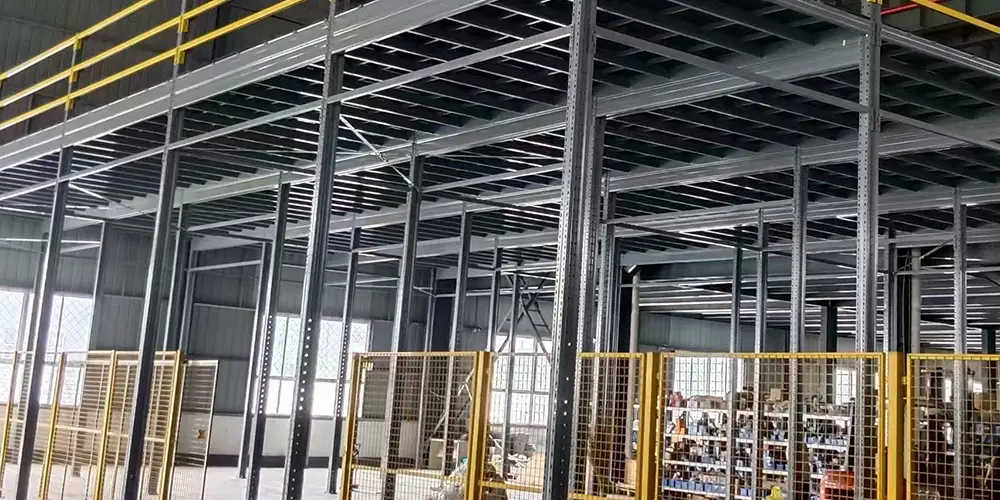
How vertical structural platforms and cantilever systems unlock unused cubic volume without extending building footprints.
Engineering considerations for heavy-duty structural steel racking operating in sub-zero refrigerated logistics hubs.
Maximizing vertical building clear height to store cylindrical rolls and specialized unit loads systematically.
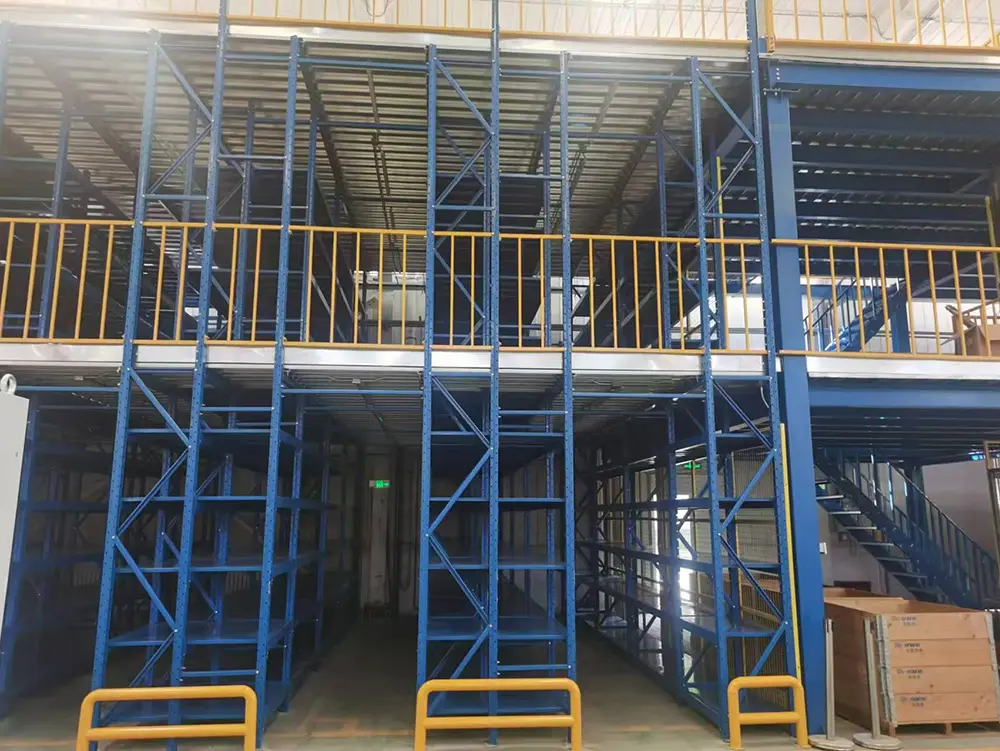
Evaluating beam profiles, structural connectors, and cart nesting mechanisms for optimal safety and capacity.
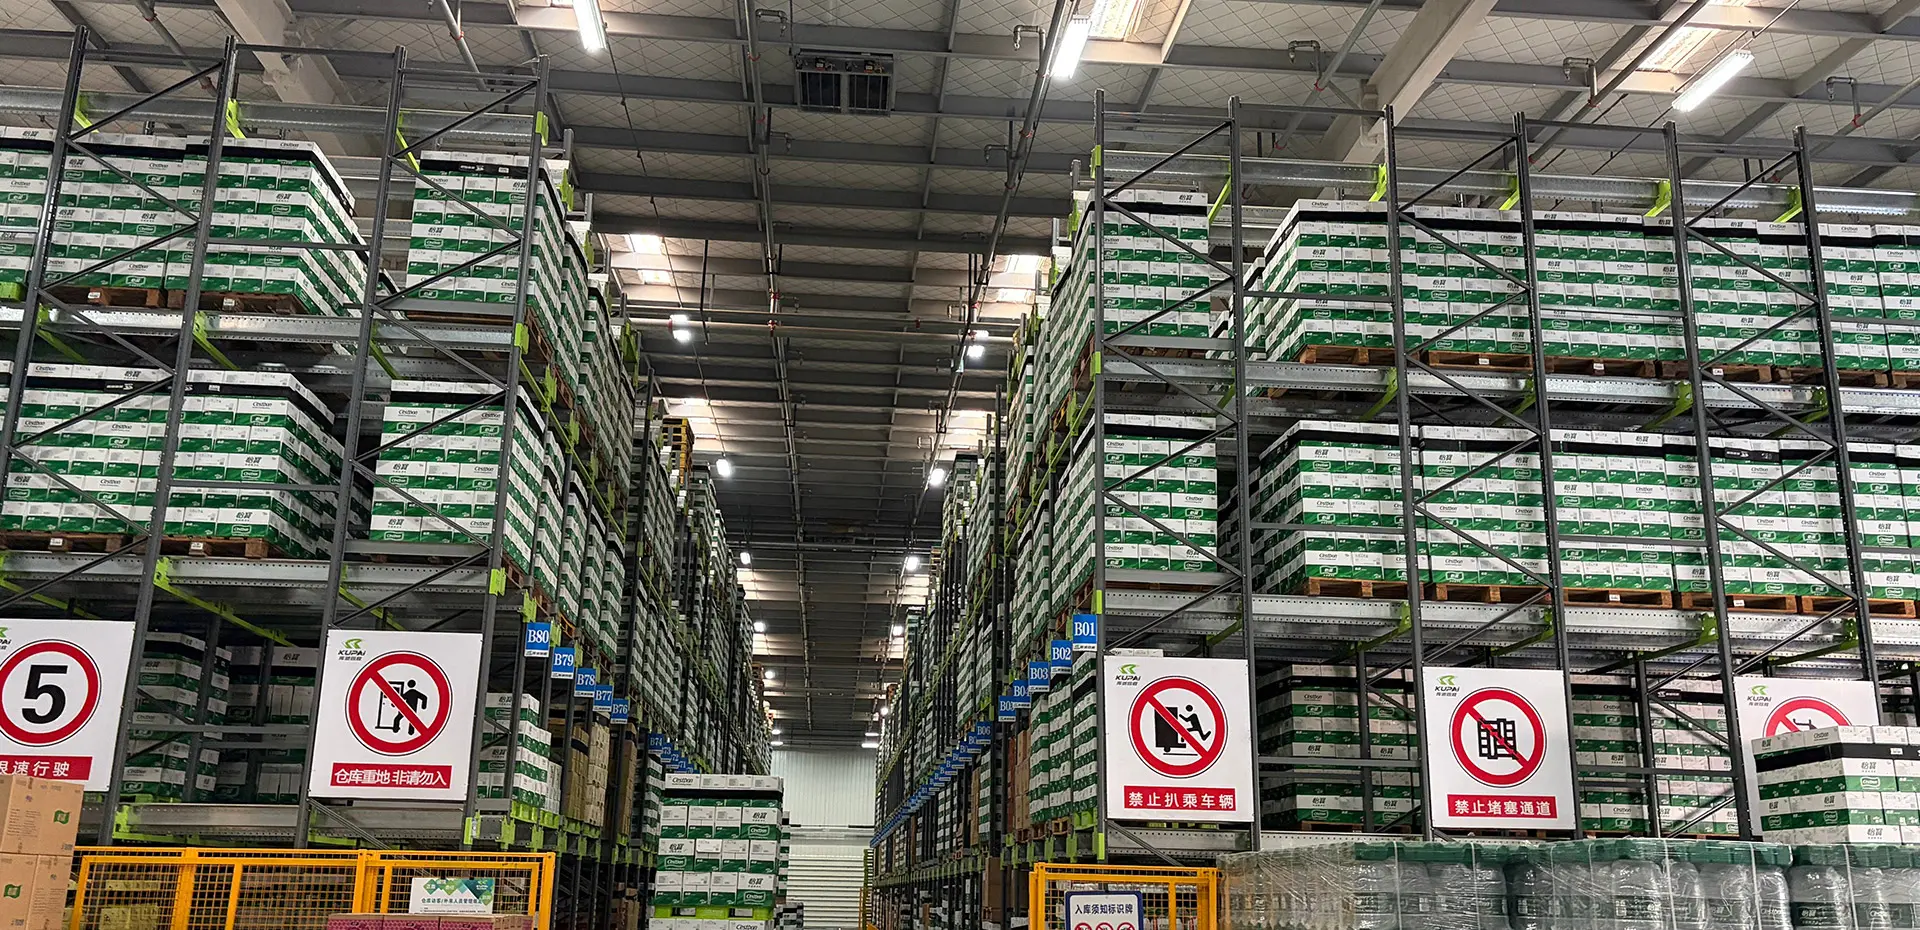
When automated storage and retrieval systems deliver maximum ROI, and how to plan modular migration paths.
Detailed technical responses to the questions most frequently posed by global warehouse engineers, project consultants, and procurement managers:
Guake Logistics Technology manufactures a full range of industrial storage equipment, including:
Yes. Our in-house engineering team provides end-to-end engineering layouts free of charge. Simply submit your CAD or PDF building floor plans, clear internal height measurements, pallet load dimensions (LxWxH), unit weight per pallet, forklift model specifications, and required hourly throughput.
System selection depends on your SKU count, required speed, and selectivity balance:
Yes. Every international project comes with detailed 3D installation drawings, exploded component lists, and step-by-step guidance videos. For turn-key projects, we dispatch certified installation supervisors and commissioning technicians globally to manage on-site erection and electrical integration. Learn more on our Global Service portal.
Quality and load structural safety are validated through multiple protocols: structural Finite Element Analysis (FEA) compliant with FEM and RMI standards; certified Q235B/Q355B raw steel sourcing; ISO 9001 quality system monitoring; ultrasonic weld inspection; and factory load testing of beam-column assemblies prior to export dispatch.
Yes. Customization is standard at Guake. Upright heights, frame depths, beam spans, beam connector configurations, powder coating RAL colors, decking materials (steel panels, wire mesh, timber), and mobile base drive motor specs are fully tailored to your exact application.
Mobile racking systems apply concentrated line loads via the guide rail wheels. Floor slabs generally require a minimum compressive strength of 30 N/mm² and must meet flat-floor tolerance standards such as DIN 18202 or TR34 FM2. Guake provides precise wheel load calculation sheets to your civil contractor prior to rail installation.
Guake mobile racking electrical cabinets can be integrated with an auxiliary uninterruptible power supply (UPS) or backup facility generator interface. In emergency power-loss scenarios, manual mechanical release levers allow operators to release the motor brake and hand-crank carriages to open essential picking aisles.
System design utilizes low-maintenance brushless gearmotors and direct-drive wheel assemblies. Recommended preventative maintenance includes quarterly cleaning of floor guide channels, checking optical safety sensors, and annual inspection of wheel bearing grease and PLC wiring terminals.
Yes. Guake designs custom seismic mobile racking equipped with mechanical anti-tilt floor retainers, top-guide stabilization tracks, and acceleration-sensing emergency stop relays that immediately lock carriages in position during seismic motion events.
Our Siemens or Schneider PLC control architectures support standard industrial communication protocols (EtherNet/IP, Modbus TCP, OPC-UA). This allows your Warehouse Management System (WMS) or ERP (e.g., SAP, Manhattan) to trigger automated aisle movements directly from forklift terminal scans.
Standard manufacturing lead times at our Shandong plant range from 3 to 5 weeks depending on project scale. Shipping via Qingdao Port provides direct ocean container routes to Europe, North America, Southeast Asia, and the Middle East in 15 to 35 days.
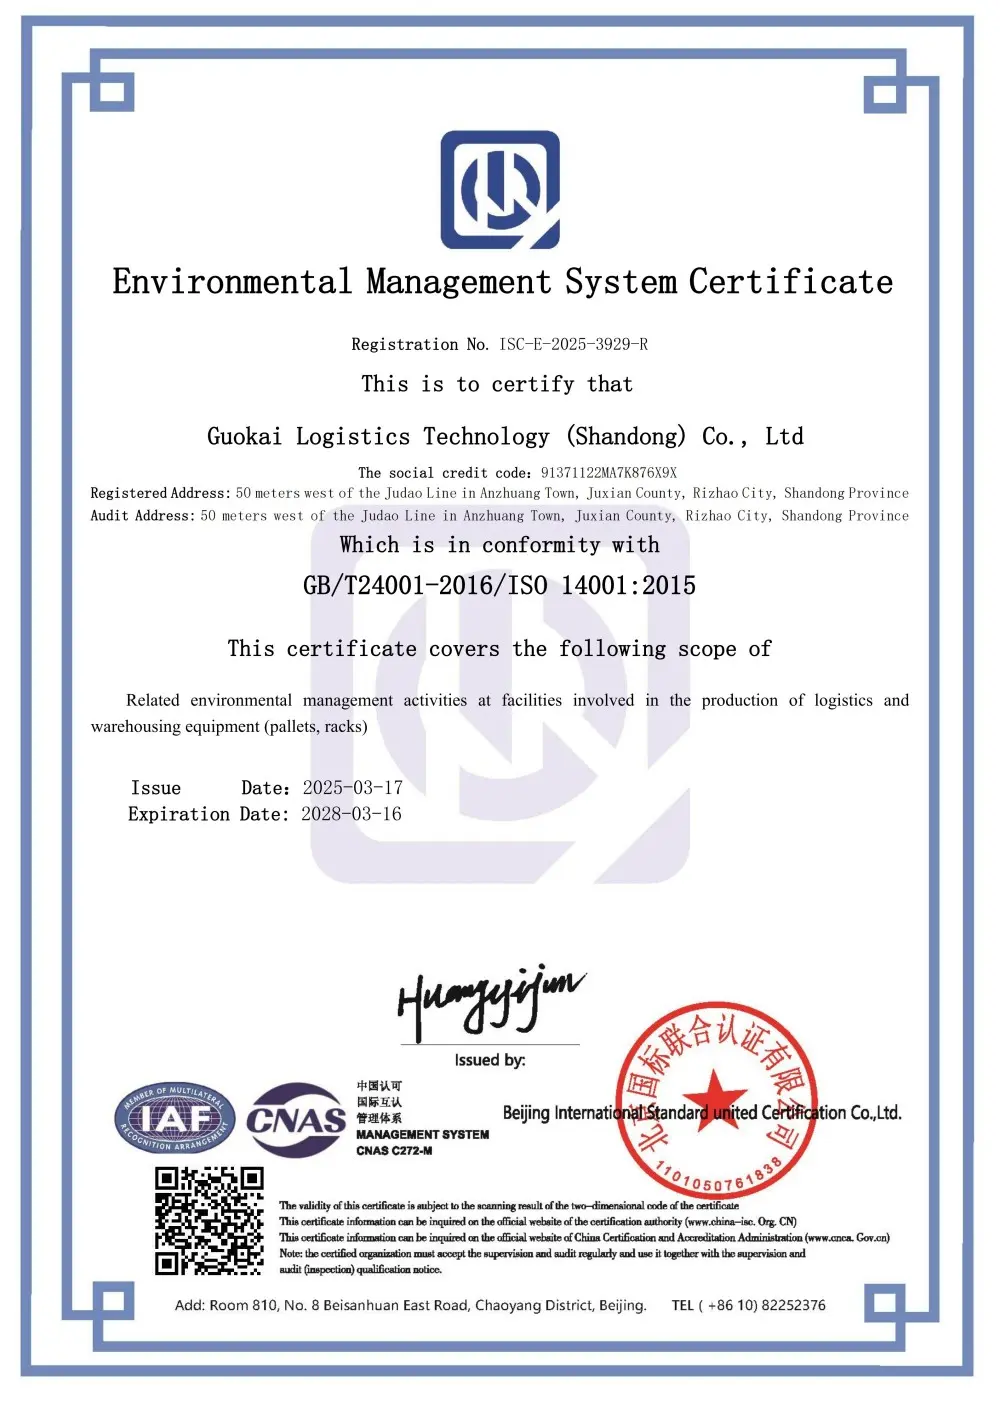
Guake operates under certified ISO 9001 and ISO 14001 management systems, maintaining long-term supply partnerships with global enterprise logistics networks:
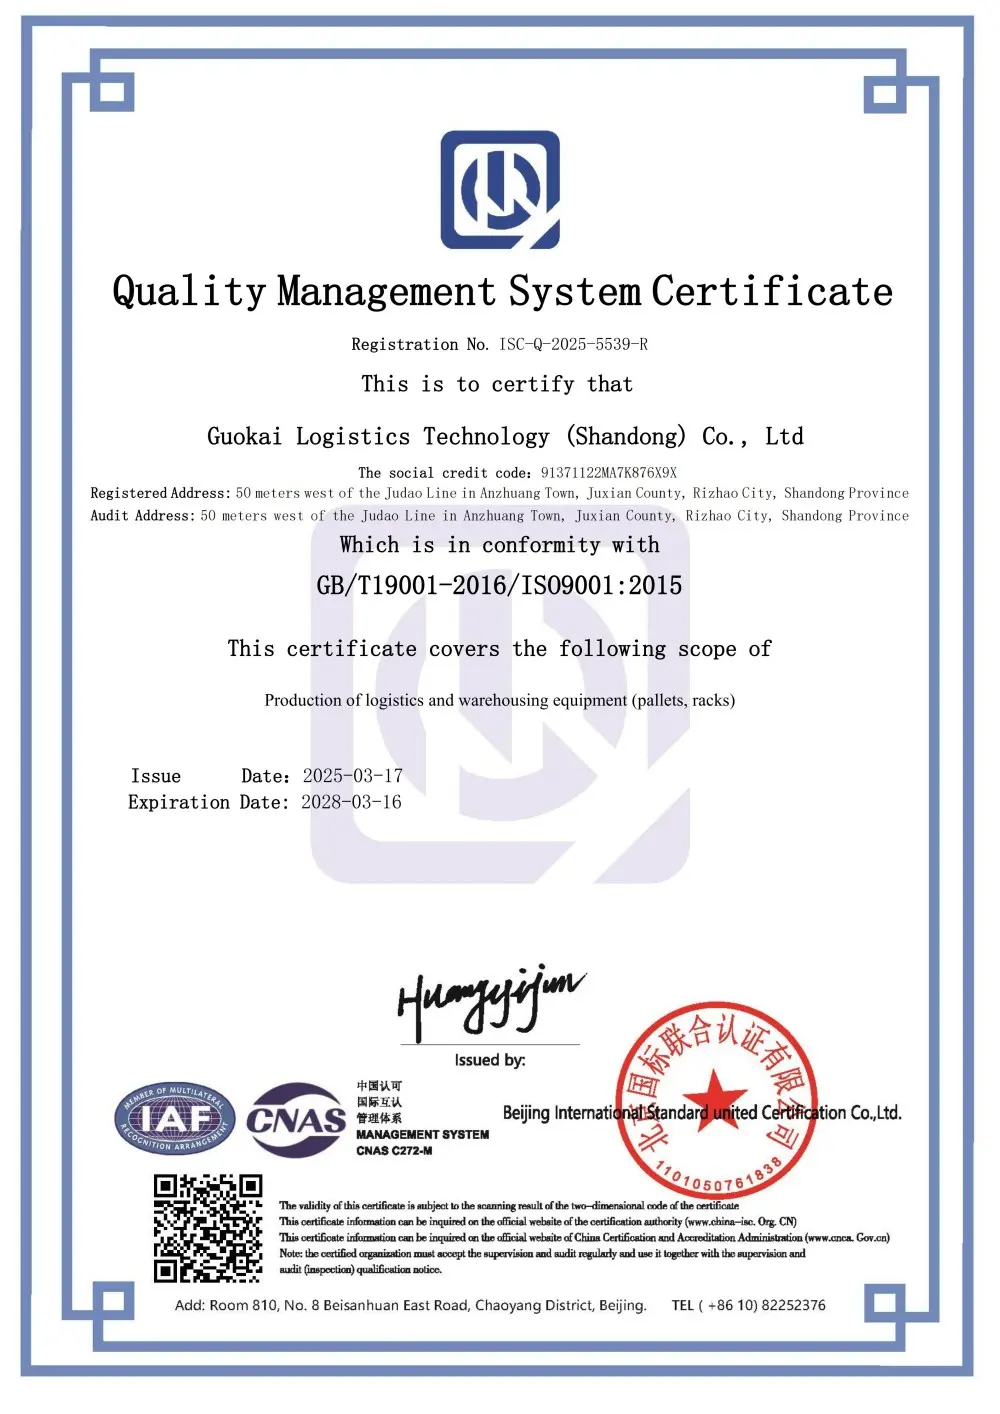
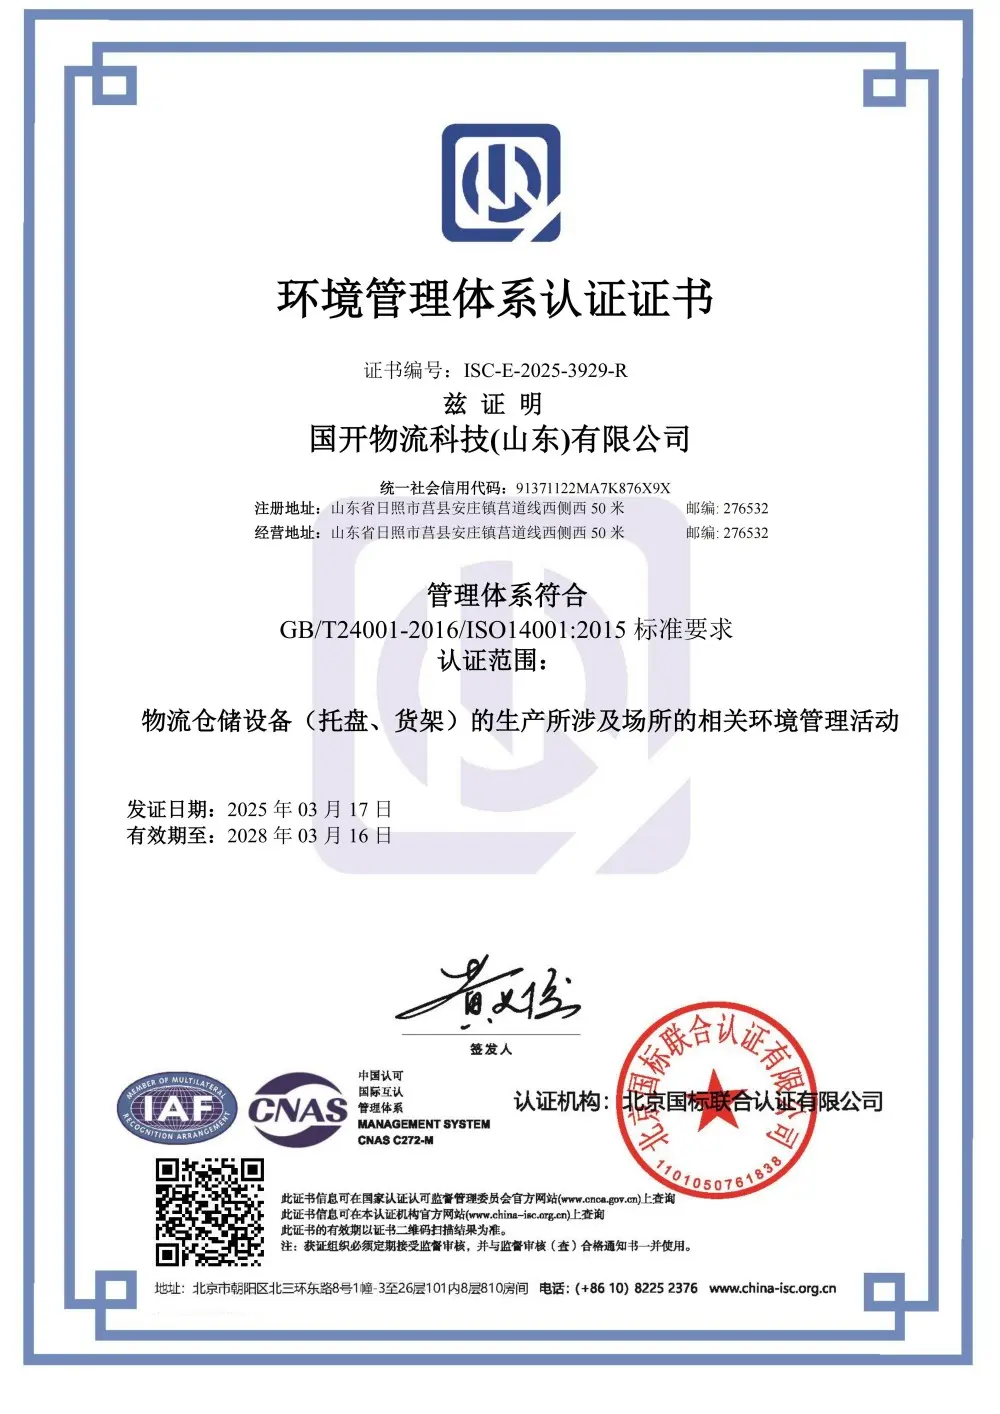
Browse our core product categories manufactured directly in our Shandong facility, ready for international project shipment.

Heavy-duty modular steel shelving units for organizing tools and industrial maintenance parts.
Versatile warehouse storage system configured for manual hand-loading and carton picking.

Unobstructed column arm storage system for pipes, tubing, aluminum extrusions, and timber.

Boltless rapid assembly metal shelf units offering adjustable shelf heights and clean aesthetics.
Motorized shuttle carriage systems driving automated pallet handling inside deep channels.

Integrated rack-supported mezzanines creating secondary working floors for order fulfillment.

Heavy-section structural steel floors providing wide open spans for industrial machinery.

Industry standard heavy-duty selective beam racking for high-capacity industrial warehouses.
Contact our Shandong engineering headquarters today to request CAD layout design proposals, FEA load calculations, and factory-direct pricing for your warehouse development.
