


Explore our precision-engineered warehousing storage solutions manufactured in Shandong, China. Built to international structural and safety codes.

Semi-automated radio shuttle pallet runner designed for high-volume, deep-lane storage with maximized footprint efficiency.
Explore Shuttle Racking
Heavy-duty structural steel platforms expanding vertical warehouse floor area for multi-tier industrial operations.
Explore Steel Platforms
Integrated multi-level mezzanine system combining structural racks with elevated walkways for manual item picking.
Explore Mezzanines
Continuous aisle high-density storage framework eliminating working aisles for large batch homogeneous palletized loads.
View Drive In Racking
Nested cart storage design accommodating 2 to 5 pallets deep per lane with Last-In, First-Out (LIFO) accessibility.
View Push Back Racking
Electronically driven mobile racking bases moving along floor rails to unlock 100% pallet selectivity in compact spaces.
View Mobile Racking
Automated battery-powered shuttle system designed for deep lane pallet handling with FIFO/LIFO flexibility.
View Radio Shuttle
Custom engineered storage solutions for non-standard, long-span structural profiles, pipes, and irregular industrial materials.
View Special RackingIn modern industrial logistics, static pallet racking and traditional fork-truck operations are increasingly hitting physical limits regarding volumetric storage efficiency and throughput limits. As global land costs rise and labor availability fluctuates, international enterprises are shifting toward high-density 3D Automated Storage and Retrieval Systems (AS/RS). At the absolute forefront of this technological transformation is the China 4-Way Shuttle System.
Unlike traditional 2-Way Radio Shuttles (which only travel linearly along a single deep storage channel) or rigid Stacker Crane AS/RS systems (which rely on massive, single-aisle crane towers constrained to single tracks), the 4-Way Pallet Shuttle is a fully autonomous robot capable of bi-directional movement. It travels cross-aisle (longitudinally) and along storage lanes (transversally) on custom cold-rolled guide rails. Coupled with high-speed vertical reciprocating conveyors (elevators) and intelligent Warehouse Control Systems (WCS), 4-Way Shuttles form a matrix-style 3D storage web. Shuttles can dynamically shift levels and channels, dynamically reallocating fleet density according to real-time throughput spikes.
While a 2-Way shuttle acts purely as an automated forklift extension within a single rack lane, a 4-Way Shuttle operates as an intelligent fleet unit inside a unified 3D matrix. If an elevator or shuttle requires maintenance, WCS software instantly reroutes adjacent 4-Way robots across the grid. This eliminates single-point-of-failure vulnerabilities inherent in Stacker Crane systems.
A granular breakdown of mechanical, electrical, and sensor systems powering Guake's high-efficiency 4-Way Pallet Shuttles.
Utilizing long-life Lithium Iron Phosphate (LiFePO4) battery packs combined with supercapacitor fast-charging technology. Shuttle units automatically navigate to in-rack charging stations during idle windows, completing a full operational charge in 30 minutes for 8+ hours of continuous duty.
Powered by high-torque brushless DC (BLDC) servo motors equipped with absolute optical encoders. The dual-wheel drive system executes smooth acceleration/deceleration curves, preventing cargo displacement even at maximum speeds.
Integrated 4-corner laser distance sensors, photoelectric obstacle detection switches, mechanical edge bumpers, and end-of-rail anti-drop sensors guarantee zero-collision safety within densely populated grid structures.
As a premier logistics technology manufacturer headquartered in Linyi, Shandong Province, Guake Logistics Technology (Shandong) Co., Ltd. leverages China's unmatched steel manufacturing ecosystem. By sourcing high-grade Q355B and Q235B cold-rolled structural steel directly from national mills, we ensure superior tensile strength, structural rigidity, and tight tolerances required for high-bay 4-Way Shuttle tracks.
Unlike regional assemblers who outsource critical hardware, Guake operates vertically integrated production lines encompassing full-automated roll-forming machinery, robotic laser cutting, precision CNC stamping, and automated electrostatic powder coating lines. This end-to-end control delivers compelling benefits to global buyers:
Evaluating the direct economic ROI of implementing 4-Way Shuttle Systems against conventional warehousing options.
| Storage Metrics / System Type | Selective Pallet Rack | 2-Way Radio Shuttle | Stacker Crane AS/RS | China 4-Way Shuttle System |
|---|---|---|---|---|
| Volumetric Space Density | Low (approx 40%) | High (approx 70%) | Very High (approx 80%) | Maximum (85%+) |
| SKU Versatility & Selectivity | 100% Access | LIFO / Channel FIFO | 100% Access | Dynamic 100% 3D Matrix |
| CAPEX Investment Level | Low | Medium | Extremely High | Balanced / High ROI |
| System Redundancy Risk | N/A (Manual) | Low | High (Crane Failure Stops Aisle) | Zero Single-Point Failure |
| Energy Consumption (Cold Store) | Baseline High | -20% Thermal Footprint | -30% Thermal Footprint | -40% Optimum Efficiency |
| Scalability (Fleet Expansion) | Manual Expansion | Add Shuttles Easily | Complex Structural Changes | Plug-and-Play Fleet Addition |
Payback Horizon Calculation: For a typical 10,000-pallet warehouse operational facility, transitioning from standard reach-truck racking to a Guake 4-Way Shuttle System typically yields a full capital return within 18 to 28 months. Savings stem primarily from the total elimination of 4 to 6 specialized fork trucks, substantial electricity reduction in climate-controlled spaces, and zero pallet damage caused by manual forklift operator errors inside aisles.
In sub-zero environments (-25°C to -30°C), cooling costs account for up to 60% of total warehouse operating expense. Guake 4-Way Shuttles utilize specialized low-temperature lubricants, cold-resistant electronic components, and internal heating elements for PCB control boards. By condensing cold storage footprints by 80%, operators dramatically reduce refrigeration volume loss.
Strict regulatory compliance demands strict First-Expired, First-Out (FEFO) batch tracking. Our WCS software integrates seamlessly with SAP, Oracle, and enterprise ERP systems, giving real-time tracking down to individual pallet serials while eliminating human picking error inside cleanroom facilities.
Fast-Moving Consumer Goods facilities experience massive seasonal throughput spikes. The 4-Way Shuttle system allows operators to scale picking speed dynamically: simply dispatching additional shuttle units into existing racking channels during peak promotional periods without expanding structural layout.
Heavy component storage requires exceptional frame load bearing capacity. Guake's heavy-duty 4-Way Shuttle systems safely handle heavy metal bins and structural component pallets weighing up to 1,500 kg per position with absolute structural stability.
Engineered to conform with European, American, and Asia-Pacific structural safety protocols.
Our structural racking design calculations adhere strictly to European FEM 10.2.02 and EN 15512 codes, ensuring safety factors under dynamic loading, sway stability, and seismic ground accelerations.
Guake 4-Way Shuttle robots bear full CE Certification (Machinery Directive 2006/42/EC and Electromagnetic Compatibility EMC Directive 2014/30/EU), guaranteeing safe electrical and mechanical operation worldwide.
Every shuttle fleet includes remote IoT telemetry modules. Guake engineers provide 24/7 remote diagnostics, firmware updates, and local partner engineer training for quick site support across North America, Europe, and Southeast Asia.
Technical, operational, and procurement queries answered by Guake's senior logistics automation engineers.
A 2-Way radio shuttle can only move forward and backward within a single dedicated racking lane; it requires a manual forklift driver to pick up the shuttle and physically transfer it to another channel. In contrast, a 4-Way Shuttle features integrated dual-wheel drive mechanisms that allow it to lift itself slightly and switch direction 90 degrees autonomously. It can travel longitudinally across distribution aisles and transversally into deep storage channels without any manual forklift intervention.
Level switching is accomplished by integrating vertical reciprocating conveyors (high-speed cargo elevators). When the WCS software instructs a shuttle unit to move from Level 2 to Level 5, the shuttle drives onto the elevator platform at its current level. The elevator elevates the shuttle robot to Level 5, where it rolls directly onto the target rail network to continue execution.
Because 4-Way Shuttles rely on precise optical sensors and laser positioning, structural racking installation tolerance must strictly comply with FEM 10.2.09 / EN 15512 standards. Concrete slab flatness should conform to Super Flat standards (typically FF 50 / FL 50 or VNA floor classifications) to ensure optimal rail alignment and smooth high-speed travel.
Traffic management is governed by our proprietary Warehouse Control System (WCS) middleware. The WCS maintains a real-time 3D spatial map of all shuttle locations. It dynamically locks grid nodes ahead of a shuttle's motion vector, preventing paths from overlapping. Furthermore, every shuttle hardware unit is equipped with redundant optical anti-collision sensors and emergency mechanical bump stops.
Yes. Guake manufactures specialized Cold-Chain Edition 4-Way Shuttles engineered specifically for deep-freeze environments down to -30°C (-22°F). These models feature sealed IP65-rated electronics boxes, internal condensation control heaters, specialized anti-freeze lubricants, and low-temperature LiFePO4 batteries designed to maintain high discharge efficiency.
Typical factory manufacturing lead time at our Shandong facility is 30 to 45 days following final CAD layout approval and structural calculation verification. On-site racking installation, rail alignment, and WCS software integration usually require an additional 3 to 6 weeks depending on total pallet capacity and system complexity.
To receive a complimentary CAD design layout and structural quotation, simply contact our engineering team via our website or email. Please provide your warehouse building drawing (CAD/PDF), clear height under beams, pallet dimensions (W x D x H including load), unit weight, required hourly pallet throughput, and temperature specs.
Browse our full range of manufactured storage racking systems and platform engineering products.
High-density radio shuttle racking engineered for max efficiency.
Select Product
Heavy structural steel floor platforms for industrial expandability.
Select Product
Multi-tier mezzanine shelving optimizing high-overhead warehouse spaces.
Select Product
Versatile modular shelving solutions for manual picking and archiving.
Select Product
Custom bolted structural platforms expanding operational footprint.
Select Product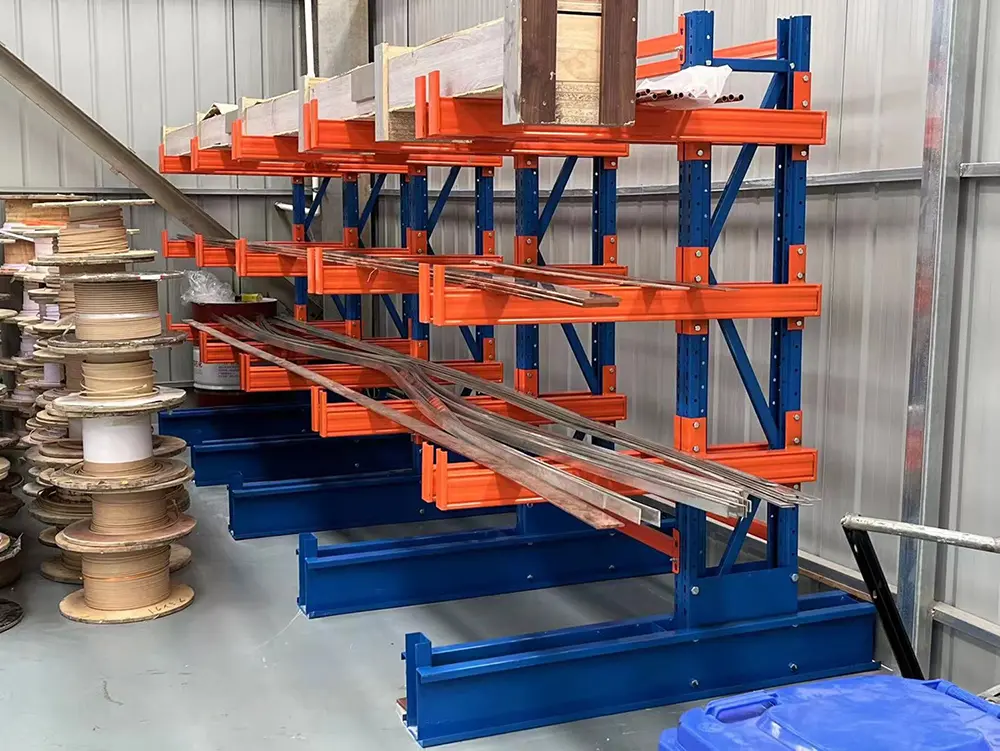
Gravity wheel and roller flow beds for continuous picking buffering.
Select Product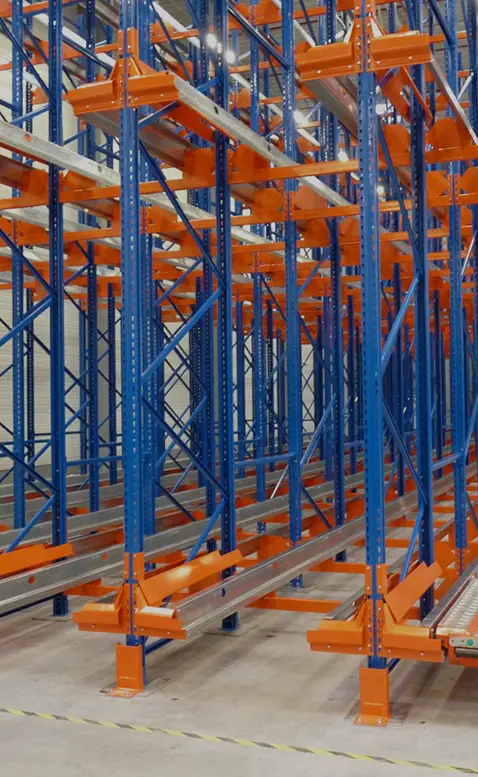
Tall structural pallet frameworks engineered for narrow-aisle trucks.
Select Product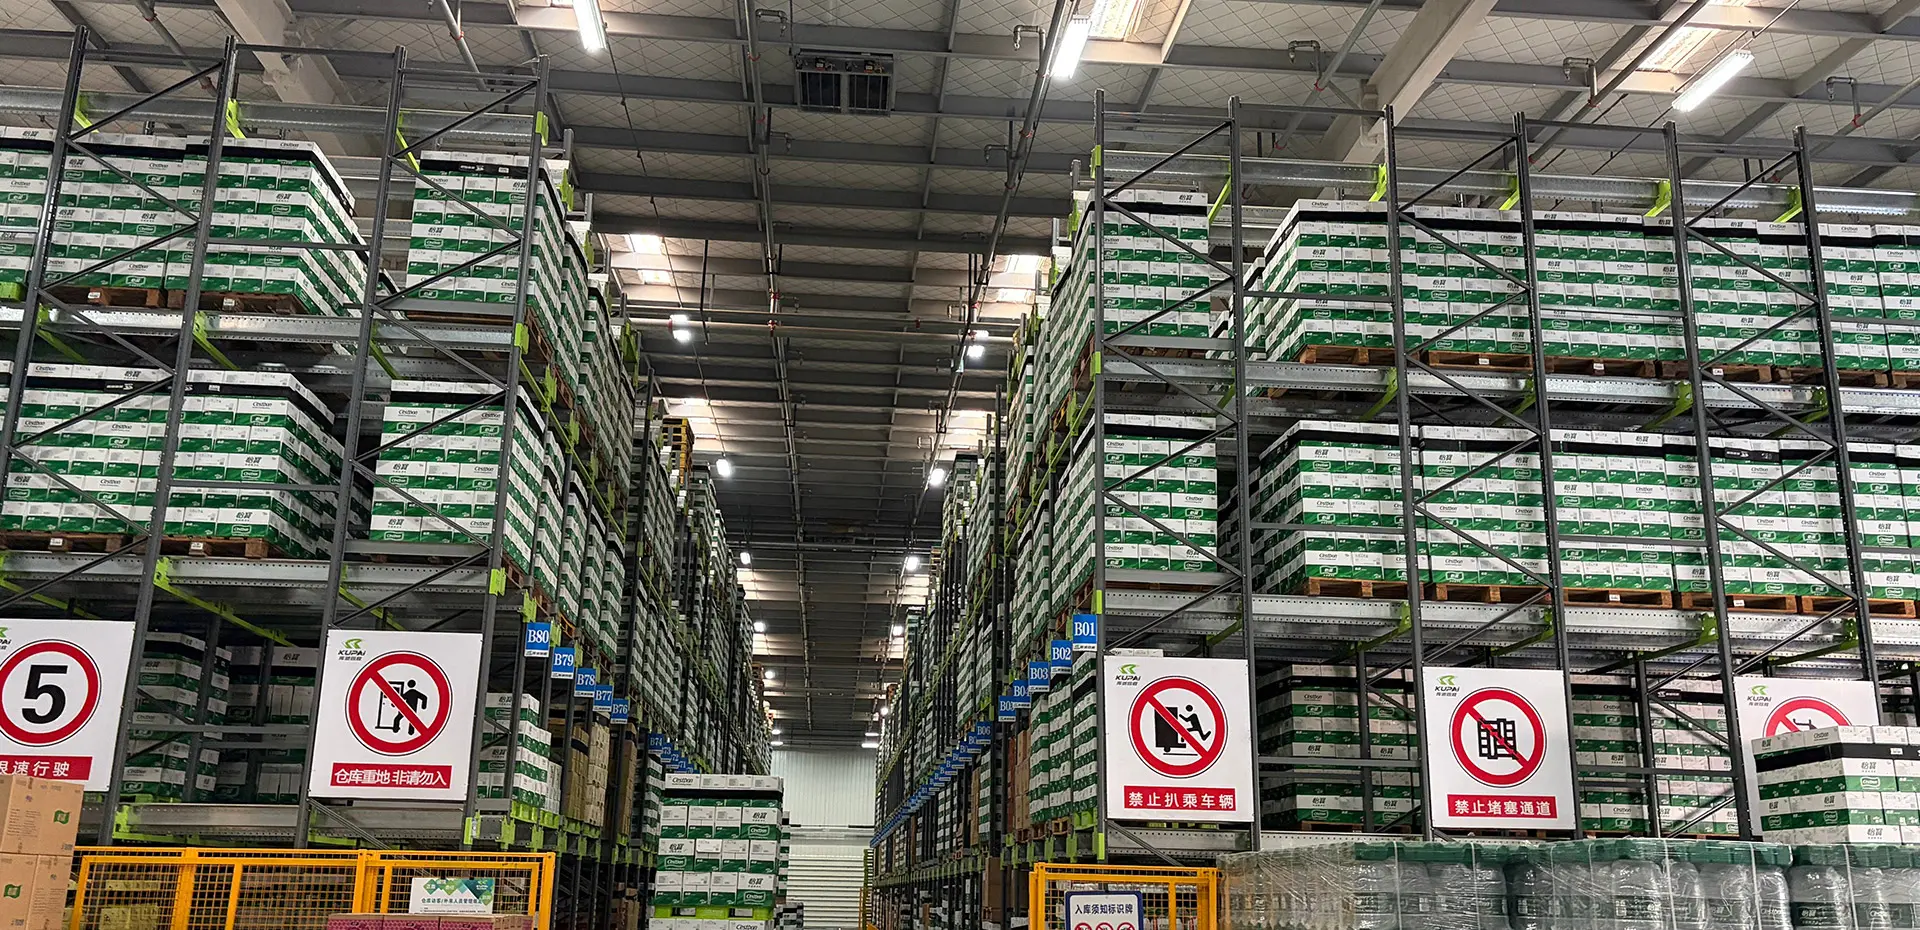
Fully integrated automated rack structures for high-bay stacker cranes.
Select ProductPartner with Guake Logistics Technology (Shandong) Co., Ltd. for factory-direct engineering expertise, competitive OEM pricing, and complete project support.
