


Explore our core engineered rack configurations manufactured with high-yield structural steel, tailored for heavy payload density and multi-tier spatial expansion.








Understanding how hybrid structural design eliminates front-column obstructions while doubling overhead cubic footprint under extreme point loads.
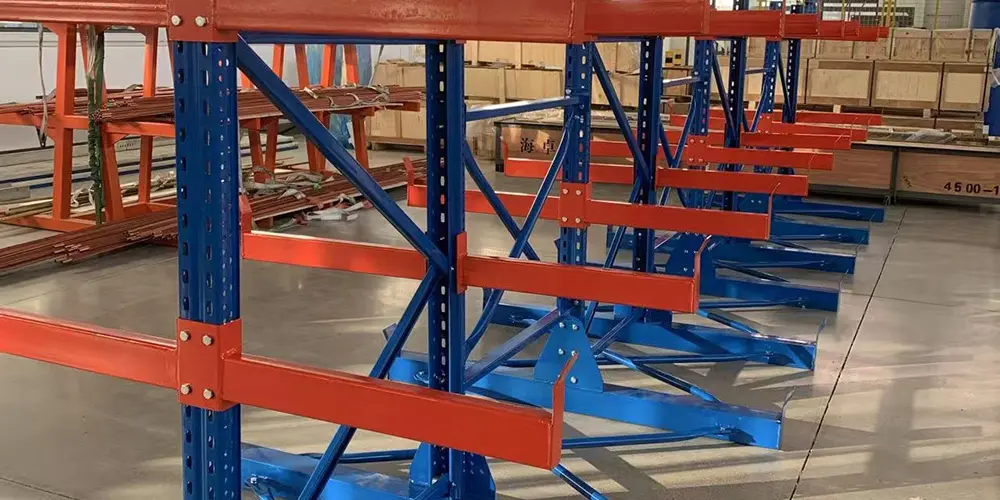
Traditional steel mezzanines rely on grid-spaced vertical columns (e.g., 4m x 6m grids) that severely restrict ground-floor vehicle movement and material handling agility. The Cantilever Mezzanine Floor System engineered by leading China suppliers fundamentally solves this constraint by fusing heavy-duty cantilever column posts with elevated structural deck joists. Utilizing cold-formed high-tensile steel or hot-rolled structural H-profiles (Q235B/Q355B grade), the vertical posts serve a dual purpose: supporting heavy-duty cantilever arms for storing long bar stock, tubing, and timber on lower tiers, while anchoring heavy primary steel beams that support an elevated mezzanine working level above.
By transferring overhead floor weight directly to rigid rear cantilever upright columns anchored with chemical expansion bolts into 300mm+ reinforced concrete foundations, ground-level operational aisles gain 100% unobstructed linear handling clearance.
To guarantee absolute structural safety, every cantilever mezzanine floor custom-designed by Guake Logistics Technology undergoes comprehensive 3D Finite Element Analysis (FEA) modeling. Under maximum uniform distributed loads (UDL) ranging from 300 kg/m² to over 1,500 kg/m², deflection limits are strictly governed by international FEM 10.2.02 and ANSI MH16.1 specifications.
Why sourcing directly from Shandong's premier racking cluster delivers unparalleled cost-efficiency, material integrity, and automated production throughput.
Located in Shandong Province—China's primary structural steel production heartland—Guake Logistics Technology leverages direct factory access to premier state steel mills (such as ShanSteel and Baosteel). We procure prime hot-rolled and cold-rolled Q235B and high-yield Q355B structural coil steel. Raw material mill test certificates (MTC) according to EN 10204 3.1 are strictly verified for chemical composition and yield strength before production begins.
Our 20,000+ m² facility houses fully automated multi-station cold-roll forming lines, 12-meter 6000W fiber laser cutting centers, and continuous CO2 gas-shielded robotic welding arms. Automated laser cutting guarantees bolt hole pitch positioning tolerances within ±0.2mm, eliminating site alignment friction during global structural installations.
Every steel structural member undergoes strict pre-treatment, including multi-stage chemical washing, rust degreasing, and shot blasting to Sa 2.5 cleanliness standards. Components are finished on an automated electrostatic powder coating line using epoxy-polyester thermoset resins (80 to 120 micrometers thickness), passing 500-hour salt spray corrosion testing.
Tailored structural cantilever mezzanine architectures customized to eliminate spatial bottlenecks across heavy engineering, logistics, and automotive sectors.
Houses heavy raw materials (steel plates, round bars, I-beams) on lower heavy-duty cantilever arms with up to 3,000 kg per arm load rating, while utilizing the overhead structural platform for CNC machining stations, tooling storage, or production offices.
Automotive logistics hubs face mixed inventory types: long exhaust pipes, body panels, and heavy engine blocks. Our hybrid layout pairs cantilever racking for irregular components with upper mezzanine picking levels fitted with bin shelving.
Ideal for storing 6-meter aluminum profiles, PVC piping, drywall bundles, and solar panel racking. Unobstructed continuous cantilever runs prevent material bending while mezzanine decks house hardware items and administrative suites.
Maximizes warehouse vertical clear height (8m to 14m) by establishing 2-tier or 3-tier steel mezzanine platforms. Integrates vertical reciprocating conveyors (VRCs), spiral chutes, and carton flow racks for fast split-case order picking.
Engineered for extreme structural precision. Supports long aircraft structural spars and composite tubes on non-marking rubber-lined cantilever arms, while the mezzanine floor provides cleanroom assembly enclosures.
Sub-zero warehouse volume is vastly expensive to cool. Hot-dip galvanized structural cantilever mezzanine platforms withstand low-temperature embrittlement down to -30°C, increasing cubic freezer space utilization by over 85%.
Engineered to conform with European, American, and Australian building codes for seamless regulatory sign-off and site safety worldwide.
Procuring structural steel from China requires total adherence to local destination structural safety standards. Guake Logistics Technology provides full engineering calculation packages stamped by certified structural engineers compliant with:
For installations situated in high seismic zones (such as Seismic Design Categories D, E, and F under IBC), cantilever mezzanine structures are engineered with specialized dynamic moment-frame connections, heavy-duty floor baseplate anchors, and vertical/horizontal X-bracing assemblies.
Structural columns utilize oversized welded baseplates anchored with M16-M24 chemical anchors into concrete subfloors, resisting lateral ground acceleration forces without structural sway or joint shear failure.
| Structural Parameter | Light to Medium Duty Standard | Heavy-Duty Industrial Standard | Extra Heavy Structural Steel (H-Beam) |
|---|---|---|---|
| Mezzanine Floor Load (UDL) | 300 kg / m² – 500 kg / m² | 500 kg / m² – 1,000 kg / m² | 1,000 kg / m² – 2,500+ kg / m² |
| Cantilever Arm Load Rating | 150 kg – 400 kg per arm | 400 kg – 1,200 kg per arm | 1,200 kg – 3,500 kg per arm |
| Steel Grade Material | Q235B Cold-Formed Steel | Q235B / Q355B Cold-Formed Structural | Q355B Hot-Rolled H-Beam Structural Steel |
| Decking Type Options | Steel Panels / Plywood / MDF | Perforated Steel / Checkered Plate | Heavy Bar Grating / Reinforced Steel Deck |
| Max Column Height | 3,000 mm – 5,000 mm | 5,000 mm – 9,000 mm | Up to 15,000 mm (Multi-Tier) |
| Surface Protection | Epoxy Powder Coating (80µm) | Thermoset Powder Coating (100µm) | Hot-Dip Galvanized (ISO 1461, 65µm+ zinc) |
How emerging robotics, IoT structural sensors, and high-strength alloys are transforming static mezzanine platforms into intelligent warehousing hubs.
Future mezzanine floors are increasingly required to support Autonomous Mobile Robots (AMRs) operating on upper decking levels. Guake's R&D roadmap includes specialized ultra-flat steel decking systems with dynamic point-load deflection reinforcement, sound-dampening sub-layers, and high-friction anti-slip coatings optimized for robot navigation wheel traction.
Integrating wireless strain gauges and piezoelectric vibration sensors into critical cantilever arm joints and main structural mezzanine beams. These IoT sensors continuously stream live stress, deflection, and impact data to cloud dashboards, alerting warehouse managers before micro-cracks or overload fatigue exceed safety thresholds.
Moving away from permanently welded site structures toward 100% boltless, clip-in modular cantilever arm brackets and standardized interlocking deck joists. This allows enterprise operators to dismantle, expand, or reconfigure mezzanine platform footprints with zero waste when operational logistics demand shift.
How direct factory sourcing from China reduces capital expenditure (CapEx) while safeguarding long-term asset value and installation timelines.
Procuring industrial storage infrastructure through regional distributors often incurs overhead markups of 35% to 60%. By partnering directly with Guake Logistics Technology (Shandong) Co., Ltd., enterprise buyers gain direct engineering collaboration, transparent steel price indexing, and complete oversight over factory fabrication.
Structural steel components are flat-packed using custom steel-banded pallets and wood-free protective cradles. Structural members are nested to achieve maximum volumetric density per 40ft High Cube (40HC) container (up to 26 metric tons), minimizing shipping freight cost per square meter of floor space.
To ensure zero field installation defects, our factory enforces rigorous acceptance testing before export clearance:
Expert technical answers regarding structural calculations, local building codes, installation mechanics, and custom manufacturing options.
A standard racking mezzanine utilizes traditional pallet rack uprights with front columns located at regular intervals (typically 1.5m to 2.7m), creating obstructions on the ground level. A cantilever mezzanine floor uses heavy-duty cantilever column posts situated at the rear or center, featuring overhanging arms and cantilevered primary steel beams. This design eliminates front vertical columns entirely along ground aisles, allowing continuous horizontal storage for long materials (pipes, timber, steel bars) while providing a solid, uninterrupted elevated floor platform above.
To prepare an accurate FEA-backed structural proposal, our engineering team requires:
We design mezzanine floor decks to accommodate local municipal fire codes. For facilities requiring in-rack and under-mezzanine sprinkler coverage, we offer open steel mesh grating (up to 70% water permeability) or pre-punched perforated steel floor panels. Furthermore, staircases are engineered with compliant riser heights, handrails (1100mm height with toe-plates), and self-closing safety drop gates in accordance with OSHA, EN ISO 14122, and AS1657 standards.
The optimal decking depends on your application: Steel Checkered Plates provide high durability, non-slip surfaces, and complete solid dust/liquid isolation between levels. Open Steel Bar Grating maximizes light passage and sprinkler penetration, essential for high-bay facilities. High-Density Structural Plywood/MDF on Steel Sub-decking offers a cost-effective, noise-dampening surface smooth for hand trolley rolling in e-commerce picking areas.
Every exported system includes comprehensive installation documentation: a fully labeled 3D assembly schematic, piece-marked component packing lists, and step-by-step video installation guides. For major enterprise projects, Guake can dispatch experienced installation engineers to superintend local erection crews, perform quality sign-offs, and conduct final load-testing verification on site.
For standard dry indoor warehouses, our electrostatic thermoset epoxy powder coating (80-120µm) provides durable scratch and rust protection in custom RAL colors. For high-humidity, outdoor, chemical, or sub-zero cold-storage (-30°C) installations, we supply Hot-Dip Galvanizing (HDG) according to ISO 1461, immersing steel components in 450°C molten zinc to achieve a 65µm to 85µm zinc protective layer guaranteed against corrosion for 25+ years.
Initial CAD layout proposals and structural FEA reports are delivered within 48 hours. Once approval drawings are signed and raw material steel testing is verified, manufacturing takes 20 to 30 calendar days depending on project tonnage. Ocean shipping transit from Qingdao/Linyi ports takes approximately 14-35 days depending on the destination port (Southeast Asia, Europe, Middle East, or the Americas).
Yes. All Guake mezzanine systems feature 100% bolted structural connections (Grade 8.8 or 10.9 high-tensile fasteners) with zero field welding required during assembly. This modular architecture allows the entire floor structure to be unbolted, packaged, relocated, and re-erected in a new warehouse facility or expanded by adding matching modular joists and columns.
Select from our specialized long-goods cantilever racks, heavy-duty selective storage, boltless shelving, and integrated platform systems.







Connect directly with Guake's structural engineering team in Shandong. Receive FEA structural calculations, 3D CAD layouts, and direct factory pricing within 48 hours.
