


Factory-direct engineered warehouse systems manufactured in Shandong, China. Built to ISO & FEM standards for global industrial applications.

Multi-tier structural floor platforms designed to double vertical warehouse capacity without structural facility modifications.
View Mezzanine Systems
Heavy-duty bolted structural steel platforms supporting extreme floor loads from 300kg/m² up to 1,000kg/m².
Explore Steel Platforms
Semi-automated deep-lane pallet storage powered by remote-controlled shuttles. Maximizes cold storage volume efficiency.
Discover Shuttle Systems
Continuous lane pallet storage eliminating operating aisles. Ideal for large batches of homogeneous SKUs.
View Drive-In Racks
Nested cart dynamic storage supporting 2 to 5 pallets deep per lane. Combines dense storage with single-aisle access.
View Push Back Systems
Electric motorized mobile bases running on floor rails, opening operational aisles on demand to double storage footprint.
Explore Mobile Racking
Column-free front access engineered specifically for steel pipes, timber, aluminum extrusions, and heavy sheet materials.
View Cantilever Systems
Battery-powered lithium shuttle cars integrated with warehouse management software for high-throughput logistics.
Explore Shuttle AutomationIn modern industrial logistics, traditional selective pallet racks present fundamental structural limitations when handling non-palletized, linear, or irregularly shaped cargo. Standard selective pallet frames utilize vertical front columns connected by horizontal beams, creating a enclosed rectangular box bay. When attempting to store 6-meter steel pipes, 12-meter aluminum extrusions, raw timber bundles, or heavy sheet metal, front structural uprights create physical obstructions that render conventional racking unusable.
This operational challenge led to the development of Cantilever Rack Shelving. Architecturally, cantilever systems eliminate front vertical columns entirely. The design relies on central heavy-duty vertical column towers, robust base assemblies anchored directly into concrete foundations, and horizontal arms cantilevered outward to support distributed structural loads. This uninhibited, continuous storage bay allows fork trucks and side-loaders to deposit long goods of any length across multiple arm levels without horizontal obstruction.
Hot-rolled structural I-beams and H-sections (Q355B steel) built for extreme point loads, seismic resistance, and heavy industrial abuse in steel mills.
High-tensile cold-rolled steel profiles engineered for light to medium duty storage, providing cost efficiency for plumbing, PVC, and molding inventory.
Arm design engineered around maximum permissible deflection ratios ($L/300$), preventing load sag and ensuring safe forklift clearance during retrieval.
The structural engineering of cantilever rack shelving centers on managing bending moments ($M$) concentrated at the junction between the cantilever arm and the vertical column. Unlike standard pallet racks where weight is divided evenly across four vertical posts, a cantilever arm acts as a classic overhanging beam subjected to uniformly distributed load ($w$) or concentrated load ($P$).
The maximum bending moment generated at the arm connection is calculated using the load center distance ($L_c$):
Bending Moment Formula: $M = W \times L_c$
Where $W$ represents total payload weight per arm level, and $L_c$ is the distance from the vertical column face to the center of load gravity. China OEM factories utilize heavy 4-bolt or hairpin connection plates welded to tapered arm profiles to dissipate these high moment stresses into the upright tower structure efficiently.
Furthermore, structural stability requires rigid horizontal and vertical X-bracing sets connected between upright towers. These cross-bracing bays transfer lateral shear forces caused by forklift impacts or seismic ground movement, maintaining total structural integrity across long storage runs.
When international procurement directors, supply chain VPs, and EPC contractors evaluate a China Cantilever Rack Shelving Manufacturer, purchasing decisions extend far beyond initial per-ton steel pricing. Enterprise buyers require robust proof of structural compliance, metallurgical verification, and total cost of ownership (TCO) optimization.
Racking systems must comply strictly with international structural design codes: RMI (Rack Manufacturers Institute) in North America, FEM 10.2.09 in Europe, and AS4084-2012 in Australia to ensure site sign-off.
Direct sourcing from tier-1 steel mills (such as Baosteel, Shougang) guaranteeing certified yield strength ($f_y \ge 355 \text{ MPa}$ for Q355B structural steel) with mill test certificates (MTC) supplied per batch.
Outdoor timber yards and heavy chemical storage demand Hot-Dip Galvanizing (HDG) to EN ISO 1461 standards (minimum 65–85 μm coating thickness) for 30+ year rust resistance.
How Shandong’s advanced industrial cluster combines robotic manufacturing, raw material scale, and deep-sea port logistics to deliver global cost dominance.
Located in Shandong Province—China’s heavy engineering steel heartland—Guake Logistics Technology leverages fully integrated Industry 4.0 manufacturing lines. CNC automatic punching units pierce upright column profiles at precise 75mm or 100mm pitch increments with zero cumulative tolerance error.
Multi-axis Fanuc and KUKA robotic welding stations perform continuous, deep-penetration metal active gas (MAG) welds on heavy column-to-base joint plates. This automated execution eliminates human welding defects, ensuring uniform stress distribution and certified load capacities across every single manufactured batch.
Before surface coating, raw structural steel members undergo a 12-stage automated pre-treatment sequence including heavy shot-blasting (Sa 2.5 standard), degreasing, zinc phosphating, and deionized water rinsing. This guarantees ultra-strong paint adhesion for epoxy electrostatic powder coatings.
Furthermore, export logistics utilize flat-pack modular packing engineering. Upright towers, arms, and bracing sets are bundled using high-tensile steel strapping with protective corner guards, optimizing 40ft High Cube container volumetric utilization and reducing sea freight costs per ton significantly.
Industrial real estate markets in North America, Europe, and East Asia have experienced dramatic per-square-meter cost escalation over the past decade. Facility managers can no longer afford wide, single-level floor storage for long items like timber stock, aluminum profiles, or heavy steel pipes. Storing materials on floor dunnage consumes valuable operational square footage while creating severe safety hazards and slow inventory retrieval speeds.
By transitioning to high-bay Cantilever Rack Shelving systems reaching heights up to 10 to 12 meters, facilities transition their operational footprint from two-dimensional square-meter planning ($m^2$) to three-dimensional cubic volume maximization ($m^3$).
Cubic Storage ROI Case Study: Replacing floor-bound bundle storage with a 6-tier structural cantilever racking system increases vertical capacity by 450% within the exact same building footprint. Paired with narrow-aisle side-loading forklifts or multi-directional reach trucks, operational aisle widths are compressed from 5.5 meters down to just 2.2 meters.
Versatile engineering designs customized to meet the distinct operational demands of heavy industry worldwide.
Heavy-duty structural H-beam cantilever racks designed to support 3,000kg to 5,000kg per arm level. Configured with removable vertical pipe stops to prevent heavy round steel bars and seamless oil pipes from rolling off during forklift maneuverings.
Outdoor galvanized cantilever installations featuring roof trusses integrated directly onto upright tower tops. Provides rain and UV protection for premium engineered timber, plywood sheets, and architectural wooden beams.
Medium-duty cantilever arms fitted with protective plastic liners, rubber sleeves, or brass end caps. Prevents scratching and surface marring on sensitive anodized aluminum extrusions and decorative architectural trims.
Custom double-sided cantilever systems integrated directly alongside vehicle assembly lines, holding frame rails, driveshafts, exhaust pipes, and heavy stamping dies for quick overhead crane picking.
Continuous mesh-decked or steel-plate cantilever racking allowing simultaneous storage of long pipe bundles alongside palletized drywall compound, doors, and sheet insulation on the same arm levels.
Specialized heavy cantilever columns fitted with axle spools to hold massive electrical cable reels and solar panel mounting rails, enabling direct payout of wiring directly from stored spools.
Selecting the optimal cantilever specification requires balancing payload weight, operational height, environmental exposure, and financial budget. The comparative matrix below outlines structural thresholds calculated by China manufacturing engineers:
| Engineering Parameter | Cold-Rolled Cantilever System | Heavy-Duty Structural Steel (H-Beam) |
|---|---|---|
| Raw Material Steel Grade | Q235B Cold-Rolled Coils | Q355B Hot-Rolled Structural H-Beams / I-Beams |
| Load Capacity Per Arm | 100 kg – 600 kg per arm | 800 kg – 4,500 kg per arm |
| Maximum Tower Height | Up to 4.5 Meters | Up to 12.0 Meters (Custom engineered) |
| Forklift Impact Resistance | Moderate (Requires floor guide rails) | Extreme (Heavy structural steel gauge resilience) |
| Arm Connection Type | Hook-in / Keyhole slot with safety pins | Heavy 4-Bolt Flange Connection / Hairpin Pivot |
| Environmental Resistance | Powder Coated (Indoor dry storage) | Hot-Dip Galvanized (Outdoor / Corrosive environments) |
| Primary Target Application | Light PVC, copper tubing, molding, furniture | Steel pipes, heavy rebar, structural lumber, coils |
Modern distribution hubs rarely rely on a single racking format. High-efficiency logistics plants integrate cantilever systems alongside other specialized warehouse storage architectures to manage diverse stock keeping units (SKUs).
As a leading total-solution manufacturer, Guake Logistics Technology engineers multi-zone facility blueprints combining:
Detailed answers regarding engineering, customization, shipping logistics, and structural safety from our senior engineering team.
Factory-direct engineered warehouse systems for every industrial application.

Cost-effective column-free storage designed for plastic pipes, wood trim, and medium weight tubing.
View Details
Heavy structural platforms creating usable overhead floor space for picking, assembly, or offices.
Explore Platforms
Standard selective beam pallet racks giving 100% direct access to every stored pallet position.
View Pallet Racks
Versatile manual boltless shelving for small parts, e-commerce fulfillment centers, and archive boxes.
Explore Shelving
Rapid assembly clip-in steel shelving designed for retail stockrooms and light industrial inventory.
View Boltless Racks
Heavy-gauge modular storage racks engineered for commercial workshops, tools, and industrial garages.
View Garage Units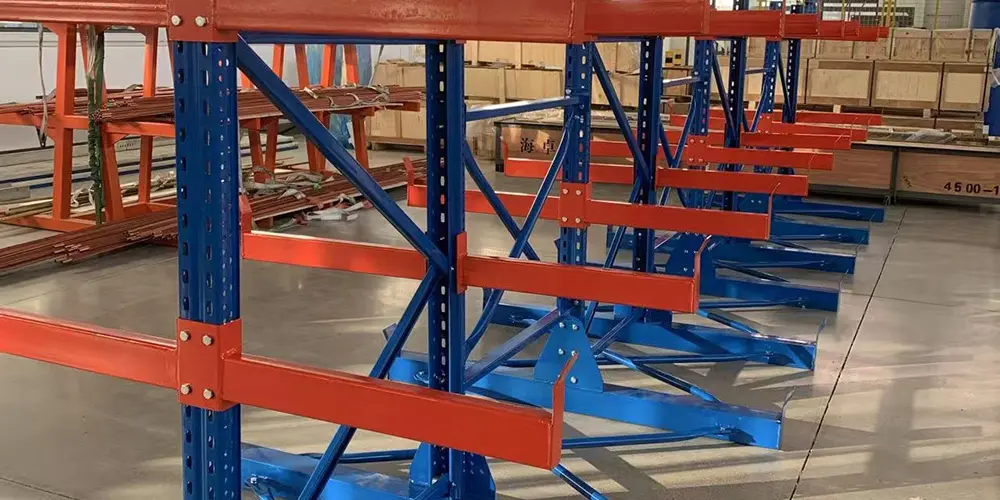
High-capacity structural H-beam cantilever racking designed for oil & gas pipe yards and heavy steel tubing.
View Pipe Racks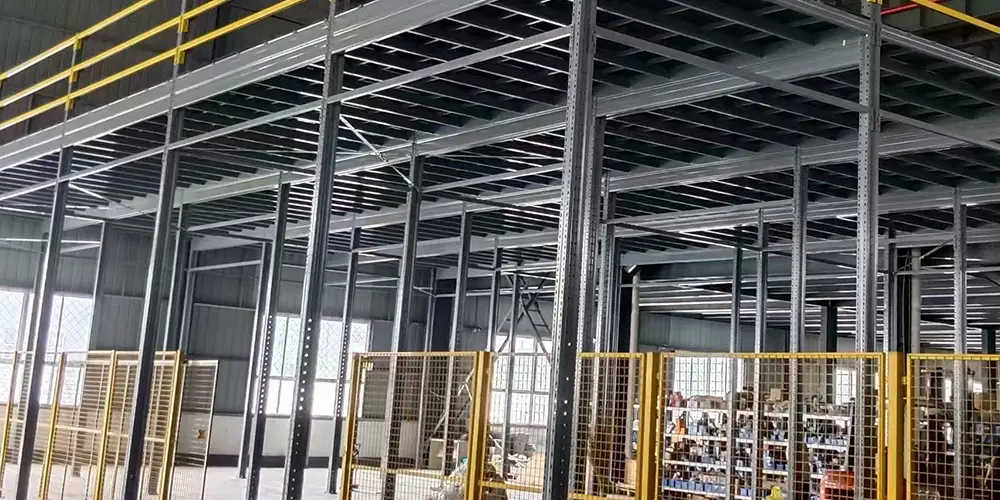
Integrated multi-level floor systems maximizing high-bay ceiling heights for dense order picking.
Explore MezzaninesShare your warehouse layout drawings, material load profiles, or storage targets with our Shandong engineering team for a full structural proposal within 24 hours.
