


Engineered in Shandong, China. Fully customizable heavy-duty structural steel solutions manufactured to international safety and load-bearing standards.

Motorized mobile bases mounted on embedded floor rails. Eliminates fixed aisles to expand storage capacity by up to 100%.
Explore Mobile Racking
Semi-automated deep-lane storage system utilizing wireless pallet shuttles. Supports both FIFO and LIFO operational flows.
View Shuttle Systems
Multi-tier heavy-duty structural steel platforms converting vertical airspace into usable picking, office, or storage floors.
View Mezzanine Racks
High-density cold-storage ready pallet shuttle configurations engineered for high throughput and minimized forklift entry risk.
View Shuttle Racks
Heavy structural I-beam steel platforms supporting dynamic floor loads up to 1,000 kg/m² for industrial warehousing.
View Steel Platforms
Maximizes cubic storage volume by permitting forklifts to drive directly into storage lanes. Ideal for bulk homogeneous SKUs.
View Drive-In Racks
Nested cart storage matrix allowing 2 to 5 pallets deep per lane with automatic gravity-fed pallet indexing upon retrieval.
View Push Back Racks
Heavy-duty cantilever arms engineered for oversized, long, or irregular profiles including pipes, lumber, and steel coils.
View Special PurposeAs global industrial land prices escalate and warehouse operational expenditures mount, logistics operators, 3PL providers, and cold-chain enterprises are moving away from traditional static racking. Mobile Rack Storage Systems represent the benchmark engineering solution for space optimization.
By placing heavy-duty pallet racking onto electric motorized mobile carriages running on precision floor tracks, static gangway aisles are consolidated into a single movable working aisle. This transforms standard 45% floor utilization into an astonishing 85% to 90% net cubic utilization.
Refrigerated and sub-zero cold storage warehouses (-25°C) face exorbitant power costs per cubic meter. China mobile rack storage systems double the pallet capacity within identical refrigerated envelopes, slashing cooling overhead per pallet by up to 40%.
Unlike block stacking or drive-in racking which sacrifice selectivity for density, electric mobile racking allows instant radio-remote or WMS-triggered aisle opening, offering immediate direct access to every single pallet position without double handling.
China mobile rack storage manufacturing combines heavy industrial cold-rolled steel fabrication with precision electrical engineering and IoT safety controls.
The core structural element of mobile rack storage is the heavy-duty welded steel base carriage. Equipped with dual-flanged forged steel wheels running on cold-drawn guide rails embedded flush into the concrete slab, each mobile base unit supports payloads exceeding 24,000 kg (24 tons) per bay assembly.
Safety compliance is paramount when moving multi-ton structural arrays. Modern mobile racking systems manufactured in China incorporate quadruple safety redundancies complying with European EN 15095 and ISO standards:
Compare high-density warehousing systems to evaluate structural density, selectivity percentage, initial CapEx ROI, and operational suitability.
| Storage System Type | Cubic Density | SKU Selectivity | Access Flow | Cold Storage Efficiency | Relative CapEx Index |
|---|---|---|---|---|---|
| Mobile Racking System | Ultra-High (85-90%) | 100% Direct Access | FIFO / LIFO | Optimal (-25°C Ready) | Medium - High |
| Radio Shuttle Racking | Ultra-High (80-85%) | Lane Dependent | FIFO / LIFO | Excellent | Medium - High |
| Drive In Racking | High (65-75%) | Low (Per Lane) | LIFO Only | Good | Low (Cost Effective) |
| Push Back Racking | Moderate (60-70%) | Lane Face (2-5 Deep) | LIFO Only | Moderate | Medium |
| Mezzanine & Steel Platform | Adds Vertical Floor Area | 100% Manual / Tote | Flexible | N/A (Ambient/Chilled) | Medium |
| Selective Pallet Racks | Standard (40-50%) | 100% Direct Access | FIFO / LIFO | Low (High Footprint) | Lowest |
Mobile rack storage systems deployed by China manufacturers are customized to meet unique localized environment factors and regulatory demands across key industrial sectors.
Operating in environments down to -30°C requires special cold-grade steel (Q355D/E), low-temperature synthetic lubricants, and IP65-rated moisture-sealed electronics. China suppliers design heating cables inside floor tracks to eliminate ice build-up and structural jams.
Pharmaceutical distribution nodes require non-contaminating, dust-free storage solutions. Electric mobile bases utilize sealed gearboxes and epoxy powder-coated surfaces that withstand strict washdown protocols and anti-microbial sanitation requirements.
For heavy stamping dies, engine blocks, and spare parts hubs, mobile cantilever and heavy beam mobile racks provide dense, accessible storage with point load capacities exceeding 4,000 kg per shelf beam level.
The convergence of Robotics, Artificial Intelligence, and Structural Steel Engineering is giving rise to fully autonomous mobile storage ecosystems.
Future mobile racking integration bypasses human forklift drivers entirely. Autonomous Guided Vehicles (AGVs) communicate via 5G/Wi-Fi 6 WMS gateways, triggering mobile aisles to open dynamically as the AGV approaches the aisle entry point.
Machine learning algorithms analyze order picking history during peak and off-peak shifts, positioning mobile bases ahead of time to open aisles with high-frequency SKUs, eliminating driver waiting latency by up to 60%.
Embedded strain gauges and vibration telemetry units stream continuous mechanical integrity data to cloud dashboards, alerting maintenance personnel to floor settlement or frame deflection before structural fatigue occurs.
Guake Logistics Technology (Shandong) Co., Ltd. brings over 15 years of precision manufacturing experience to the global material handling market, operating out of Linyi, Shandong—China's primary structural steel production hub.
Our 20,000+ m² manufacturing facility utilizes certified high-tensile cold-rolled steel coils (Q235B & Q355B). Automated continuous roll-forming lines, robotic laser cutters, and 60-meter automatic electrostatic powder coating lines guarantee tight dimensional tolerances (+/-0.5mm) and robust corrosion resistance.
From initial CAD layout planning and structural FEA stress calculations to export packaging, customs compliance, international shipping, and remote/onsite installation supervision—Guake serves as your single accountable engineering partner.
Mobile rack storage systems engineered in China strictly comply with international structural safety codes, guaranteeing safe operational load factors across global logistics markets.
Design standards for steel static pallet racking, governing beam deflection, column slenderness, and joint stiffness under heavy payloads.
European standard regulating safety requirements for power-operated mobile racking, shelving, and shuttle storage equipment.
Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks used extensively across North American markets.
Custom structural base tie-downs and heavy expansion anchors engineered to absorb lateral ground acceleration forces in active seismic zones.
Essential technical and procurement insights answered directly by our senior structural engineering team.
Guake Logistics Technology manufactures a comprehensive portfolio of high-density and conventional warehouse racking systems:
Both systems provide exceptional storage density (80-90% floor space utilization), but they serve different inventory profiles:
Mobile Racking mounts standard selective racks on motorized bases. It opens one aisle at a time, providing 100% direct access to every SKU, making it superior for high SKU diversity with medium throughput.
Radio Shuttle Racking uses automated shuttles inside deep lanes. It offers higher throughput for a few SKUs stored in large batch quantities, but direct access to individual interior pallets is limited.
Because mobile rack bases concentrate heavy multi-ton loads onto steel floor rails, the concrete floor must meet strict structural criteria:
Yes. Our engineering department provides complete layout proposals along with structural engineering calculations free of charge. Simply submit your warehouse details including:
Our mobile racking systems feature multiple power contingency safeguards:
Yes. Every overseas project includes comprehensive structural drawings, 3D installation guides, component packing lists, and electrical schematics. We offer flexible support options including dispatching senior installation engineers to your international job site for on-site commissioning, as well as live remote technical guidance via video link.
Absolutely. All structural parameters are engineered to order. We offer custom upright heights up to 15 meters, tailored beam lengths, adjustable level pitches, and powder coating in any standard RAL color code to match your corporate branding.
Select a specialized storage structure engineered to maximize your specific warehouse operational workflow.

Boltless modular steel shelving units for hand-loaded inventory, spare parts, and archival storage applications.
View Shelving Systems
Adjustable column and arm system designed for continuous lateral storage of lightweight pipes and profiles.
View Cantilever Systems
Rapid assembly interlocking steel shelf units providing flexible tier heights without mechanical fasteners.
View Boltless Shelving
Free-standing structural steel platforms engineered to support heavy machinery, sorting lines, or elevated offices.
View Platform Systems
High-density manual carton picking racks integrated with catwalk stairways for e-commerce fulfillment hubs.
View Multi-Layer Shelving
Standard high-bay selective pallet storage frames engineered for heavy industrial unit load storage.
View Heavy Pallet Racks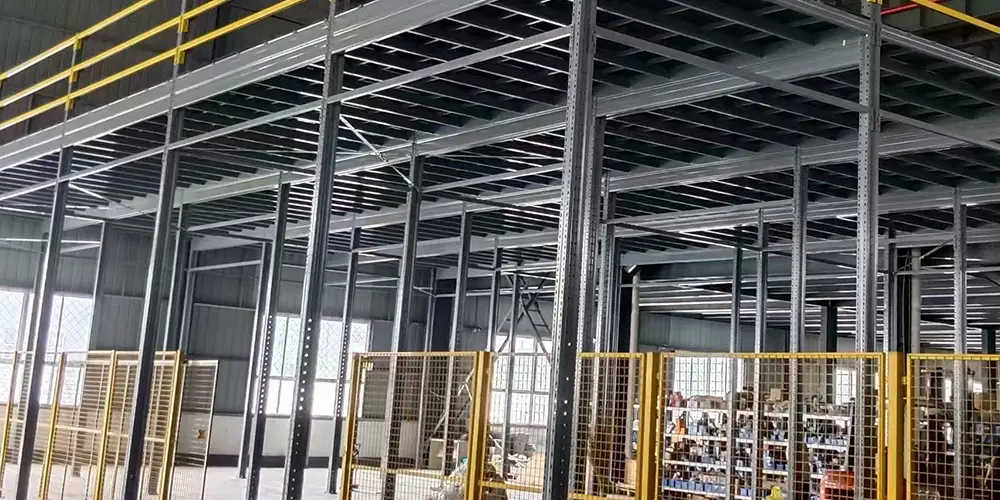
Integrated rack-supported mezzanine floors providing double or triple usable square footage above ground storage.
View Mezzanine Platforms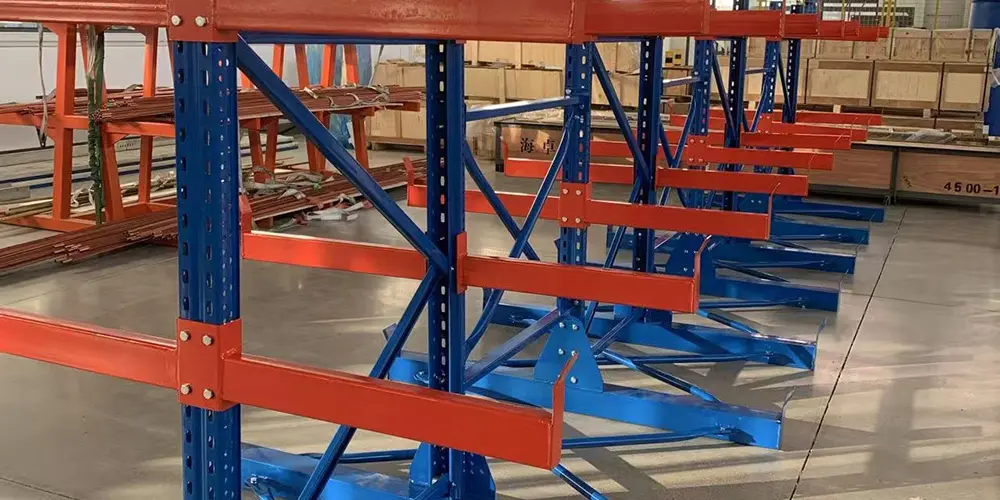
Unobstructed front access cantilever arms engineered for heavy timber, steel bars, tubing, and sheet materials.
View Heavy CantileverPartner with China's leading mobile rack storage manufacturers. Contact Guake Logistics Technology for an engineered proposal, CAD drawing layout, and transparent factory-direct quotation.
