


Explore our core engineered storage solutions manufactured directly in our Shandong manufacturing facilities, compliant with ISO9001, FEM 10.2.02, and ANSI MH16.1 standards.

Semi-automated deep-lane pallet storage using wireless battery-powered shuttles. Maximize cubic density and eliminate forklift rack travel.
Explore System Specs
Integrated rack-supported multi-level floor structures for hand-load picking, e-commerce fulfillment, and secondary storage decks.
Explore System Specs
Heavy-duty structural steel platforms providing clear-span multi-floor work zones, office installations, or heavy machinery placements.
Explore System Specs
High-density LIFO/FIFO storage engineered for uniform SKUs. Removes internal working aisles to double effective storage volume.
Explore System Specs
Dynamic 2-to-5 deep pallet loading per aisle face. Gravity-fed nested carts allow rapid LIFO rotation without entering rack lanes.
Explore System Specs
Heavy-duty selective racks mounted on automated electric mobile bases. Creates 100% pallet selectivity with only one single movable aisle.
Explore System Specs
Unobstructed arm columns specialized for long, bulky materials including steel pipes, timber profiles, aluminum extrusions, and sheets.
Explore System Specs
Ultra-high precision vertical rack architecture custom-fabricated for integration with stacker cranes, shuttle cars, and WMS/WCS software.
Explore System SpecsAnalyzing the macro-economic forces, real estate cost inflation, and industrial logistics optimization driving global demand for Chinese multi-tier rack engineering.
Industrial land acquisition costs across North America, Europe, and Asia-Pacific have surged by 42% over the last five years. Multi-tier racking systems unlock vertical storage height (up to 12-15 meters), transforming unused ceiling void space into high-value operational flooring. This doubles or triples effective square footage without increasing the physical facility footprint or expanding municipal property tax obligations.
Modern omnichannel fulfillment centers require split-case picking, rapid item access, and specialized SKU categorization. Multi-tier mezzanine shelving creates dedicated horizontal picking levels integrated with gravity chutes, belt conveyors, and vertical lifts. This architecture decreases order picking cycle times by up to 65% compared to single-level manual warehouse layouts.
Partnering directly with premier Chinese racking manufacturers like Guake Logistics Technology provides procurement teams with a 35-50% Total Cost of Ownership advantage. By combining high-yield cold-rolled steel processing, advanced robotic welding, and automated surface coating under strict ISO control, Chinese suppliers deliver structural integrity that fully complies with global safety codes at lower CAPEX.
A deep engineering dive into structural deflection limits, seismic mitigation design, cold-rolled section profiles, and mechanical structural integrity.
Guake multi-tier racking utilizes premium structural steel grades Q235B and Q355B (equivalent to ASTM A36 and ASTM A572 Grade 50). Upright columns are manufactured using continuous 18-stage cold-roll forming machines, producing complex multi-ribbed omega sections ($\Omega$) that deliver ultra-high moment of inertia and resistance against axial buckling.
Multi-tier mezzanines require specific flooring selection depending on pallet jack operation, foot traffic, and light transmission requirements:
Under maximum rated static live load ($W_{live}$), beam horizontal deflection ($\delta$) must strictly satisfy: $\delta \le \frac{L}{200}$ (where $L$ is the clear beam span). For multi-tier walkway support beams, deflection is capped at $\delta \le \frac{L}{300}$ to guarantee walking stability and eliminate vibration fatigue.
A quantitative comparison matrix evaluating capital expenditure, storage density, operational speed, and architectural requirements.
| System Architecture | CAPEX Cost / $m^2$ | Cubic Vol. Efficiency | Pallet / SKU Selectivity | Throughput Speed | Operational Flexibility |
|---|---|---|---|---|---|
| Multi-Tier Mezzanine Racking | Medium ($$) | Ultra High (85-90%) | 100% Direct Piece / Box Access | High (Multi-level simultaneous picking) | High (Reconfigurable) |
| Radio Shuttle Racking | Medium-High ($$$) | Very High (80-85%) | Batch / Lane Dependent | Very High (Automated shuttle movement) | Medium (Fixed pallet channels) |
| Heavy Steel Platforms | Medium ($$) | Moderate (Clear span floor) | 100% Open Space Access | Depends on equipment layout | Ultra High (Machinery/Office floor) |
| Selective Pallet Racking | Low ($) | Low-Medium (40-50%) | 100% Direct Pallet Access | Medium (Forklift aisle dependent) | High (Standard layout) |
| Full Automated ASRS System | Very High ($$$$$) | Maximum (90-95%) | 100% Automated System Access | Ultra High (Robotic crane speed) | Low (Fixed physical infrastructure) |
Custom structural engineering tailored to vertical market requirements: E-Commerce, Cold Chain, Automotive Parts, and Pharmaceutical Distribution.
3 to 4-tier rack-supported structures equipped with integrated carton live storage, pick-to-light systems, spiral chutes, and outbound belt conveyors. Enables thousands of pickers to work simultaneously on isolated floor tiers without congestion.
Optimized multi-tier layouts using hot-dip galvanized or specialized low-temperature powder-coated steel designed for sub-zero operations (-25°C to -30°C). High thermal efficiency reduces refrigerated volume loss per stored SKU.
Hybrid multi-tier mezzanine racks combining heavy-duty cantilever arms for exhaust pipes/bumpers with light-duty bin storage for gaskets, micro-fasteners, and electronic modules. Custom compartmentalized shelf dividers maximize organization.
Inside Guake Logistics Technology: 20,000+ $m^2$ state-of-the-art facility equipped with automated roll-forming, robotic welding, and environmental surface finishing.
High-precision automatic rolling mills guarantee profile dimension tolerances within $\pm 0.5\text{mm}$. Continuous punch indexing ensures exact beam-to-column connector alignment.
Automated ABB robotic arm welding workcells ensure deep weld penetration, zero spatter, and consistent fatigue resistance across all critical beam connector brackets.
Automated 9-stage pre-treatment wash followed by thermosetting epoxy-polyester powder coating (80-120 microns thickness) for maximum scratch and corrosion prevention.
Every manufacturing batch undergoes non-destructive load testing, spectral steel analysis, and salt spray testing under certified ISO 9001, ISO 14001, and CE systems.
From initial CAD layout drafting to final structural commissioning: How Guake manages global multi-tier racking projects seamlessly.
Browse our complete range of specialized warehouse rack components, cantilever systems, boltless shelving, and platform extensions.

Versatile heavy-duty shelving modules built with adjustable beam heights for commercial parts storage and maintenance workshops.
View Product Details
Freestanding arm racking engineered for light-to-medium long profiles, PVC tubing, molded trim, and sheet materials.
View Product Details
Rapid assembly rivet-lock shelving designed for manual archive hand-loading, spare parts rooms, and light e-commerce bins.
View Product Details
Wide-span column-supported structural platforms suitable for integrating heavy automated sorting conveyors and offices.
View Product Details
Multi-tiered organized bin shelving system optimized for high-density small parts picking and inventory sorting rooms.
View Product Details
Standard high-capacity selective racking engineered for maximum forklift accessibility and heavy unit load configurations.
View Product Details
Bespoke engineered multi-floor structures integrating staircases, safety handrails, pallet drop gates, and cat-walks.
View Product Details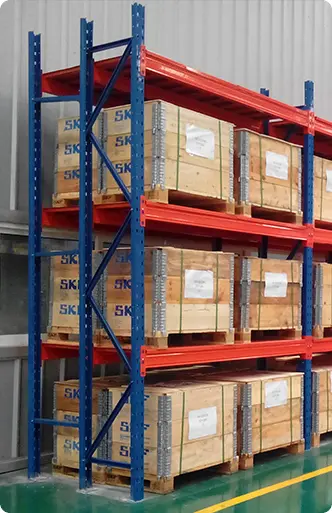
Integrated narrow-aisle (VNA) high-bay rack structures designed for precision reach-truck operations up to 15 meters high.
View Product DetailsIn-depth technical answers to structural, safety, economic, and logistical questions standard for enterprise buyers.
Engineering a multi-tier racking system requires a complete structural evaluation of both the rack framework and the concrete slab foundation. Critical parameters evaluated include:
Top-tier Chinese manufacturers like Guake Logistics Technology operate fully automated continuous roll-forming lines and robotic welding equipment that match Western manufacturing quality. Guake uses international structural design standards including FEM 10.2.02 (Europe), ANSI MH16.1 (USA), and AS4084 (Australia) while sourcing high-grade certified Q355B steel directly from major Chinese steel mills. This yields a 30% to 50% cost advantage in capital expenditure without compromising structural safety, material thickness, or structural longevity.
Multi-tier racking platforms must comply with municipal fire codes. Key design adaptations provided by Guake include:
Yes. Guake multi-tier mezzanine racks feature 100% bolted structural connections. No field welding is required during assembly. Upright frames, support beams, floor decking panels, and handrail systems can be unbolted, reconfigured for altered tier heights, expanded with additional bays, or fully dismantled and relocated to a new logistics facility as business requirements evolve.
Standard fabrication time at our Shandong facility is 15 to 25 business days following approval of CAD layout drawings and FEA structural calculations. For export logistics, components are packaged using protective corner guards, steel strap bundling, and specialized container loading strategies that maximize payload density—reducing international ocean freight costs per metric ton.
Walkway tiers designed exclusively for personnel foot traffic are typically rated at $300 - 500\text{ kg/m}^2$. If electric or manual pallet jacks operate on upper floor tiers, the structural framing is reinforced with heavy-duty C-channel sub-beams, thicker steel deck plates ($2.0\text{mm} - 3.0\text{mm}$), and dense column grid spacing to support concentrated wheel point loads up to $1500\text{ kg}$.
