


Custom-engineered racking systems manufactured to EN 15512, FEM 10.2.02, and RMI structural compliance. Explore our top 8 enterprise-grade storage configurations below.

Multi-tier mezzanine shelving system engineered to multiply usable floor area without building extensions. Ideal for e-commerce order picking.
View Product Details
Semi-automated deep lane pallet storage utilizing motorized radio shuttles. Maximizes cold storage volume and high-throughput lanes.
View Product Details
Heavy-duty bolted structural steel platforms supporting point loads up to 1,000 kg/m². Fully customizable beam spans and decking options.
View Product Details
High-density LIFO storage system removing aisle spaces. Allows forklifts to drive directly into rack lanes for uniform SKU storage.
View Product Details
2 to 5 deep pallet storage utilizing nested inclined carts. Gravity-fed system providing single-aisle loading and high SKU accessibility.
View Product Details
Automated pallet runner technology supporting both FIFO and LIFO operational flows. Minimizes forklift transit times inside high-bay bays.
View Product Details
High-density heavy-duty racks mounted on motorized mobiled bases. Opens a single working aisle on demand to achieve 85% footprint efficiency.
View Product Details
Industrial multi-tier rack-supported platforms tailored to warehouse ceiling clearances. Integrated with staircases, handrails, and pallet gates.
View Product DetailsThe global logistics and industrial sector is undergoing a structural transformation. Industrial real estate values across North America, Western Europe, and Asia-Pacific have risen sharply, driven by e-commerce expansion, regional nearshoring strategies, and stringent urban land zoning regulations. According to recent industrial market intelligence, prime warehouse rental rates in key logistics hubs have escalated at compound annual growth rates (CAGR) exceeding 6.8% over the past five years. Consequently, global enterprise logistics managers, Third-Party Logistics (3PL) operators, and industrial manufacturers can no longer justify expanding building footprints horizontally.
Instead, modern supply chain strategy dictates vertical spatial optimization—maximizing the ratio of usable cubic storage per square meter of concrete slab floor area. Converting traditional floor stacking or low-bay static layouts to engineered high-density pallet storage solutions (such as drive-in, push-back, radio shuttle, and automated AS/RS systems) enables facilities to increase storage capacity by 80% to 250% within the exact same structural footprint. This optimization directly reduces overhead lease costs, lowers per-pallet storage overhead, and drastically improves facility throughput efficiency.
Key Insight for Enterprise Procurement: Upgrading static warehouse layouts to high-density pallet storage solutions yields an average Return on Investment (ROI) period of 14 to 22 months through direct real estate lease savings and reduced operational forklift transport times.
Rapid expansion of consumer stock-keeping units requires high-selectivity racking combined with multi-tier picking mezzanines to handle fast-moving inventory and direct-to-consumer order fulfillment.
Refrigerated warehouse facilities face immense electricity expense. Deep-lane pallet shuttle racking compresses air space volume, reducing the kilowatt consumption required per refrigerated pallet position.
Geopolitical shifts and shipping delays have forced enterprises from "Just-in-Time" to "Just-in-Case" inventory models, driving urgent procurement demand for robust heavy-duty pallet racking systems.
China has solidified its position as the premier international hub for structural steel rack manufacturing. Located in Linyi City, Shandong Province—one of China's most robust industrial steel processing and logistics zones—Guake Logistics Technology (Shandong) Co., Ltd. embodies the technological capabilities of China's Industry 4.0 manufacturing evolution.
The manufacturing edge of Chinese pallet storage equipment relies on three core structural advantages: integrated raw material supply chains, precision automated roll-forming equipment, and advanced metallurgical surface protection treatment standardizations.
Guake utilizes certified cold-rolled structural steel coils (Q235B and high-yield Q355B grade steel). Q355B steel delivers superior yield strength (≥355 MPa) and tensile strength (≥470 MPa), allowing structural upright frames to sustain extreme load capacities while reducing total dead weight.
Manufacturing lines feature computer-controlled continuous roll-forming mills integrated with automated CNC laser punching units. This guarantees upright pitch hole center tolerances within ±0.5mm over 12-meter profile lengths, ensuring perfect beam connector engagement.
Upright frame bracing and heavy-duty beam connector claws are welded using automated multi-axis robotic MIG welding arms. Constant voltage arc welding eliminates human error, preventing weld porosity and cold joints for structural fatigue safety.
Every component undergoes an 18-stage automatic pre-treatment process—including acid rust removal, zinc phosphating, and pure water rinsing—followed by thermosetting epoxy polyester powder coating (film thickness ≥80μm), passing 1000-hour salt spray corrosion testing.
Selecting the optimal pallet storage solution requires balancing storage density, pallet selectivity (direct access), operational throughput, and investment capital. The technical matrix below provides engineering reference metrics across primary racking architectures.
| Storage System Type | Cubic Space Utilization | Pallet Selectivity | Operational Flow | Max Load per Level | Deflection Limit Standard | Primary Industrial Application |
|---|---|---|---|---|---|---|
| Selective Pallet Racking | 40% – 50% | 100% Direct Access | FIFO / LIFO | Up to 4,500 kg/pair | L/200 (EN 15512) | General Distribution, FMCG, High-SKU Logistics |
| Drive In / Drive-Thru Racking | 75% – 85% | 15% – 20% (Lane level) | LIFO (Drive-In) / FIFO | Up to 1,500 kg/pallet | L/200 Structural Rail | Uniform Bulk Goods, Beverage, Cold Storage |
| Push Back Racking (Nested Carts) | 65% – 75% | 30% – 40% (Lane face) | LIFO Flow | Up to 1,400 kg/cart | L/250 Cart Track | Medium-SKU Batch Storage, Buffer Zones |
| Radio Shuttle Racking System | 80% – 90% | 20% – 30% (Semi-Automated) | FIFO or LIFO | Up to 2,000 kg/shuttle | L/250 Precision Rail | Cold Storage (-30°C), Food Processing, High Throughput |
| Motorized Mobile Racking | 80% – 85% | 100% (Single dynamic aisle) | FIFO / LIFO | Up to 24,000 kg/bay | L/200 Floor Guide Rail | High-Value Inventory, Frozen Food, Limited Space |
| Mezzanine & Steel Platform | 100% Space Multiplier | 100% Manual / Conveyor | Continuous Access | 300 – 1,000 kg/m² | L/300 Floor Beam | E-Commerce Picking, Assembly, Modular Offices |
| Cantilever Heavy Racking | 60% – 70% | 100% Side Loading | Direct Access | Up to 3,000 kg/arm | L/150 Arm Limit | Steel Pipes, Extrusions, Timber, Sheet Plates |
Structural engineering of pallet racking systems manufactured by Guake Logistics Technology strictly adheres to global design protocols, including European EN 15512 (Adjustable Fabricated Steel Racking), FEM 10.2.02, and American RMI (ANSI MH16.1) standards. Key structural design metrics include:
When enterprise procurement managers and supply chain directors evaluate Chinese pallet storage manufacturers, technical compliance and logistical execution are vital. Sourcing pallet storage systems involves analyzing Total Cost of Ownership (TCO), material certification, container packing efficiency, and local installation guidance support.
Verified structural steel origin traceable back to major domestic steel mills (such as Shougang Group or Baosteel). MTC documentation confirms chemical composition (Carbon, Manganese, Silicon) and mechanical tensile properties prior to cold forming.
Validation of beam connector claw shear resistance, upright frame buckling capacity under axial compression, and stub column compression tests verified by ISO/IEC 17025 accredited testing bodies.
Optimized knock-down component design maximizing cubic meter capacity inside standard 40-foot High Cube (40' HC) shipping containers, utilizing steel bundling frames and protective edge corner guards to prevent transit scratching.
Provision of step-by-step 3D installation CAD assemblies, detailed component packing lists, video manuals, and remote/on-site engineering installation supervision for rapid site commissioning.
Different industrial sectors demand specialized racking configurations engineered for specific operational environments, environmental temperatures, and pallet handling equipment.
Operating Temp: -25°C to -30°C
Optimal Solution: Radio Shuttle Racking or Mobile Racking Systems.
Engineering Note: Steel components use cold-resistant powder coatings and special low-temperature lubricants for shuttles, maximizing expensive refrigerated space.
Load Profile: Heavy engine blocks, stamping dies, raw metal bars.
Optimal Solution: Heavy-Duty Selective Racking & Cantilever Systems.
Engineering Note: Custom steel decking, coil cradles, and thick beam profiles designed for heavy forklift impacts.
Operation: High SKU variety, rapid piece picking, carton flow.
Optimal Solution: Multi-Tier Mezzanine Platforms & Selective Racking.
Engineering Note: Integrates gravity carton flow beds, automated belt conveyors, and integrated catwalk floors.
Founded in 2010 in Linyi, Shandong, Guake is a premier designer, manufacturer, and system integrator of intelligent warehouse racking equipment. Our integrated services span engineering layout design, structural calculation, precision manufacturing, global shipping, and on-site installation guidance.
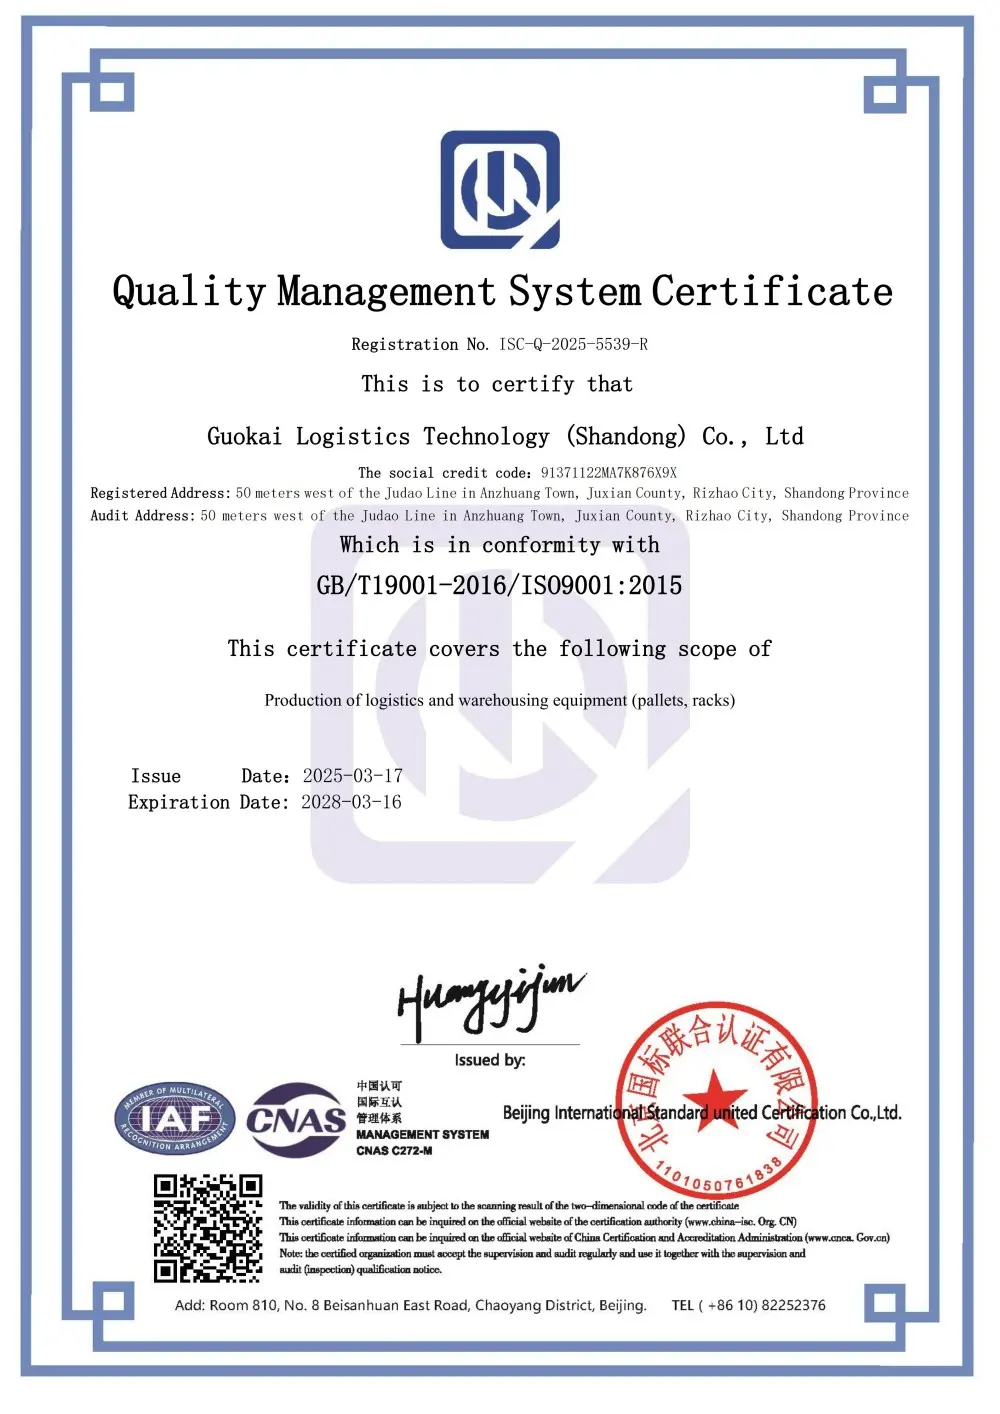
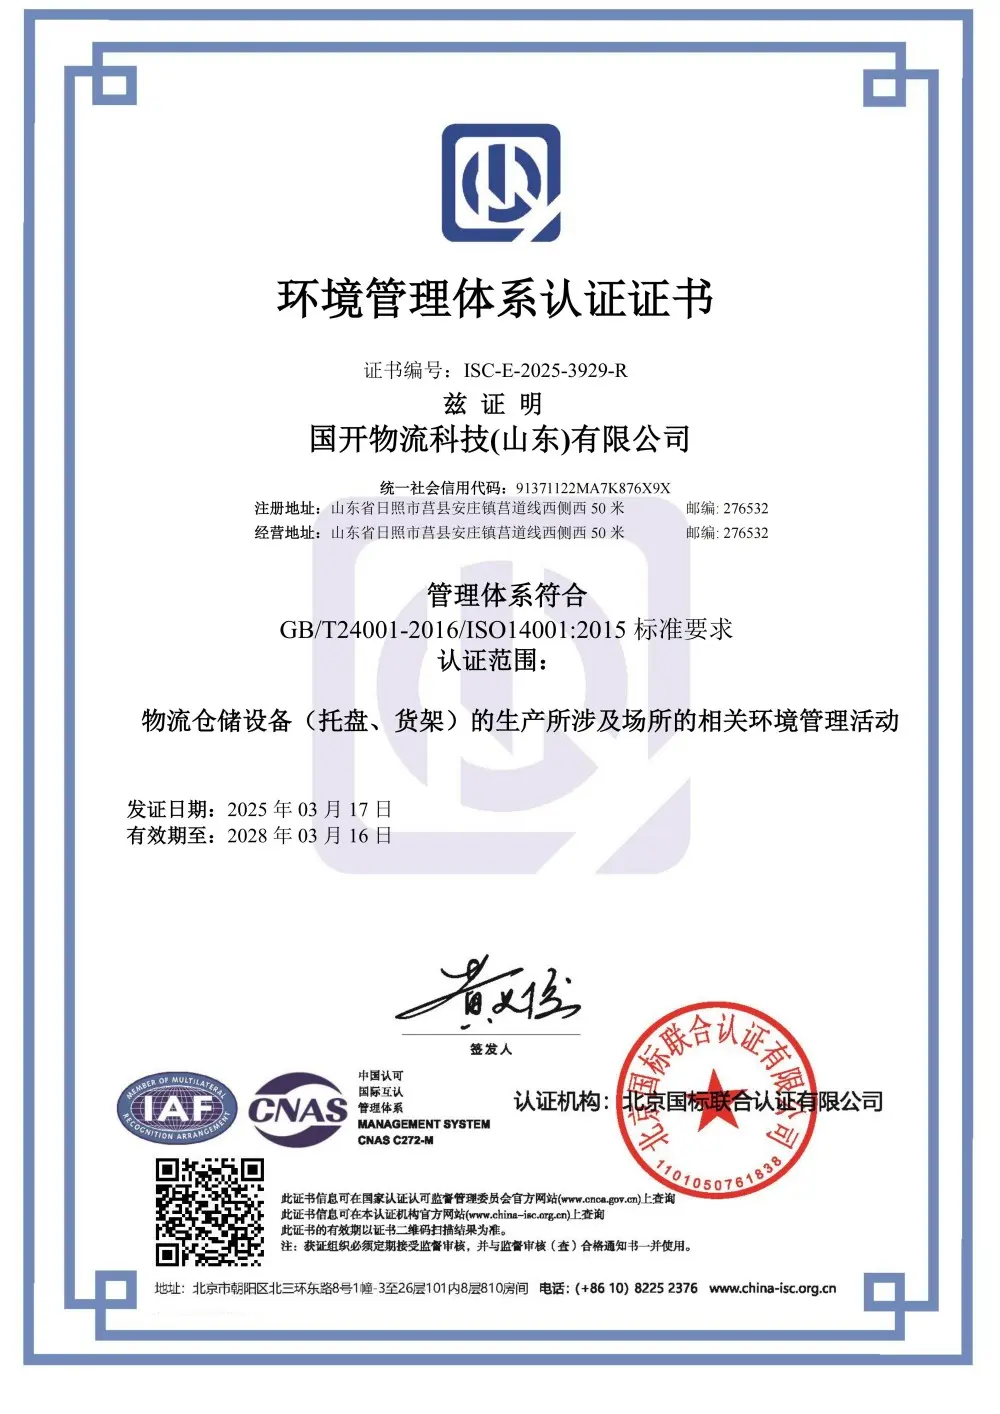
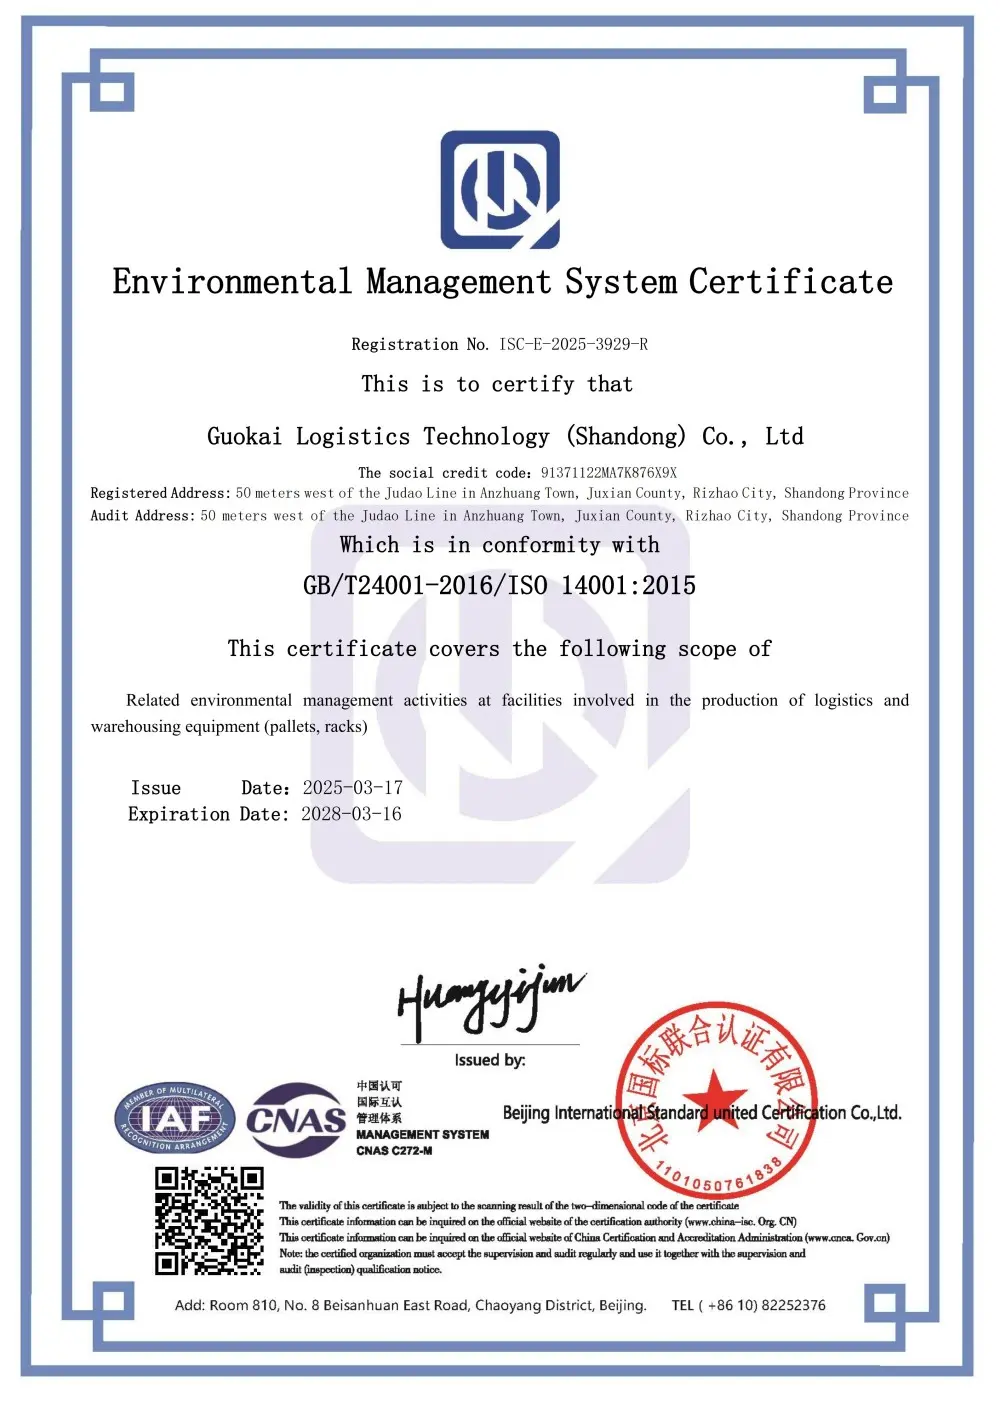
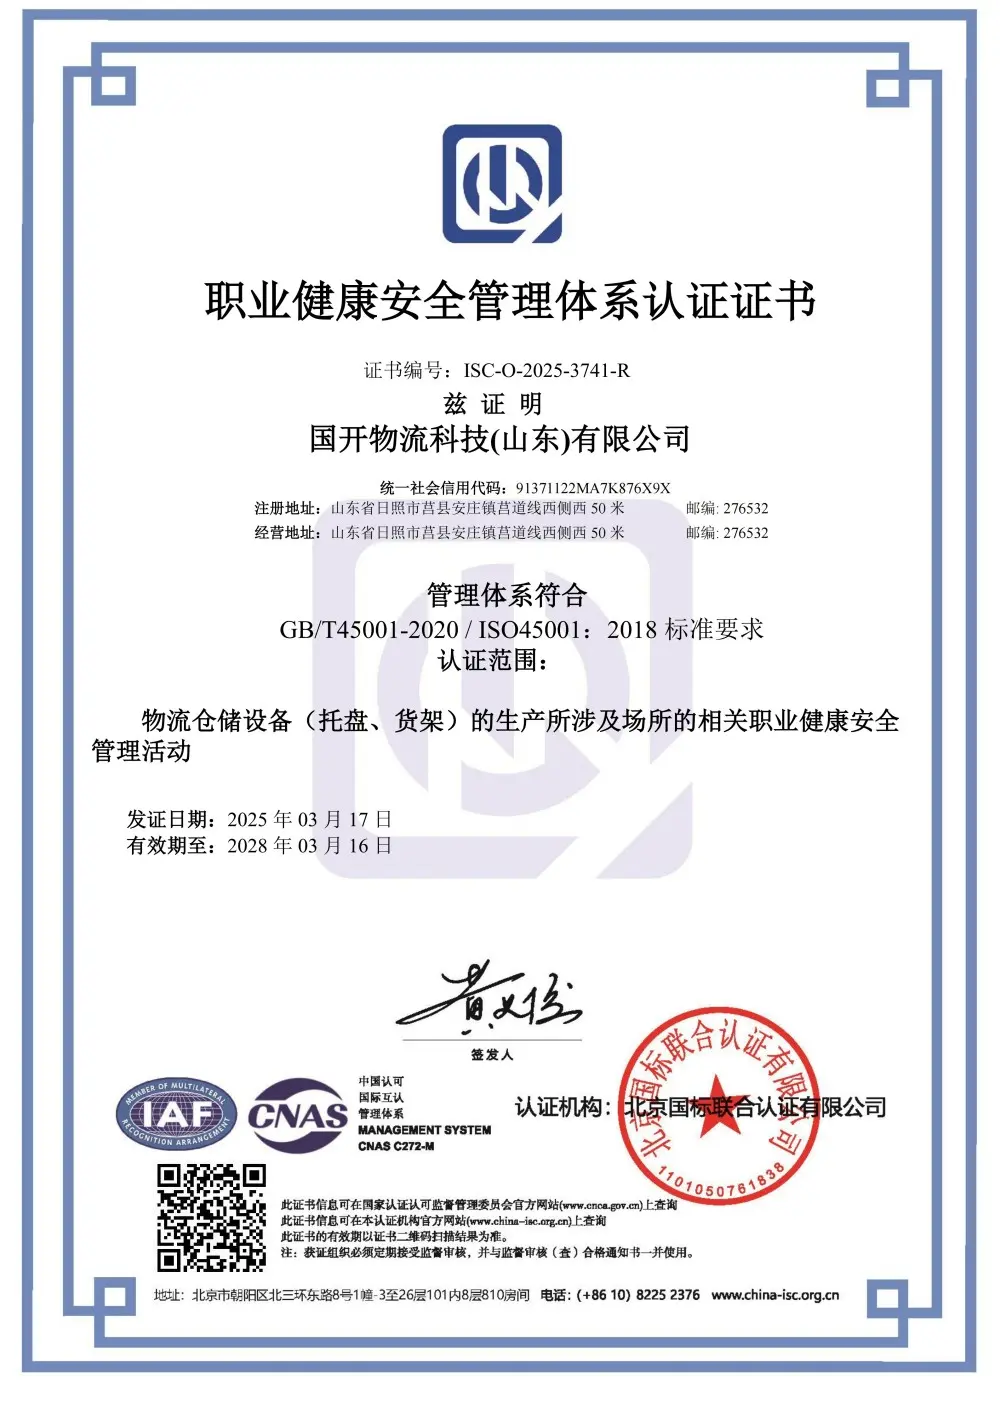
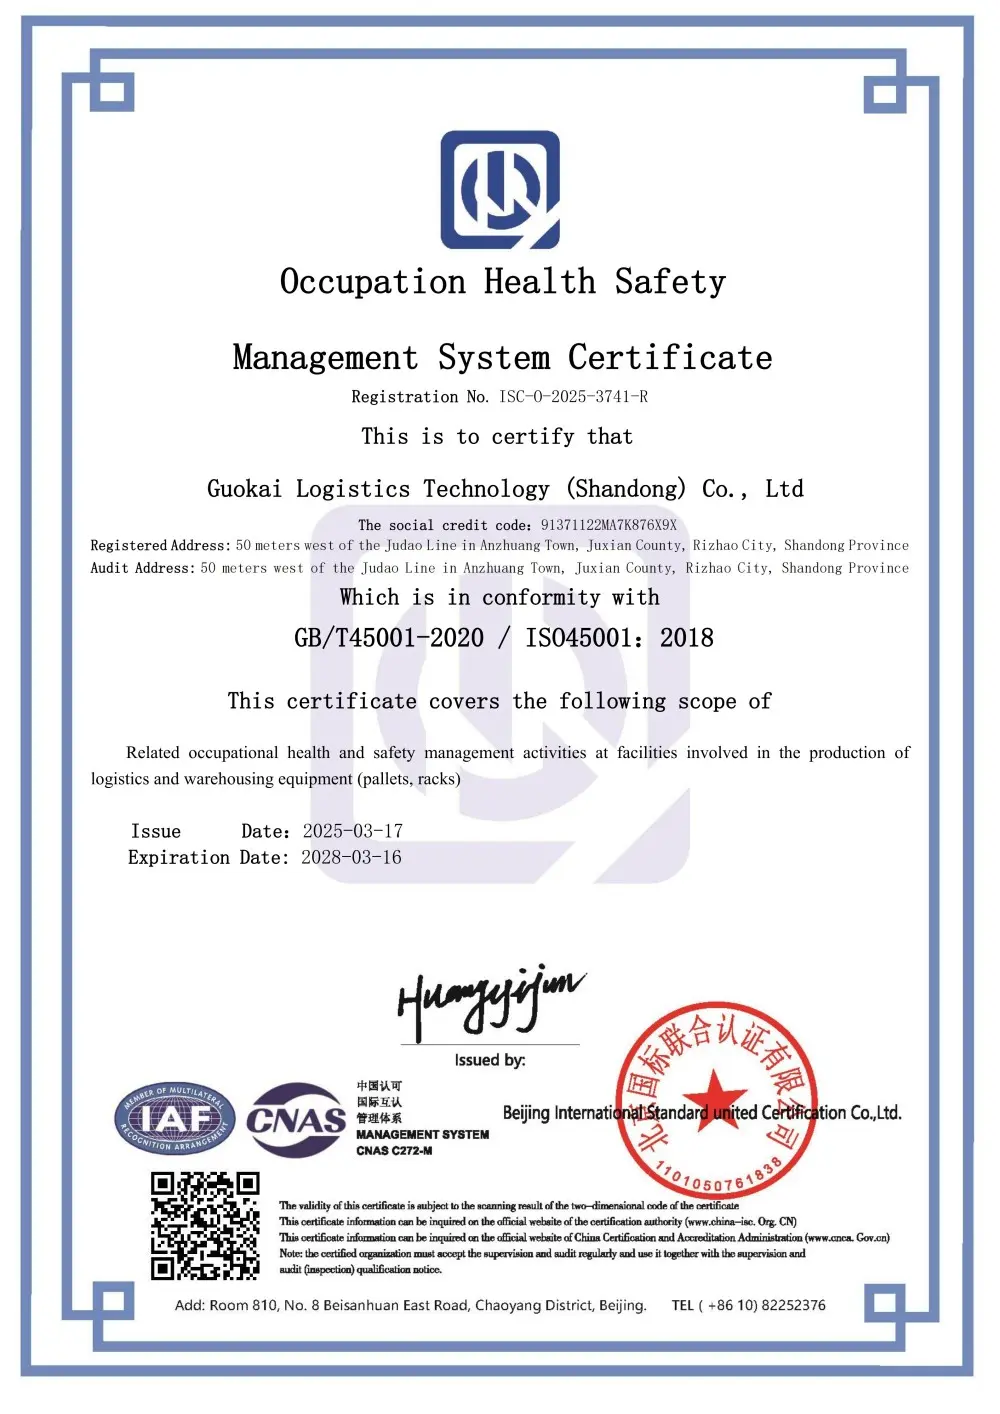
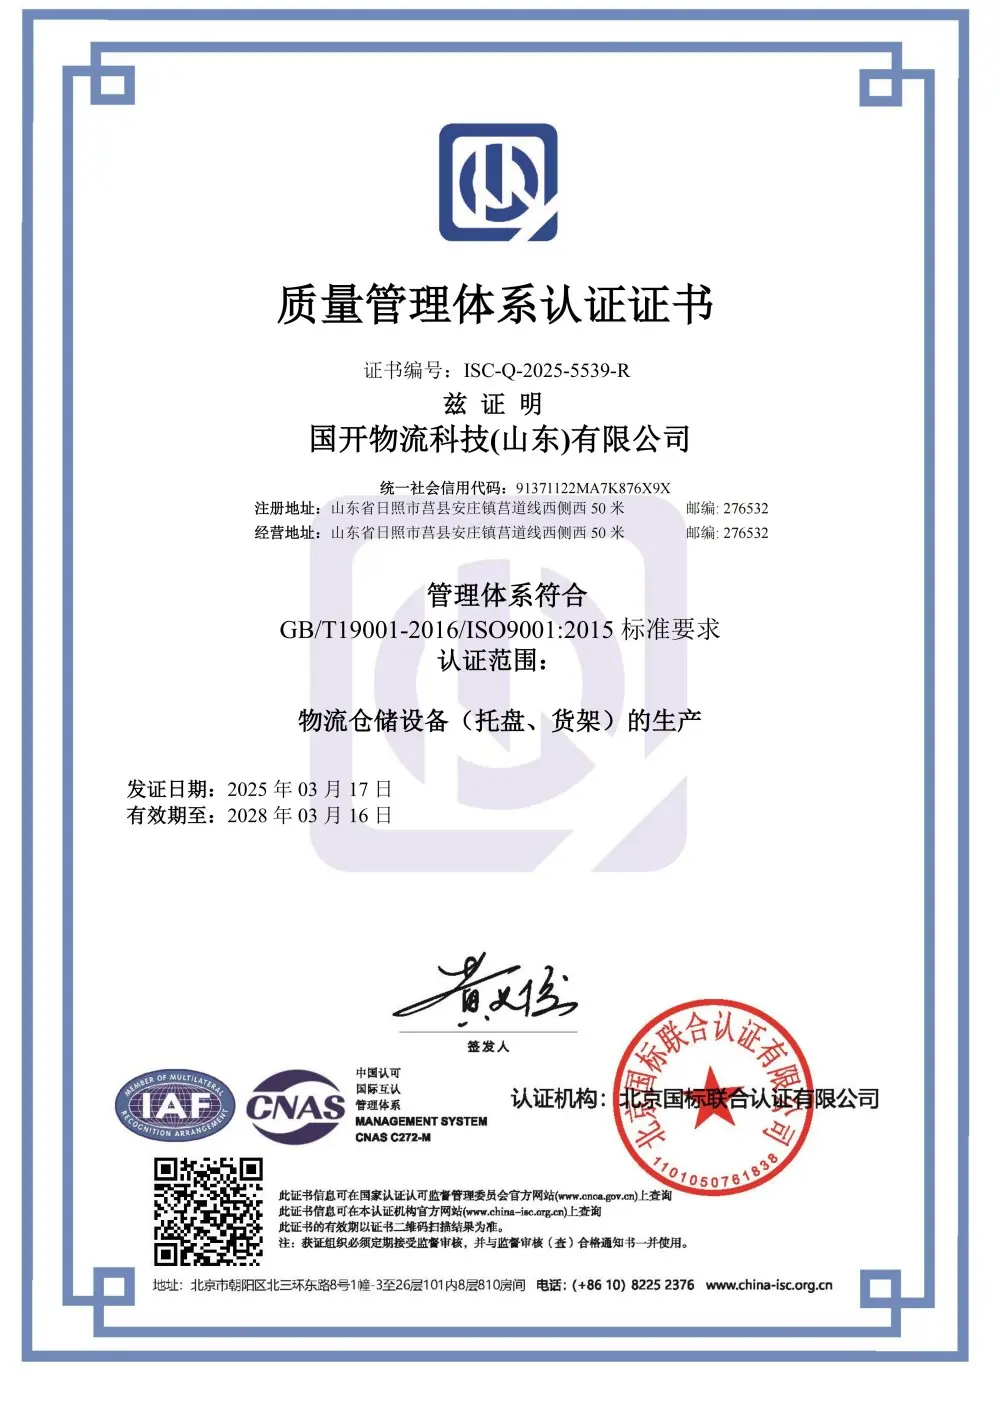
Comprehensive technical and logistical answers regarding system selection, layout design, quality testing, and international shipping.
Guake Logistics Technology manufactures a full range of high-performance warehousing solutions including:
Yes. Our structural engineering team provides complete 2D CAD layouts and 3D BIM proposal renderings. To initiate layout planning, simply provide us with:
Selection depends on your SKU diversity, selectivity requirements, and throughput demand:
Yes. Every exported project includes comprehensive installation drawings, structural assembly diagrams, component packing manifests, and step-by-step video guidance. Additionally, for major enterprise projects, we deploy senior site engineers for on-site installation supervision, commissioning, and safety inspection.
Quality control is maintained through rigorous multi-stage testing:
Yes. All structural dimensions—including upright frame height, depth, beam span length, load capacities per level, beam connector pitch (50mm/75mm), decking types (wire mesh, steel panel, timber), and RAL surface powder colors—are completely customized to match your building and operational specifications.
For standard heavy-duty selective or shuttle racking systems, concrete slab floor thickness should be at least 150mm to 200mm with minimum compressive strength grade C25 or C30 (25-30 MPa). Baseplate anchor bolts require flat slab floor tolerances compliant with DIN 18202 or ASTM E1155 F-number standards to prevent structural frame leaning.
Direct supply of specialized cantilever racking, heavy-duty beam racks, modular shelving systems, and custom industrial platforms direct from Shandong, China.

Heavy-duty column-and-arm racking engineered for storing long structural goods, pipes, aluminum extrusions, and timber packs.
View Product Details
Standard selective structural steel pallet racks featuring adjustable drop-in step beams and high load-bearing capacity.
View Product Details
Flexible arm racking designed for lighter bar stock, plastic conduits, and sheet materials with unobstructed front access.
View Product Details
Quick-assembly clip-in shelving units engineered for manual hand-picking warehouses and spare parts rooms.
View Product Details
Heavy boltless steel shelving units providing modular storage for light industrial, commercial, and workshop applications.
View Product Details
Heavy structural steel floor platforms providing clear spans beneath for forklift travel and active working space above.
View Product Details
Multi-tier light duty shelving arrays featuring integrated stairs and walkways for high-density small parts cataloging.
View Product Details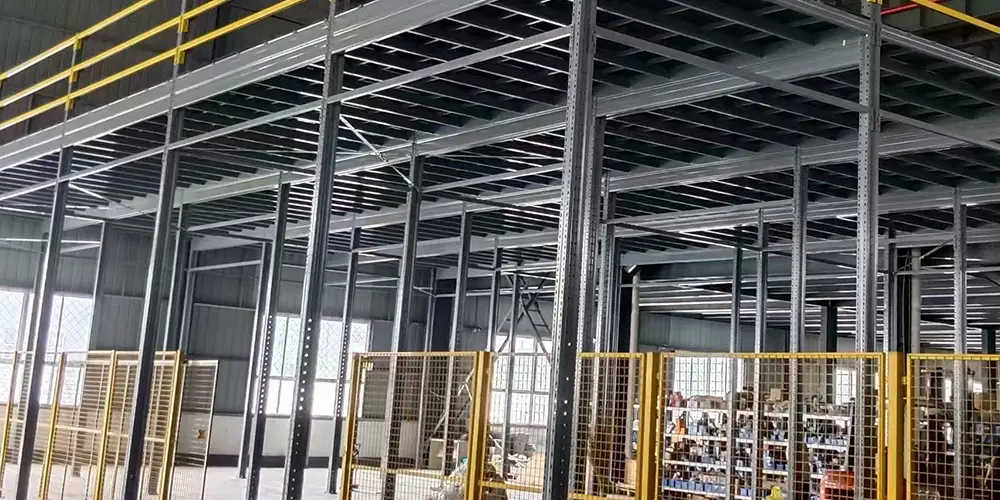
High-capacity structural mezzanine floor decks engineered with steel bar grating or heavy checker plate surfaces.
View Product DetailsSend us your warehouse CAD drawings or pallet specifications today. Our senior structural engineers will provide a customized 3D layout design and factory-direct quote within 24 hours.
