


Precision-engineered pallet racks, automated shuttle platforms, and multi-tier structural solutions manufactured directly in Shandong, China.

Semi-automated radio shuttle systems designed for ultra-dense pallet storage with high throughput efficiency.
China Shuttle Racking Manufacturer
Multi-tier steel rack platforms multiplying usable vertical overhead floor space without structural expansion.
China Mezzanine Racking Factory
Heavy-duty bolted structural steel decks built to sustain heavy equipment, picking aisles, and office integration.
Steel Platform Racks Factory
Maximum cubic density storage ideal for high-volume homogeneous goods and cold-storage facilities.
Drive In Racking Suppliers
Nested cart architecture allowing 2 to 5 deep pallet loading with dynamic gravity-fed access.
Push Back Racking Factory
Motorized movable rack bases on floor rails that unlock 100% pallet selectivity while saving 50% aisle space.
Mobile Racking Manufacturer
High-speed intelligent pallet shuttles supporting both FIFO and LIFO operational logic.
Radio Shuttle Racking Factory
Custom structural cantilever designs optimized for long, heavy, or non-standard industrial loads.
Special Purpose RackingIn an era defined by rapid e-commerce growth, volatile supply chains, and rising industrial land costs ($150 to $400 per square meter in tier-1 logistics hubs across North America and Europe), enterprise logistics operators can no longer rely on traditional horizontal footprint expansion. Modern warehouse managers face the imperative of optimizing cubic space utilization.
Racked storage systems represent the structural backbone of physical intralogistics. From selective beam pallet racks to automated high-bay racking systems (ASRS), industrial storage equipment directly impacts throughput speed, SKU density, structural safety, and operational overhead. Selecting an experienced China racked storage manufacturer offers global enterprises a strategic combination of structural engineering expertise, metallurgical scalability, and substantial Capital Expenditure (CapEx) savings.
Industrial racking is not merely steel shelving; it is structural engineering designed to support multi-ton live loads safely under static and dynamic loading conditions.
We utilize prime hot-rolled cold-formed steel coils (such as Q235B and Q355B structural steel grade). Structural upright columns feature continuous multi-fold profiles (up to 13-15 bends) that exponentially increase section modulus and buckle resistance while minimizing overall weight.
Every customized racking configuration undergoes rigorous computer-simulated Finite Element Analysis (FEA) testing. This ensures full compliance with international standards such as FEM 10.2.02 (European standard), RMI (USA standard), and AS4084-2012 (Australian code).
Components pass through a 9-stage automatic chemical pretreatment line before receiving an electrostatic epoxy-polyester powder coating (60-80μm thickness). For outdoor or corrosive cold-room applications, heavy-duty hot-dip galvanizing guarantees 25+ years of zero oxidation.
Comparing structural mechanics, pallet selectivity ratios, inventory flow principles, and optimal use cases.
The Radio Shuttle system combines high-density deep-lane storage with semi-automation. A battery-powered wireless shuttle vehicle runs on rails inside the storage channels, lifting and carrying pallets to their destination without forcing forklifts to enter the rack lanes.
Mezzanine racking systems utilize rack uprights or heavy structural steel columns to support a second or third elevated floor deck. This transforms unused vertical height into usable floor space for manual small-parts picking, packing stations, assembly lines, or modular executive offices.
Drive-in racking eliminates working aisles by allowing forklifts to drive straight into continuous storage lanes resting pallets on continuous side rails. Push-back racking utilizes nested carts on inclined rails where each incoming pallet pushes existing pallets back up to 5-6 deep.
Heavy-duty mobile racking mounts traditional selective pallet racks onto motorized chassis moving along floor tracks, opening only one aisle at a time. Cantilever racking features extended unbolted load arms for holding long profiles, pipes, timber, and sheet metal safely.
Located in Shandong, China—the world’s epicenter for high-grade steel output and machinery fabrication—Guake Logistics Technology leverages a fully integrated industrial supply chain ecosystem. Direct access to raw steel mills reduces raw material procurement costs and guarantees batch-to-batch metallurgical consistency.
Our manufacturing facilities utilize high-speed automated roll-forming production lines, robotic continuous fillet welding, and high-precision laser profiling equipment. This automation enables rapid production cycles, strict tolerance compliance (under ±0.5mm), and significant labor efficiency gains—passing direct Capital Expenditure (CapEx) savings of 30% to 50% to global procurement partners without sacrificing structural standards.
Schedule a Factory Video AuditHow customized racked storage configurations solve region-specific logistics challenges around the world.
In North American megacities, high throughput velocity is vital. Deploying multi-tier mezzanine picking platforms combined with heavy-duty teardrop pallet racking allows 3PL operators to organize multi-SKU e-commerce fulfillment lines while utilizing vertical warehouse clearance up to 40 feet.
European energy costs demand extreme volumetric storage density in refrigerated warehouses. Utilizing radio shuttle racking and motorized mobile racking drastically cuts the refrigerated air cubic meter footprint per stored pallet, reducing facility operating expenses by up to 40%.
Fast-growing industrial sectors in the GCC and Southeast Asia demand heavy structural steel platform racks and outdoor cantilever systems capable of withstanding extreme ambient temperatures, humidity, and high structural static loads for oil, gas, and construction materials.
The next decade of industrial storage moves beyond static steel framework. Modern facilities are transitioning to Rack-Supported Buildings (ASRS), where the high-bay racking structure supports both the internal load and the external roof and wall cladding.
Furthermore, integration with Autonomous Mobile Robots (AMRs) and automated Guided Vehicles (AGVs) requires hyper-precise rack manufacturing tolerances (below ±1.0mm vertical alignment across 20-meter heights) and specialized floor rail embedments to guarantee optical sensor alignment.
Sensors embedded in upright columns detect forklift impact forces and structural overload strain in real-time.
Transitioning to low-carbon zero-VOC powder coatings and recycled high-strength alloy steels.
3D CAD/BIM integration allowing warehouse digital twins to simulate throughput bottlenecks dynamically.
Use this quantitative engineering matrix to shortlist the optimal racking architecture for your facility parameters.
| Racking Architecture | Volumetric Storage Density | Pallet Selectivity | Handling Equipment Required | Relative CapEx / Pallet | Optimal SKU Profile |
|---|---|---|---|---|---|
| Selective Pallet Racks | Standard (40-50%) | 100% Direct Access | Standard Reach / Forklift | Low ($) | High SKU variety, fast picking |
| Radio Shuttle Racking | Ultra High (80-90%) | Batch / Lane Access | Forklift + Shuttle Robot | Medium-High ($$$) | Low SKU count, bulk storage, cold chain |
| Push Back Racking | High (65-75%) | Lane Face Access (2-6 Deep) | Standard Counterbalance | Medium ($$) | Medium SKU count, medium rotation |
| Drive-In Racking | Very High (75-85%) | Last-In, First-Out (LIFO) | Specialized Narrow Forklift | Low-Medium ($$) | Homogeneous goods, seasonal storage |
| Motorized Mobile Racking | Very High (85-90%) | 100% Selective (On Demand) | Standard Reach Truck | High ($$$$) | High-cost space, cold storage hubs |
| Mezzanine Platforms | 200-300% Floor Area | 100% Manual / Conveyors | Staircases / Goods Lifts | Medium ($$$) | Small-parts picking, e-commerce packing |
When requesting structural design proposals from China racked storage manufacturers, supply the following technical parameters to ensure rapid and accurate CAD layout generation:
Direct answers to the engineering, manufacturing, and international procurement queries most frequently asked by global facility managers.
Select from our certified heavy-duty shelving, cantilever racks, shuttle systems, and steel structure platforms.

High-durability boltless metal shelving units designed for versatile light-to-medium hand-loaded picking.
View Shelving Range
Adjustable continuous arm racking for organized lateral loading of timber, tubing, and plastic extrusions.
View Cantilever Racks
Rapid assembly clip-in shelving systems ideal for commercial stockrooms and archive storage.
View Screw-Free Series
Structural steel beams and decking configured for heavy overhead machinery floor space expansion.
Steel Platform Systems
Multi-tier manual bin storage structures for dense small-parts e-commerce order picking.
View Multi-Layer Shelving
High-capacity selective beam racking with safety locking pins and adjustable upright beam pitch.
Heavy-Duty Pallet Racks
Rack-supported mezzanine catwalk floors engineered for dual-purpose pallet and carton picking.
China Mezzanine Shelving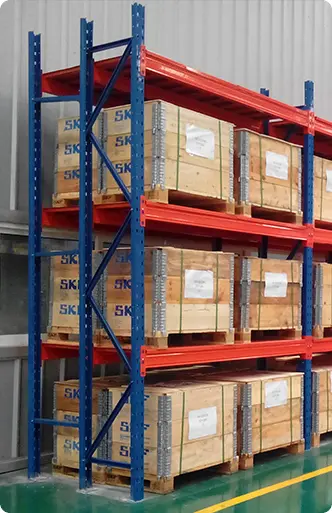
Semi-automated radio shuttle pallet systems designed for high-density warehouse storage efficiency.
China Shuttle SystemsTransform your facility floor plan into a high-density, highly efficient intralogistics asset. Contact Guake Logistics Technology (Shandong) Co., Ltd. for custom CAD drawings, FEA calculations, and direct factory quotation.
Consult with our logistics technology specialists for immediate technical support:
