


Discover our factory-direct structural rack systems designed for heavy-duty industrial logistics, automated warehousing, and high-density inventory environments.

Multi-tier heavy-duty structural steel platforms maximizing overhead spatial utilization without structural modifications.
View Details
Integrated mezzanine shelving platforms engineered for high SKU count picking operations and multi-level floor expansion.
View Details
Semi-automated radio shuttle pallet runner system providing maximum cubic storage density with FIFO/LIFO capabilities.
View Details
Continuous lane pallet racking system eliminating aisle space for homogeneous, high-volume inventory storage.
View Details
Nested cart dynamic racking allowing 2 to 5 pallet deep storage with aisle-facing loading and retrieval efficiency.
View Details
Heavy structural beam platforms designed for secondary floor creation, office space integration, or picking zones.
View Details
Motorized mobile bases mounted on floor rails, offering 100% pallet selectivity while saving up to 50% aisle space.
View Details
High-speed robotic shuttle carrier system optimizing cold storage and high-throughput warehouse logistics operations.
View DetailsThe global industrial warehouse storage and heavy-duty steel rack construction industry is undergoing a structural paradigm shift. Driven by skyrocketing commercial real estate prices, post-pandemic supply chain recalibrations, and the unprecedented surge in cross-border e-commerce, enterprise logisticians are no longer viewing warehouse racking as mere cold-rolled steel static shelving. Instead, racking construction has evolved into a highly sophisticated, structural civil engineering discipline that interfaces directly with automated material handling systems, artificial intelligence (WMS/WCS), and seismic structural safety frameworks.
As international supply chains demand higher throughput and denser cubic volumetric space utilization, sourcing from qualified China racks construction suppliers & factories has become a strategic priority for Fortune 500 logistics operators, 3PL providers, and cold-chain conglomerates worldwide. Shandong, China—and specifically the industrial manufacturing hub surrounding Guake Logistics Technology—has established itself as the global epicenter for precision cold-formed structural steel roll-forming, robotic welding, and automated surface powder-coating technologies.
In modern industrial facilities, land availability constraint is the single largest driver of operational expenditure. Traditional wide-aisle pallet racking layouts utilizing standard counterbalance forklifts utilize less than 40% of a facility's total cubic volume. Contemporary warehouse engineering aims for 80% to 90% volumetric utilization through tall-bay structural steel construction exceeding heights of 15 to 40 meters.
However, constructing vertical racking at these heights introduces complex civil engineering challenges. Racking frameworks must withstand dynamic structural forces including sway deflection, harmonic vibration, forklift impact forces, asymmetrical pallet loading, and seismic acceleration vectors. Tier-1 Chinese racking factories now utilize advanced Finite Element Analysis (FEA) computer simulation to model yield stress points, section moduli, and structural buckling behaviors under extreme multi-directional loads before any steel beam is roll-formed.
The safety and longevity of an industrial warehouse racking system depend entirely on the mechanical properties of the underlying raw steel, structural profile geometry, and surface protection technology. Below is a detailed breakdown of the technical standards adhered to by leading Chinese industrial racking manufacturers.
Our upright columns and load beams are roll-formed using high tensile strength cold-rolled structural steel (Q235B and high-yield Q355B equivalent to ASTM A572 Grade 50). This guarantees maximum yield strength, resistance to permanent deformation, and superior performance under extreme thermal fluctuation in cold storage settings down to -30°C.
The structural integrity of upright frames relies on multi-fold column profile geometries (up to 13 to 15 bends along the cross-section). Multi-ribbing exponentially increases the section modulus and torsional rigidity, permitting higher load carrying capacities with optimized steel gauge thickness.
Components undergo an automated 9-stage pre-treatment wash including zinc-phosphate etching, followed by thermosetting electrostatic epoxy-polyester powder coating (60-80 microns thickness) baked at 200°C. This yields high resistance to impact chipping, moisture oxidation, and industrial chemical exposure.
When procurement managers evaluate China warehouse racking manufacturers, structural engineering certification is non-negotiable. Qualified systems engineered by Guake Logistics Technology adhere strictly to global structural codes:
No two warehouse operations are identical. A high-performing racks construction supplier must design systems tailored around specific SKU velocity profiles, load geometry, environmental conditions, and mechanical handling equipment (MHE).
Challenge: Refrigerated and frozen warehouse space operates at extreme energy costs per cubic meter (-25°C to -30°C), demanding maximum storage density without mechanical failure.
Engineering Solution: Implementation of automated Radio Shuttle Racking Systems or Mobile Racking Systems utilizing low-temperature cold-rolled structural steel, anti-freeze lithium batteries, and galvanized anti-corrosion coatings.
Challenge: Omnichannel retailers require fast piece-picking access, multi-tier floor management, and seamless integration with conveyor belts and Autonomous Mobile Robots (AMRs).
Engineering Solution: Multi-story Mezzanine & Steel Platform Racks featuring integrated steel decking, safety mesh surrounds, chute drop zones, and heavy-duty stairwells engineered for high foot traffic.
Challenge: Storing heavy engine blocks, metal dies, long steel pipes, sheet metal, and irregular raw material profiles safely.
Engineering Solution: Heavy-Duty Special Purpose Cantilever Racking engineered with freestanding columns and adjustable load-bearing arms designed for side-loading overhead cranes and heavy reach trucks.
Challenge: Large batch sizes of homogeneous palletized products requiring minimal SKU picking diversity but maximum floor space compaction.
Engineering Solution: Deep-lane Drive-In Racking and Push Back Racking Systems eliminating intermediate operating aisles to boost pallet capacity by up to 75%.
The industrial storage industry is rapidly converging with robotics, industrial IoT (IIoT), and sustainable green manufacturing. China's leading racking factories are pioneering key technological developments designed to future-proof global logistics hubs over the next decade.
Transition from manual forklift storage toward seamless integration of 4-way radio shuttles with automated guided vehicles (AGVs) and autonomous mobile robots (AMRs). Racking structures will feature standardized sensor reflectors and high-precision rack alignment rails.
Embedded strain-gauge micro-sensors and optical deflection monitors directly integrated into critical upright frames and load beams. Real-time telemetry alerts facility managers to structural overload, seismic micro-fractures, or accidental forklift impact stress.
Implementation of 100% green hydrogen-reduced steel alloys for ultra-low carbon footprint compliance, alongside super-tall autonomous AS/RS (Automated Storage and Retrieval Systems) reaching heights over 45 meters using modular self-assembling rack structures.
Use the structural selection matrix below to analyze performance trade-offs between storage density, pallet selectivity, inventory handling model, and capital expenditure (CapEx) investment.
| Racking Construction System | Volumetric Density | Pallet Selectivity | Inventory Handling | Recommended Aisle Width | Primary Industrial Use Case |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (40-50%) | 100% Direct Access | FIFO / LIFO | 3.0m - 3.5m (Standard) | High SKU variety, fast picking, general distribution. |
| Drive-In Racking | Very High (75-85%) | Low (Per Lane) | LIFO | Forklift drives into lane | Bulk homogeneous stock, seasonal goods, cold storage. |
| Push Back Racking | High (65-75%) | Medium (Lane Face) | LIFO (2-5 Pallets Deep) | 3.0m - 3.2m | Medium SKU counts requiring high density with fast access. |
| Radio Shuttle Racking | Maximum (85-90%) | Controlled Batch Access | FIFO / LIFO (Robotic) | Single Transfer Aisle | Cold storage, food & beverage, high-throughput fulfillment. |
| Mobile Racking System | Ultra High (85-90%) | 100% (Moving Aisles) | FIFO / LIFO | One Dynamic Aisle | High floor-cost facilities, freezer rooms, archive storage. |
| Steel Platform & Mezzanine | Floorspace Doubling | Manual / Modular | Multi-Level Access | Custom Walking Aisles | Small-parts picking, e-commerce, office floor creation. |
Founded in 2010 in Linyi City, Shandong Province, Guake Logistics Technology (Shandong) Co., Ltd. has grown into one of Northern China’s premier manufacturers of commercial warehouse racking systems and intelligent storage equipment. Operating a modernized production facility spanning over 20,000 square meters, our facility houses high-precision CNC roll-forming lines, automated laser cutting machines, robotic welding cells, and an eco-friendly electrostatic powder coating line.
From initial site survey CAD layout planning and structural FEA calculations to fabrication, international container packing, overseas installation supervision, and commissioning, we provide a single point of technical accountability.
Every batch of raw coil steel undergoes laboratory tensile testing. Dimensions, beam drop tolerances, weld penetration, and powder coat thickness are strictly logged under our certified ISO 9001 quality management protocol.
Our solutions are deployed across Southeast Asia, Europe, the Middle East, Australia, North America, and South America. We provide comprehensive installation documentation, 3D exploded assembly diagrams, and dedicated on-site remote engineering support.
Browse our comprehensive selection of specialized racking structures, heavy-duty shelving, cantilever frames, and automated high-bay components.

Cantilever racking systems designed for storing long pipes, timber, steel tubes, and heavy structural profiles.
View Details
Standard adjustable structural beam pallet racking providing 100% direct selectivity for heavy industrial pallet loads.
View Details
Modular industrial metal shelving units for light-to-medium hand-loaded picking and parts organization.
View Details
Arm-supported racking without front column obstruction, perfect for medium-weight plastic pipes and extrusions.
View Details
Heavy structural I-beam platforms creating mezzanine level work areas for industrial manufacturing equipment.
View Details
Rapid assembly interlocking metal shelving designed for commercial retail backrooms and e-commerce picking.
View Details
Versatile multi-tier shelving units for bin storage, archive boxes, and lightweight inventory management.
View Details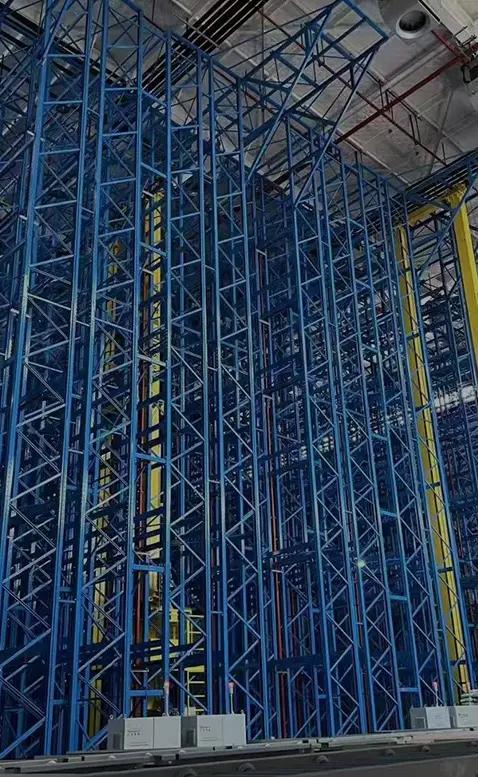
Ultra-precise high-bay steel rack structures designed for automated stacker crane integration and digital WMS control.
View DetailsContact our senior structural racking engineers today for a complimentary CAD floor plan proposal, structural FEA load calculation, and factory-direct quotation.
