


Factory-direct engineered racking and structural steel platform solutions certified to ISO9001, FEM 10.2.02, and ANSI/RMI MH16.1 specifications.

Semi-automated deep-lane pallet storage using battery-powered shuttles for ultra-high space utilization.
Explore Shuttle Racking
Multi-tier structural steel racking platforms doubling overhead usable square footage without building expansion.
View Mezzanine Systems
Freestanding structural column-and-beam platforms with up to 1,000 kg/m² surface load capacities.
View Steel Platforms
Eliminates forklift aisles to store large quantities of homogeneous SKUs in continuous LIFO bays.
View Drive-In Racking
Nested cart storage system supporting 2 to 5 pallets deep with immediate access to single aisle faces.
View Push Back Systems
Integrates heavy-duty racking columns as structural support for high-bay multi-level order picking.
Explore Mezzanine Racking
Heavy-duty pallet racks mounted on motorized bases moving on floor rails to collapse unused aisles.
View Mobile Racking
Low-temperature resistant automated pallet runners operable down to -25°C for refrigerated warehouses.
View Cold Shuttle SystemsIn modern intra-logistics, structural stability, cubic space utilization, and integration with automated material handling equipment (MHE) dictate operational profitability. As a premier China Sa Shelving And Storage Equipments Manufacturer & Factory, Guake Logistics Technology (Shandong) Co., Ltd. delivers engineered racking systems designed to withstand demanding dynamic and static stress loads across global supply chain hubs.
Our manufacturing matrix utilizes certified high-tensile cold-rolled steel profiles (Q235B and Q355B grades), precision-punched on automated continuous roll-forming production lines. By applying Finite Element Analysis (FEA) to every structural column, cross-beam, and row spacer, our engineering division guarantees load compliance with international standards including FEM 10.2.02 (European Federation of Materials Handling), ANSI/RMI MH16.1 (Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks), and AS4084-2012 (Australian Standard for Steel Storage Racking).
Standard commercial storage shelves often fail under sustained cyclic loading due to micro-fractures in low-grade steel or deficient beam-to-column connector welds. Guake's industrial-grade Sa Shelving platforms employ 5-hook cold-formed beam connectors with dynamic safety lock pins, engineered to maintain a structural safety margin of 1.95:1 above nominal load ratings, even under seismic dynamic forces compliant with Zone 4 acceleration factors.
Leveraging Shandong’s heavy industrial steel supply chain to deliver cost efficiencies, raw material quality control, and rapid global export capabilities.
Situated in Shandong province, our factory directly procures hot-rolled steel coils from tier-1 state mills (BaoSteel, Shougang). Direct mill access guarantees strict material chemical composition, batch traceability, and protection against steel price volatility.
Our 20,000+ m² production center operates automated continuous cold-roll forming lines, robotized MIG welding stations, and an automatic electrostatic epoxy-polyester powder coating line, ensuring flawless surface finishes resistant to corrosion and mechanical impact.
Proximity to Qingdao and Tianjin deep-water seaports reduces domestic inland freight expenses. Our specialized packing team utilizes custom steel skids and protective bundling to maximize sea container volume utilization while eliminating transit damage.
How Guake bridges international procurement gaps through precise structural design, BIM integration, and localized technical compliance.
Global warehouse operators must evaluate storage systems beyond initial procurement price. Our engineering team designs modular Sa Shelving layouts that allow dynamic vertical shelf adjustment (in 50mm or 75mm increments) and low friction radio shuttle components, reducing long-term maintenance overhead by up to 35%.
We provide full Building Information Modeling (BIM) files and 3D CAD layout schemes compatible with Revit and AutoCAD. Global logistics planners can embed our digital twin racking models directly into facility architectural plans to analyze forklift turning radiuses, fire sprinkler clearance, and floor slab point loading.
For operations located in active seismic zones (e.g., Pacific Rim, Latin America, Southeast Asia), standard racking designs pose collapse risks. Guake customized upright frames utilize heavy-gauge floor anchor plates, structural back bracing, and high-tensile anchor bolts calculated specifically for local PGA (Peak Ground Acceleration) values.
Our automated shuttle racking equipment and automated mobile storage systems feature open API protocols and PLC control platforms (Siemens/Schneider) that interface directly with enterprise Warehouse Management Systems (WMS) and Warehouse Control Systems (WCS).
Select the optimal racking architecture based on pallet selectivity, storage density, and operational throughput.
| Storage System Type | Cubic Density | Pallet Access (Selectivity) | Inventory Flow | Max Load per Level | Primary Industrial Application |
|---|---|---|---|---|---|
| Radio Shuttle Racking | Very High (85%+) | Lane Dependent | FIFO or LIFO | 1,500 kg / pallet | Cold Storage, Food & Beverage, FMCG Bulk |
| Selective Pallet Racks | Standard (40-50%) | 100% Direct | FIFO | 4,500 kg / level | General Logistics, E-Commerce Hubs, 3PL |
| Steel Mezzanine Platform | Space Doubling | 100% Floor Access | Continuous | 1,000 kg / m² | Parts Picking, Light Manufacturing, Offices |
| Drive-In Racking | High (65-75%) | Low (Per Lane) | LIFO | 1,200 kg / pallet | Seasonal Stock, Homogeneous Materials |
| Push Back Racking | High (60-70%) | Lane Face Access | LIFO | 1,400 kg / cart | Medium SKU Volume, Cold Storage |
| Automated Mobile Racking | Very High (80%+) | 100% (Single Aisle) | FIFO / LIFO | 24,000 kg / mobile base | Pharmaceuticals, High-Value Cold Stores |
| Cantilever Racking | Variable | 100% Side Access | Flexible | 3,000 kg / arm | Pipes, Steel Bars, Timber, Sheet Materials |
Key technological shifts reshaping modern industrial shelving, high-bay automated storage, and material handling infrastructure.
Traditional static storage is transitioning into robotic-compatible shelving systems. Upright frames and lower beam decks are now customized with optical alignment reflectors, floor magnetic tracks, and wide-span aisle clearances designed specifically for Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs).
Smart warehouses are installing wireless strain gauge sensors and impact detectors on perimeter rack columns. These IoT devices monitor structural stress in real-time, sending immediate safety alerts to facility managers if a forklift collision compromises column verticality beyond allowable FEM tolerances.
ESG compliance requires carbon footprint reductions across warehouse hardware. Guake utilizes 100% heavy-metal-free thermosetting powder coatings with zero Volatile Organic Compound (VOC) emissions, combined with energy-efficient curing ovens powered by clean natural gas technology.
Tailor-made industrial racking configurations engineered for specialized sectoral supply chains.
Refrigerated warehouse facilities incur massive thermal energy expenses, requiring maximum cubic pallet storage per square meter of refrigerated space. Guake's Radio Shuttle Racking Systems engineered with cold-resistant steel fasteners and lithium-iron-phosphate shuttle batteries allow high-density deep-lane storage operating continuously at -25°C, reducing refrigeration energy overhead per pallet by up to 40%.
Rapid SKU turnover and intensive manual piece picking demand multi-level accessibility. Our Rack-Supported Mezzanines and Boltless Medium-Duty Shelving incorporate integrated staircases, safety drop gates, mesh decking, and chute systems. E-commerce fulfillment operators achieve up to 300% expanded picking face availability within the same warehouse footprint.
Heavy machinery components, metal stamping dies, and engine blocks require extreme load stability. Guake's custom Heavy-Duty Selective Pallet Racking utilizes heavy-gauge upright profiles (120mm x 95mm section) with double-C welded box beams, accommodating up to 4,500 kg per beam level while providing 100% direct crane or forklift access.
Pharmaceutical distribution hubs require strict hygiene, zero particulate shedding, and smooth cleanable surfaces. We manufacture custom galvanized or stainless-steel wire mesh decking and powder-coated shelving with non-porous antimicrobial surface finishes, ensuring full compliance with GMP and FDA storage cleanliness standards.
Expert answers regarding structural engineering, customized manufacturing, international delivery, and installation safety.
Guake Logistics Technology manufactures a complete portfolio of warehouse storage equipment and industrial shelving systems, including:
Every racking system engineered by Guake undergoes rigorous structural calculation using Finite Element Analysis (FEA) software in accordance with ANSI/RMI MH16.1 and FEM 10.2.02 codes. We analyze static dead loads, dynamic live loads (forklift placing force), wind shear (for open-sided structures), and seismic horizontal accelerations. Standard designs incorporate a structural safety factor of 1.95:1 based on the minimum yield strength ($f_y$) of our certified Q235B/Q355B cold-rolled steel.
Yes. 100% of our production is engineered to order based on client architectural drawings. When you submit your floor plan (CAD or PDF), our engineering team calculates:
For international projects, Guake provides comprehensive technical support packages:
Guake offers multi-stage surface preparation and coating options tailored to your facility's environmental conditions:
Standard manufacturing lead time for full container loads (20ft / 40ft HQ) ranges from 15 to 25 working days following final CAD drawing approval. Delivery time by sea from Qingdao/Tianjin ports to major destination harbors is typically:
Guake's specialized Cold-Chain Radio Shuttles feature low-temperature hydraulic fluids, electronic component heaters, and sealed anti-condensation control boxes. Powered by high-capacity Lithium Iron Phosphate ($LiFePO_4$) batteries with thermal jackets, our shuttles operate at peak efficiency down to -25°C with an continuous shift autonomy of 8 to 10 hours per battery charge.
Direct factory procurement eliminates middleman markup fees, giving you 20-40% cost savings while providing direct access to the structural engineering team that designs your system. Furthermore, you receive factory-original spare parts, complete raw material test certificates (MTC), and direct warranty coverage directly from the manufacturer.
Complete your facility layout with customized cantilever racks, boltless shelving units, and automated ASRS components.

Unobstructed arm racking engineered specifically for long profiles, tubing, timber bundles, and sheet goods.
View Special Racking
High capacity structural beam racking system supporting up to 4,500 kg per beam level for industrial pallets.
View Heavy-Duty Racks
Versatile boltless modular steel shelving for workshop tool storage, maintenance bays, and parts inventory.
View Metal Shelving
Flexible single or double-sided cantilever columns for lightweight extrusions, plastic pipes, and conduits.
View Cantilever Racks
Rapid snap-in assembly shelving units ideal for light manual order picking and archival box storage.
View Boltless Shelving
Heavy structural I-beam platform systems creating usable second-floor office space or assembly zones.
Explore Steel Platforms
Multi-tier manual shelving aisles designed for high-density bin picking in electronic parts warehouses.
View Multi-Layer Shelving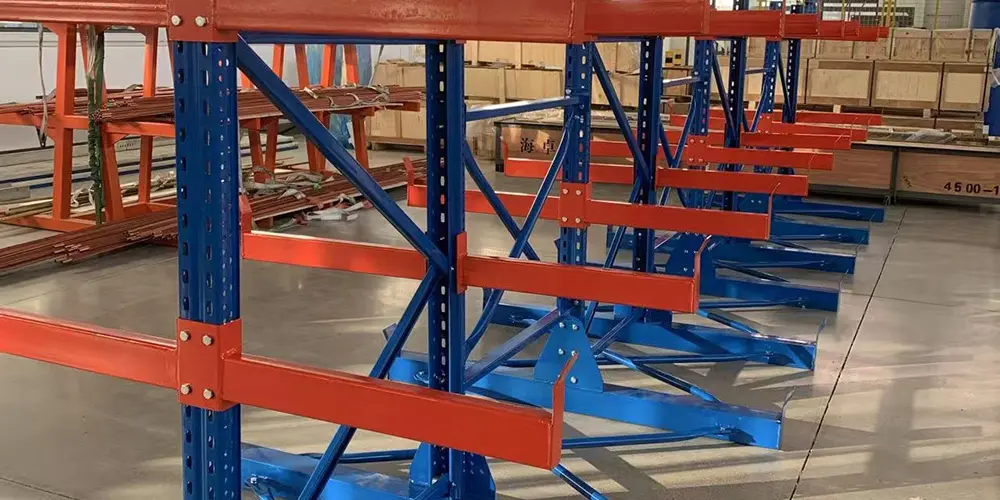
Extra heavy-duty column arms supporting up to 3,000 kg per arm for steel bar stock and heavy tubing.
View Heavy Cantilever