


Factory-direct industrial shelving, high-bay racking, and structural steel platforms precision-engineered to international FEM and RMI standards.








Evaluating structural steel standards, roll-forming engineering, and direct manufacturing advantages from Shandong's premier logistics infrastructure hub.
China's dominance in standard pallet rack manufacturing stems from unmatched metallurgy supply chains. At Guake Logistics Technology (Shandong) Co., Ltd., we utilize premium prime Q235B and high-yield Q355B structural steel coils (equivalent to ASTM A1011 SS Grade 36 and EN 10025 S355). Cold-roll formed with continuous 18-stage rolling profiles, our upright posts deliver superior buckling resistance, optimized section modulus, and precise hole-pitch tolerances matching worldwide teardrop and hex patterns.
Standard pallet racking must satisfy stringent structural criteria to prevent structural collapse under seismic or accidental forklift impact. Guake designs strictly conform to North American RMI (ANSI MH16.1), European FEM 10.2.02, and Australian AS4084-2012 structural specifications. Advanced Finite Element Analysis (FEA) software simulates extreme load combinations, live dynamic stresses, and beam deflection ratios restricted under L/200, guaranteeing structural safety for multi-tier operations up to 15 meters high.
Operating a modern 20,000 m² state-of-the-art manufacturing center in Linyi, Shandong, Guake seamlessly integrates raw steel coil slitting, automatic stamping, continuous roll-forming, robotic welding, and automated electrostatic powder coating. Purchasing direct from a established OEM/ODM China supplier eliminates intermediary markups, reduces project procurement lead times by up to 35%, and guarantees full traceability from mill test certificates to final container loading.
Deconstructing key purchasing triggers, Total Cost of Ownership (TCO) variables, and critical structural engineering constraints evaluated by global supply chain executives.
Industrial real estate costs have escalated globally by over 40% in key logistics hubs. Supply chain managers are compelled to transition from flat storage to vertical racking systems. Standard selective and teardrop pallet racks allow warehouses to utilize clear heights up to 12–15 meters, boosting volumetric storage density by up to 300% without expanding physical building footprints.
Sourcing heavy steel infrastructure internationally requires smart freight engineering. Guake's knock-down (KD) upright frame designs, nested step beam geometry, and customized wooden pallet packaging maximize freight density inside 40ft High Cube (40HQ) containers. This reduces ocean transport costs per pallet position to historical lows, offering substantial TCO savings for overseas buyers.
Procurement directors operating in active seismic zones (e.g., US West Coast, Japan, Latin America, Southeast Asia) mandate rigorous dynamic structural calculations. Guake structural engineers configure heavy-duty enlarged baseplates, double-anchor footings, high-tensile 8.8 grade anchor bolts, and specialized frame bracing geometries to withstand severe seismic accelerations without structural collapse.
Discover how precision automated manufacturing lines deliver standard pallet racking components with sub-millimeter tolerances and extreme structural durability.
Equipped with 18-pass automated cold roll-forming machines, Guake produces upright profiles with uniform wall thickness and zero internal stress concentration. Continuous automatic CNC punching guarantees precise 50mm, 75mm, or 76.2mm (3-inch) pitch hole centers for complete interchangeability.
Beam end-connectors (claw connectors) are welded to box beams and step beams using multi-axis ABB industrial welding robots. Shielded gas MIG welding eliminates weld porosity, guarantees deep penetration, and withstands extreme dynamic bending moments during heavy pallet placement.
Components undergo a 6-stage chemical pretreatment, including acid rust removal, phosphating, and pure water rinsing. Powder coating is applied via Swiss Gema electrostatic spray systems using thermosetting epoxy-polyester powder (60–80 micron film thickness) cured at 200°C for maximum scratch resistance.
Rigorous quality checkpoints test raw material chemical composition, tensile yield strength, weld ultrasonic integrity, powder adhesion (cross-hatch test), and dimensional alignment. Every shipment includes factory certification documents matching international procurement specs.
From freezing temperature environments to high-speed e-commerce fulfillment hubs, Guake standard and custom racking systems optimize operations worldwide.
Refrigerated warehouses face extreme operational costs per cubic meter. Guake supplies specialized low-temperature resistant steel standard pallet racks, hot-dip galvanized drive-in racks, and radio shuttle systems that maintain structural ductility down to -30°C without embrittlement, maximizing cold room volume utilization up to 85%.
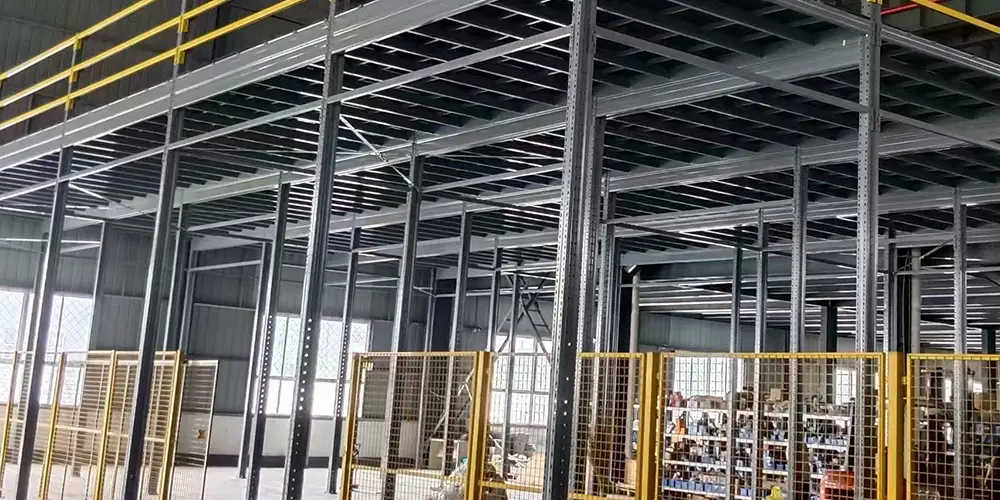
High-speed omni-channel fulfillment facilities require high SKU selectivity combined with multi-tier picking structures. Integrating standard selective pallet racking on lower levels with steel mezzanine picking platforms on upper floors enables rapid hand-picking of individual items alongside heavy bulk pallet replenishment.
Handling automotive stamping dies, engine blocks, and raw steel coils requires ultra-heavy beam capacities exceeding 4,000 kg per level. Guake manufactures heavy-duty structural steel beam racks with reinforced columns, heavy wire mesh decking, and impact-resistant column guards engineered for grueling factory environments.
Compare load capacities, operational throughput, pallet selectivity, and spatial footprint efficiency across primary heavy-duty warehouse racking types.
| Racking Architecture Type | Pallet Selectivity | Space Utilization | Forklift Operating Aisle | Typical Load Capacity | Ideal Inventory SKU Profile |
|---|---|---|---|---|---|
| Standard Selective Pallet Rack | 100% Immediate Access | 40% – 50% Volume | 3.0m – 3.8m (Standard) | 1,000kg – 4,500kg / Level | High SKU diversity, frequent picking, general distribution |
| Drive-In / Drive-Through Rack | LIFO / FIFO (Lane Level) | 65% – 75% Volume | Forklift enters rack lane | 1,000kg – 1,500kg / Pallet | Low SKU counts, bulk homogeneous goods, cold storage |
| Push Back Cart Racking | LIFO (2-6 Pallets Deep) | 60% – 70% Volume | 3.0m – 3.5m Aisle Face | 1,000kg – 1,500kg / Cart | Medium SKU counts, fast batch turns, front picking access |
| Automated Radio Shuttle Rack | FIFO or LIFO (Deep Lane) | 80% – 85% Volume | Aisle Face Only (Robot In Lane) | 1,500kg – 2,000kg / Shuttle | High-throughput, FMCG, food & beverage, cold chain |
| Motorized Mobile Racking | 100% (Single Moving Aisle) | 80% – 90% Volume | 1 Open Dynamic Aisle | 800kg – 2,000kg / Pallet | High real estate value, low-to-medium throughput |
| Multi-Tier Steel Mezzanine | 100% Floor Access | 200% – 300% Floor Area | Pedestrian / Hand Cart / Lift | 300kg – 1,000kg / SQM | E-commerce small parts, manual picking, floor expansion |
Providing full international engineering backing from initial CAD layout design to on-site assembly guidance and certified structural safety checks.
Before fabrication begins, Guake senior storage engineers prepare comprehensive CAD floor plan layouts, 3D structural renders, and full engineering stress calculation dossiers. We verify building slab floor capacity, clear height limitations, column spacing, and forklift turning radius specifications to guarantee seamless installation.
Guake projects include complete 3D assembly blueprints, component piece mark indexing, and step-by-step installation manuals. For large scale warehousing projects, we send certified structural assembly supervisors to site or provide complete remote video commissioning guidance to ensure racking structures are plumb, squared, and securely anchored.
Guake Logistics Technology operates under audited ISO 9001:2015 Quality Management Systems, ISO 14001:2015 Environmental Management, and ISO 45001:2018 Occupational Health & Safety. Our industrial steel racking components undergo independent load testing to ensure strict compliance with European CE standards and North American safety codes.
Clear, authoritative engineering answers to common technical queries raised by global logistics directors, procurement buyers, and structural consultants.
Explore our full line of industrial heavy-duty pallet racks, cantilever long-goods shelving, and multi-tier structural solutions.







Partner directly with Guake Logistics Technology (Shandong) Co., Ltd. for factory-direct prices, certified structural load calculations, and global site delivery support.
