Engineered to order with certified Q235B/Q355B structural steel. Select your operational configuration below to explore system specifications and structural load profiles.








An exhaustive analysis of industrial real estate dynamics, cold-formed structural steel supply chains, and China's role as the world's primary upright racking manufacturing hub.
Global warehouse operators face unprecedented pressures driven by escalating land acquisition costs and rising industrial leases across major logistics hubs in North America, Europe, and Asia-Pacific. As horizontal expansion becomes financially unviable, supply chain architects are forced to maximize vertical volumetric storage density. The industrial upright column frame forms the foundational load-bearing skeleton of modern high-bay storage, dictating structural integrity up to 40-meter vertical heights.
China has established unmatched global supremacy in cold-formed structural steel fabrication. Concentrated in industrial clusters like Shandong Province, Chinese manufacturers leverage integrated steel mill supply chains, automated continuous roll-forming technology, and advanced electrostatic powder coating lines. This enables suppliers like Guake Logistics Technology to deliver structural steel racking systems engineered to international standards at a cost-per-pallet position that cannot be matched by regional fabricators.
Post-pandemic global trade networks demand adaptable, modular warehousing infrastructure. Procurement teams no longer purchase generic off-the-shelf shelving; they require customized upright frame profiles engineered with specific moment-resisting beam connections, seismic baseplate anchors, and anti-corrosive surface treatments capable of withstanding aggressive industrial environments, high throughput frequencies, and sub-zero cold storage conditions.
Deep technical parameters defining vertical load capacity, torsional stiffness, cold-roll forming precision, and European/American structural compliance.
An industrial warehouse upright frame consists of two cold-rolled vertical columns joined by continuous horizontal and diagonal bracing members using high-tensile structural bolts. The cross-sectional geometry of the vertical column (typically an Omega Profile or modified C-profile with stiffening return flanges) determines the frame's resistance to Euler axial buckling, torsional distortion, and impact fatigue.
The structural reliability of an upright frame starts with raw steel chemical composition. Standard light-to-medium systems utilize Q235B carbon steel (yield strength fy ≥ 235 MPa). For heavy-duty pallet racking, high-bay automated AS/RS structures, and seismic zones, Guake specifies high-strength cold-rolled Q355B low-alloy structural steel (yield strength fy ≥ 355 MPa, tensile strength up to 630 MPa). This high strength-to-weight ratio minimizes dead loads while providing elevated resistance to permanent plastic deformation under full rated capacity.
Upright columns are manufactured using continuous multi-stage automatic roll-forming mills with up to 24 rolling passes. Continuous CNC punching creates precise perforation patterns along the front column face. Guake manufactures standard industry pitch configurations including 50mm, 75mm, and 76.2mm (3-inch) pitch intervals, alongside teardrop hook styles for North American compatibility. Precision punching tolerance (±0.1mm) guarantees tight mechanical engagement between upright teardrop slots and beam connector claws, eliminating structural play.
Every custom upright assembly undergoes Finite Element Analysis (FEA) computer simulation to evaluate stress distribution, flexural deflection (limited strictly to L/200 under static load), and dynamic lateral stability during forklift docking or seismic excitation. All structural calculations manufactured in our Shandong plant conform rigorously to FEM 10.2.02 (European Federation of Materials Handling), EN 15512, and RMI (ANSI MH16.1) specifications.
Selecting the optimal warehouse upright configuration based on SKU diversity, pallet turnover velocity, floor load capacity, and labor automation requirements.
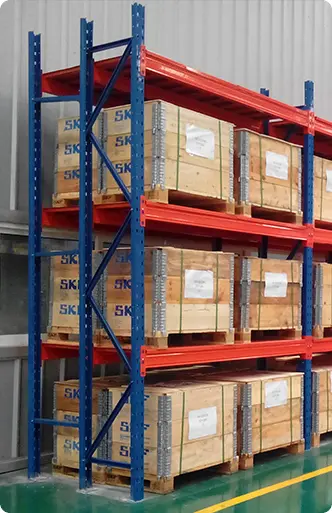
The standard benchmark for logistics operations requiring 100% immediate pallet selectivity. Constructed from vertical upright frames and horizontal box beams with safety locking pins. Ideal for multi-SKU distribution centers where direct access to every pallet position is mandatory.
Designed for ultra-high-density storage of homogeneous goods. Forklifts physically drive into structural racking lanes to place pallets on continuous heavy-duty side support rails. Removes working aisles, increasing volume utilization by up to 85%.
Utilizes nested telescoping carts riding on inclined structural steel rails. When a pallet is loaded from the aisle face, it pushes the behind pallet deeper into the rack lane. Offers high storage density (2 to 6 pallets deep per lane) combined with faster handling speed than drive-in racking.
Semi-automated deep-lane storage system utilizing an autonomous, battery-powered pallet runner controlled remotely by the forklift operator. The radio shuttle transports pallets along specially designed upright runner profiles inside deep channels, dramatically reducing loading cycle times.
Heavy-duty selective racking mounted on electrically driven mobile bases that travel along recessed floor tracks. Rows shift lateral to open only one single working aisle when commanded, doubling warehouse pallet storage capacity within the identical floor footprint.
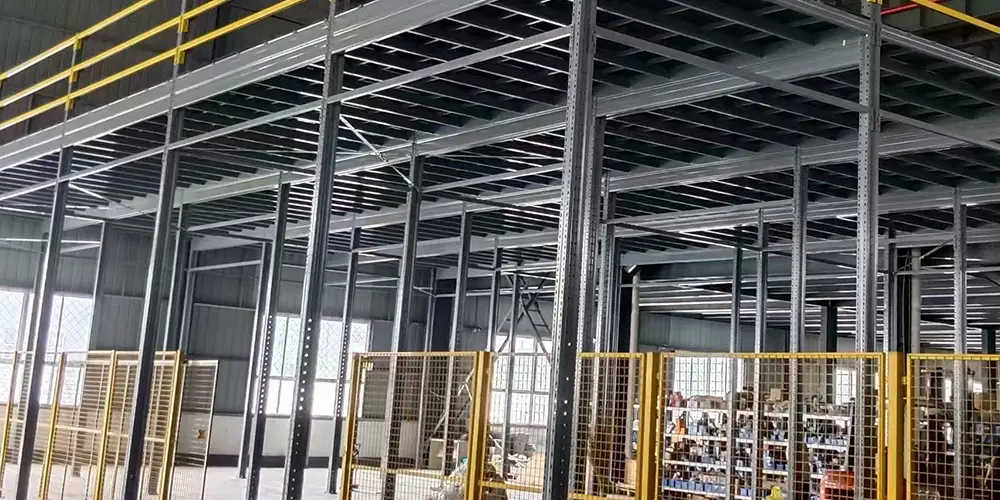
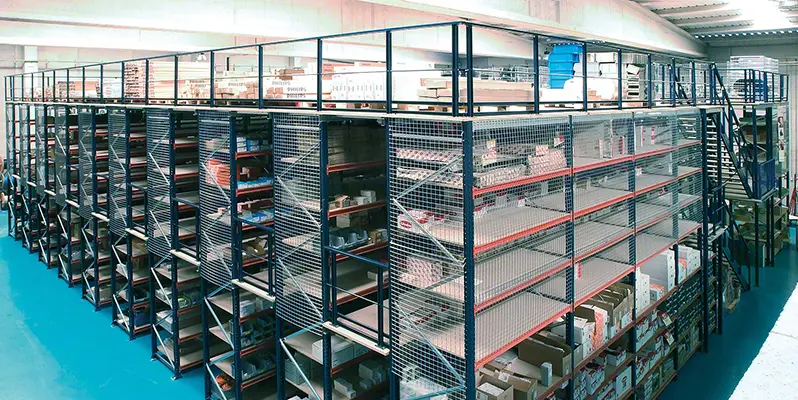
Engineered structural steel platforms and rack-supported mezzanines that transform unused vertical headroom into operational floor space. Multi-level picking walkways allow simultaneous order fulfillment, parts storage, and administrative office integration.
Examining the technological shift toward AS/RS automation, cold-chain surface engineering, structural health IoT sensors, and green manufacturing practices.
The boundary between static upright frames and robotic automation is disappearing. Next-generation warehouses deploy Automated Storage and Retrieval Systems (AS/RS) where ultra-precise clad-rack upright structures serve as both the building's structural support framing and the guidance tracks for high-speed stacker cranes reaching heights up to 40 meters. Tolerances for column verticality, beam straightness, and floor anchor deflection are engineered down to millimeter precision.
Pharmaceutical cold storage and frozen food fulfillment centers operating at -25°C to -30°C present severe engineering challenges including steel hydrogen embrittlement and coating delamination. Guake utilizes fine-grain structural steel with guaranteed Charpy V-notch impact toughness test ratings at low temperatures, combined with thermosetting epoxy-polyester powder coatings engineered to resist micro-cracking during extreme thermal cycles.
Accidental impact by heavy material handling equipment poses severe safety risks to upright column integrity. The future upright frame incorporates IoT-enabled wireless strain gauges and tri-axial accelerometer sensors embedded directly within the lower column profile. These smart sensors transmit real-time alerts to warehouse management systems (WMS) when an upright experiences localized impact energy exceeding safety thresholds, enabling proactive maintenance prior to structural collapse.
Sustainability is now a core requirement for international procurement. Guake's Shandong manufacturing facility utilizes automated 7-stage eco-friendly chemical pre-treatment cleaning systems free of toxic heavy metals, followed by zero-VOC electrostatic powder recovery booths. Combined with high-efficiency roll-forming machinery powered by solar-supplemented energy grids, total carbon emissions per metric ton of processed steel are reduced significantly.
Tailored vertical upright frame configurations optimized for diverse operational environments, compliance standards, and picking throughput requirements.
E-commerce operations handle high SKU variability, rapid order cycle times, and heavy pedestrian picking activity. Deployments combine heavy-duty selective rack bases supporting multi-tiered steel structure mezzanines overhead. Column uprights are retrofitted with continuous steel frame guards, floor-anchored corner protectors, and mesh shelf dividers to protect operators and prevent item fall-through during high-frequency picking.
Refrigerated and frozen food operations face high energy costs per cubic meter. High-density Radio Shuttle racking and Motorized Mobile racking systems are the preferred architectures. Upright frames are engineered with hot-dip galvanized steel or specialized low-temperature powder coatings. Deep lane configurations maximize thermal efficiency by removing air voids between pallets.
Heavy machinery, stamping dies, engine blocks, and raw steel coils require extreme point-load capacities. Heavy-duty upright frames utilize thick-gauge Q355B profiles (up to 3.0mm structural wall thickness) with heavy welded baseplates anchored via chemical epoxy bolts to withstand dynamic shock loading from overhead cranes and heavy-capacity forklift loading.
Medical supply and pharmaceutical facilities mandate stringent hygiene standards, non-dusting surfaces, and seamless inventory tracing. Racking systems feature smooth, non-porous powder-coated upright surfaces with rounded frame edges, wire mesh decking for unimpeded sprinkler fire suppression flow, and strict compliance with FDA/GMP cleanroom storage guidelines.
Standard technical engineering parameters across primary industrial warehouse upright configurations manufactured by Guake Logistics Technology.
| Racking System Type | Upright Column Profiles | Steel Material Grade | Max Frame Height | Max Load / Level | Surface Treatment | Design Compliance |
|---|---|---|---|---|---|---|
| Selective Pallet Racks | 80×60, 90×70, 100×70, 120×95 mm | Q235B / Q355B Cold-Rolled Steel | Up to 15.0 meters | 1,000 to 4,500 kg | Electrostatic Powder (80-120µ) | FEM 10.2.02 / RMI / EN 15512 |
| Drive-In Racking | 90×70, 100×70, 120×95 mm (Heavy Duty) | Q355B High-Tensile Steel | Up to 12.0 meters | 1,500 kg / pallet | Powder Coat / Hot-Dip Galvanized | ISO 9001 / CE / Structural FEA |
| Radio Shuttle Racking | 90×70, 100×70, 120×95 mm + Runner Rail | Q355B Low-Alloy Structural Steel | Up to 24.0 meters | 2,000 kg / pallet | Anti-Corrosive Epoxy Powder Coating | FEM 10.2.02 / EN 15512 |
| Motorized Mobile Racking | 100×70, 120×95 mm on Mobile Base | Q355B High-Yield Steel | Up to 12.0 meters | Up to 24,000 kg / Bay | Thermosetting Powder Coat | CE / EN 15512 / Dynamic Load Rated |
| Mezzanine Steel Platform | H-Beam Columns (150×150 to 300×300) | Q235B / Q355B Structural I-Beams | 2 to 4 Decking Tiers | 300 to 1,500 kg/m² | Industrial Anti-Rust Primer + Topcoat | GB 50017 / Structural Steel Building Code |
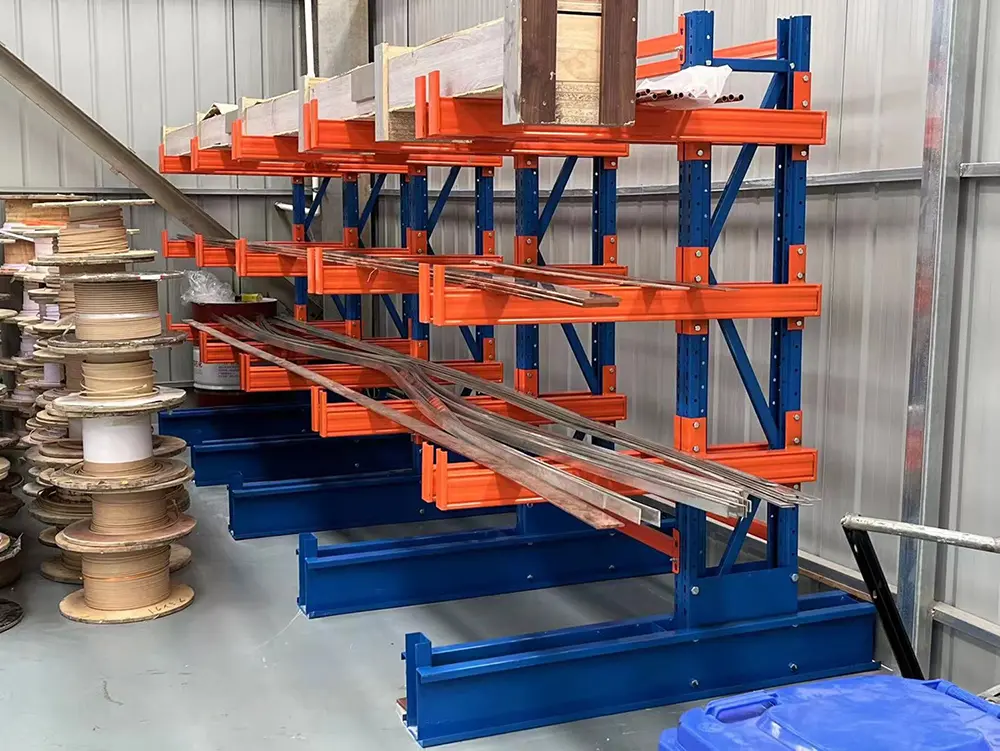
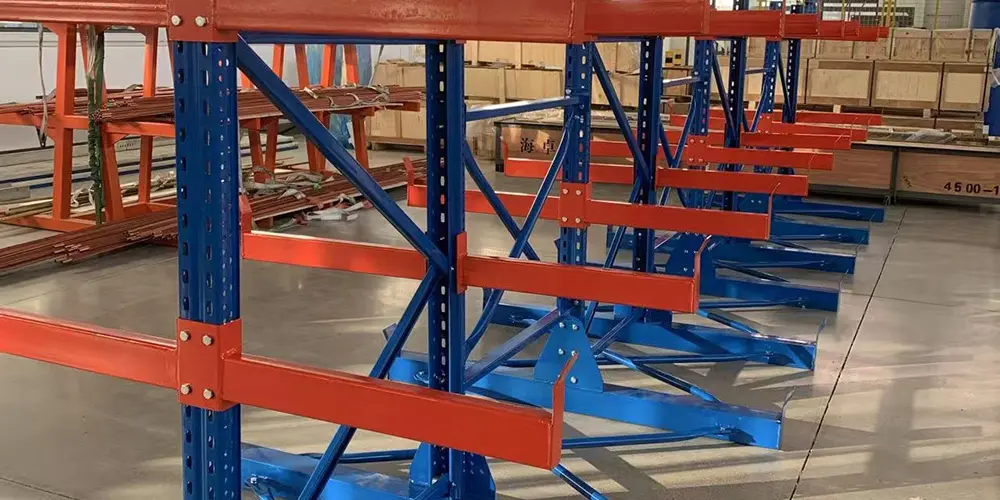
| Cantilever Racking | 200×100, 250×90, 300×90 C-Profile / Column | Q235B / Q355B Heavy Section Steel | Up to 9.0 meters | 500 to 2,000 kg / Arm | Outdoor UV-Resistant Powder / Galvanized | RMI / FEM Structural Guidelines |
Your trusted manufacturing single-source partner for precision storage racking, engineering layout design, structural calculation, and global turnkey installation.
Established in 2010 in Linyi City, Shandong Province, China, Guake Logistics Technology operates over 20,000 square meters of modern production facilities. Our manufacturing lines include continuous automated cold-roll forming machines, automatic steel tube slitting lines, high-precision laser cutting centers, robotic welding cells, and continuous electrostatic powder coating lines capable of processing thousands of metric tons of structural steel monthly.
We do not simply supply steel profiles. Guake provides an integrated project delivery model encompassing initial warehouse floor plan CAD layout design, volumetric spatial analysis, 3D structural Finite Element Analysis (FEA), structural steel fabrication, export packaging, global shipping logistics, remote installation guidance, and on-site commissioning.
Browse our comprehensive lineup of industrial cantilever racking, medium-duty shelving units, boltless systems, and structural platforms.







Direct, practical answers from our senior structural engineers regarding upright frame design, load certification, customization options, and global project execution.
To prepare an accurate structural layout proposal with matching load calculations, our engineering team requires:
Q235B is standard carbon steel with a minimum yield strength of 235 MPa, perfectly suited for standard beam levels and light-to-medium duty shelving. For high-bay upright frames, heavy pallet load capacities (>1,500 kg/level), dynamic Radio Shuttle storage, and seismic structural requirements, Guake uses Q355B low-alloy structural steel (yield strength ≥ 355 MPa). Using Q355B allows us to increase vertical load-bearing capacity by up to 30% while optimizing column steel wall thickness.
All structural designs, moment connections, bracing calculations, and safety margins manufactured by Guake comply with primary international logistics equipment standards including:
The choice depends on SKU turnover velocity, selectivity requirements, and forklift labor costs:
Yes. Every international project delivered by Guake includes comprehensive structural assembly blueprints, detailed 3D component installation diagrams, and complete hardware packing lists. For major commercial projects, we provide remote video installation support or deploy senior field engineers directly to overseas sites to supervise installation teams and conduct safety load inspections before commissioning.
Guake employs an advanced 7-stage chemical pre-treatment process (including automatic degreasing, zinc phosphating, and deionized water rinsing) prior to electrostatic powder application. Uprights are coated with 80-120 micron thermosetting epoxy-polyester powder and baked at 200°C. This creates a hard, impact-resistant finish with high resistance to salt spray, moisture corrosion, scratching, and industrial chemicals. Hot-dip galvanizing is also available for extreme outdoor or corrosive environments.
Yes. Because we control complete roll-forming and CNC punching lines in Shandong, we offer 100% custom manufacturing. Upright column heights can be produced continuously up to 12 meters (and spliced for higher AS/RS applications). Perforation pitch options include standard 50mm, 75mm, and 76.2mm (3-inch teardrop), while powder coating colors can be matched to any custom RAL color palette specified by the buyer.
Safety is engineered into every component: beam-to-upright connectors feature automatic mechanical safety locks to prevent accidental dislodgement during forklift lifting; upright frame bases are secured with heavy floor anchor bolts sized for concrete slab thickness; and heavy-duty steel corner guards and column protectors are integrated at aisle intersections to absorb accidental vehicle impacts.
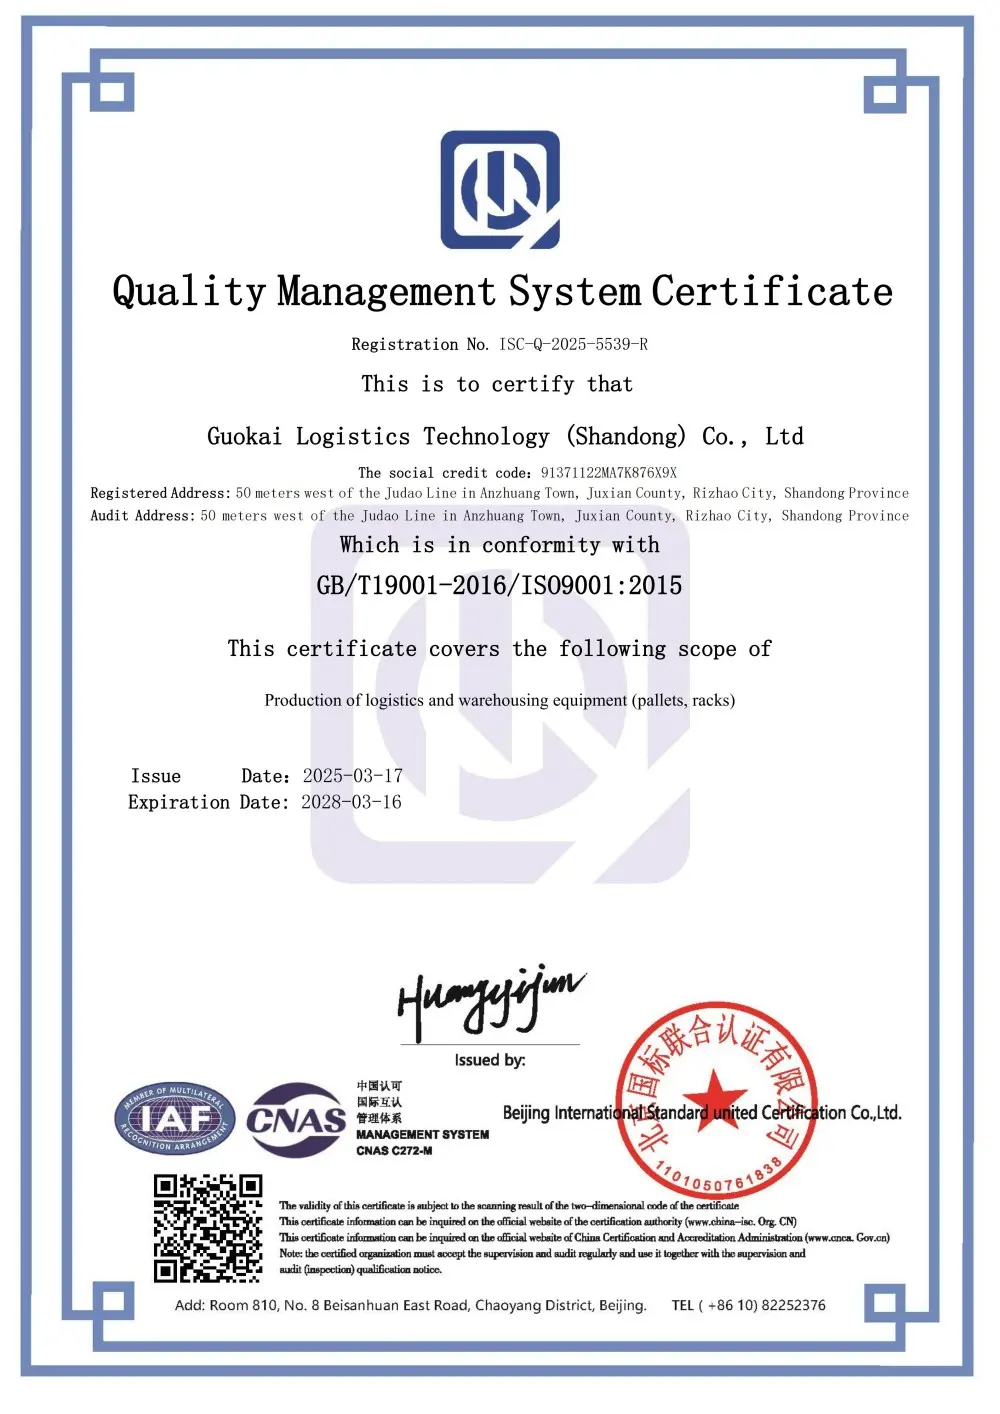
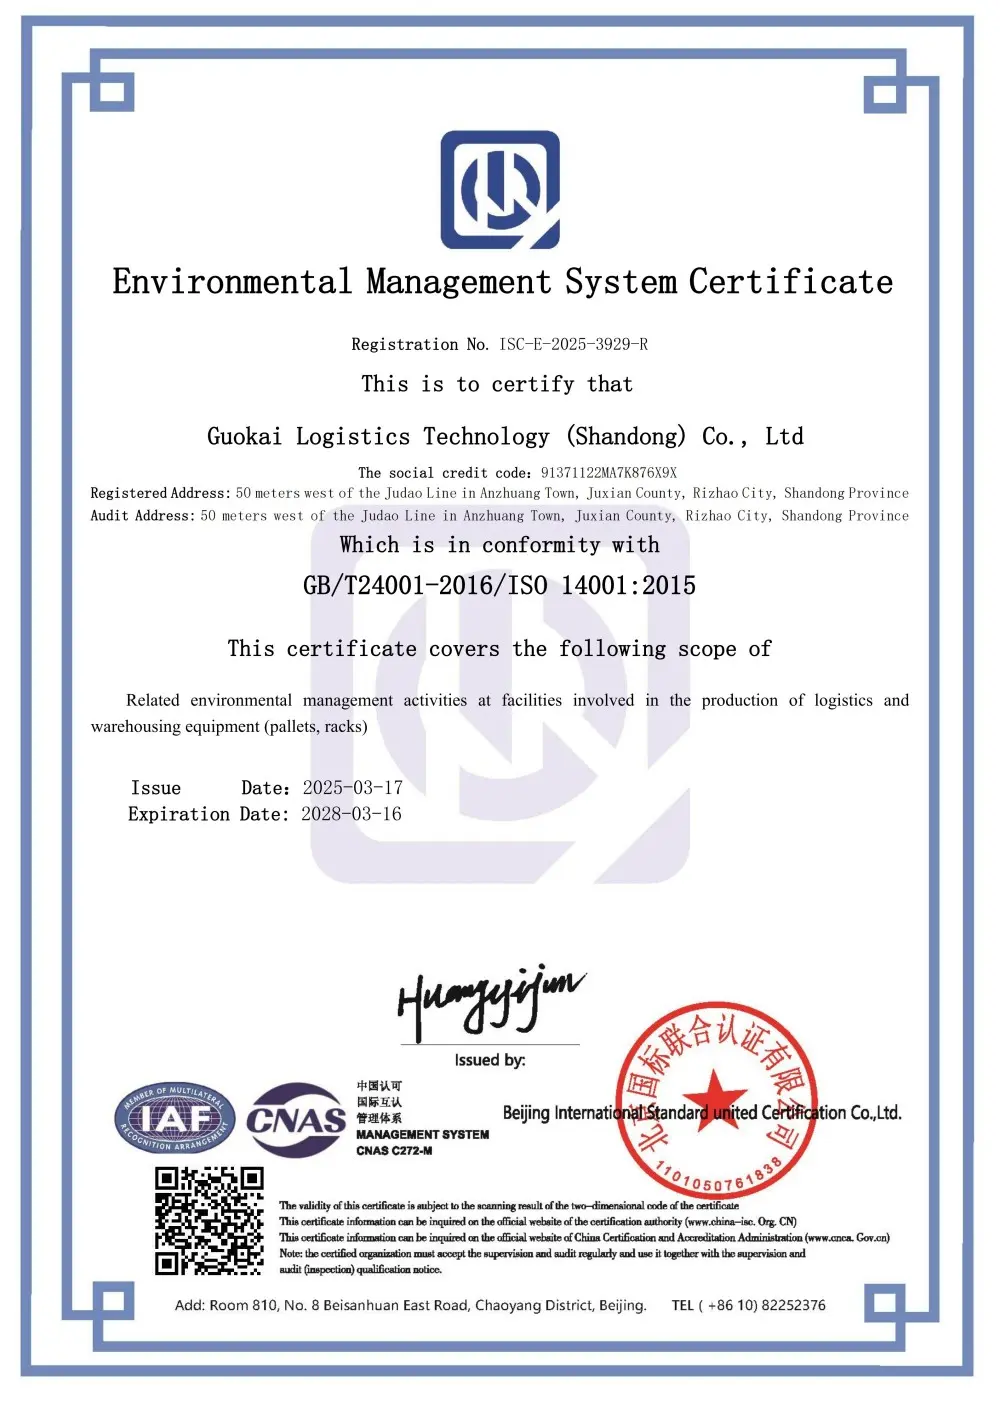
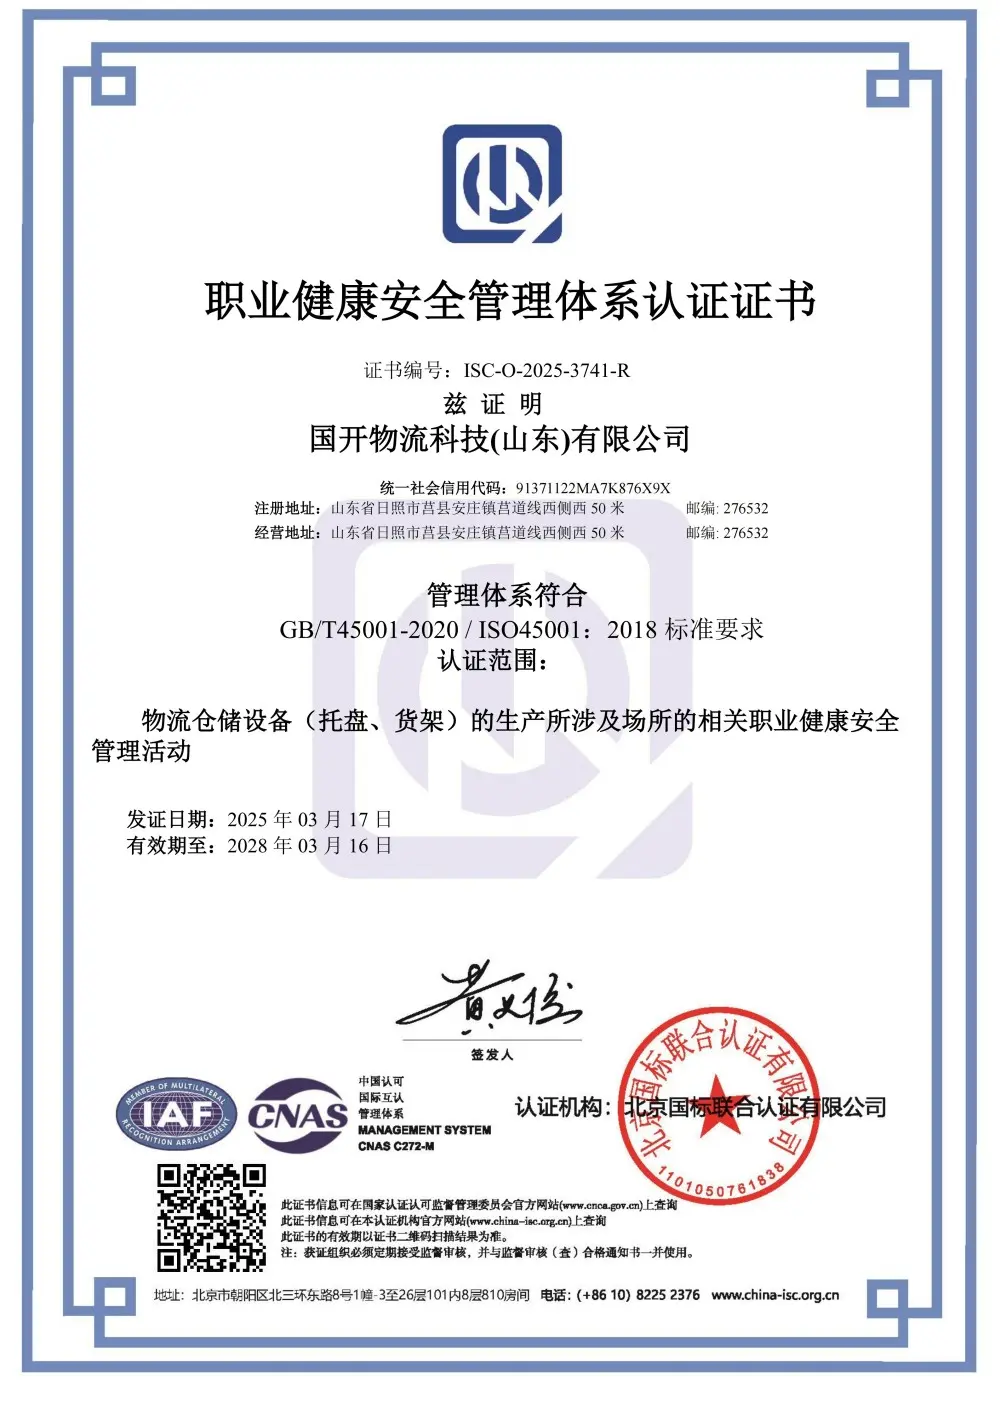
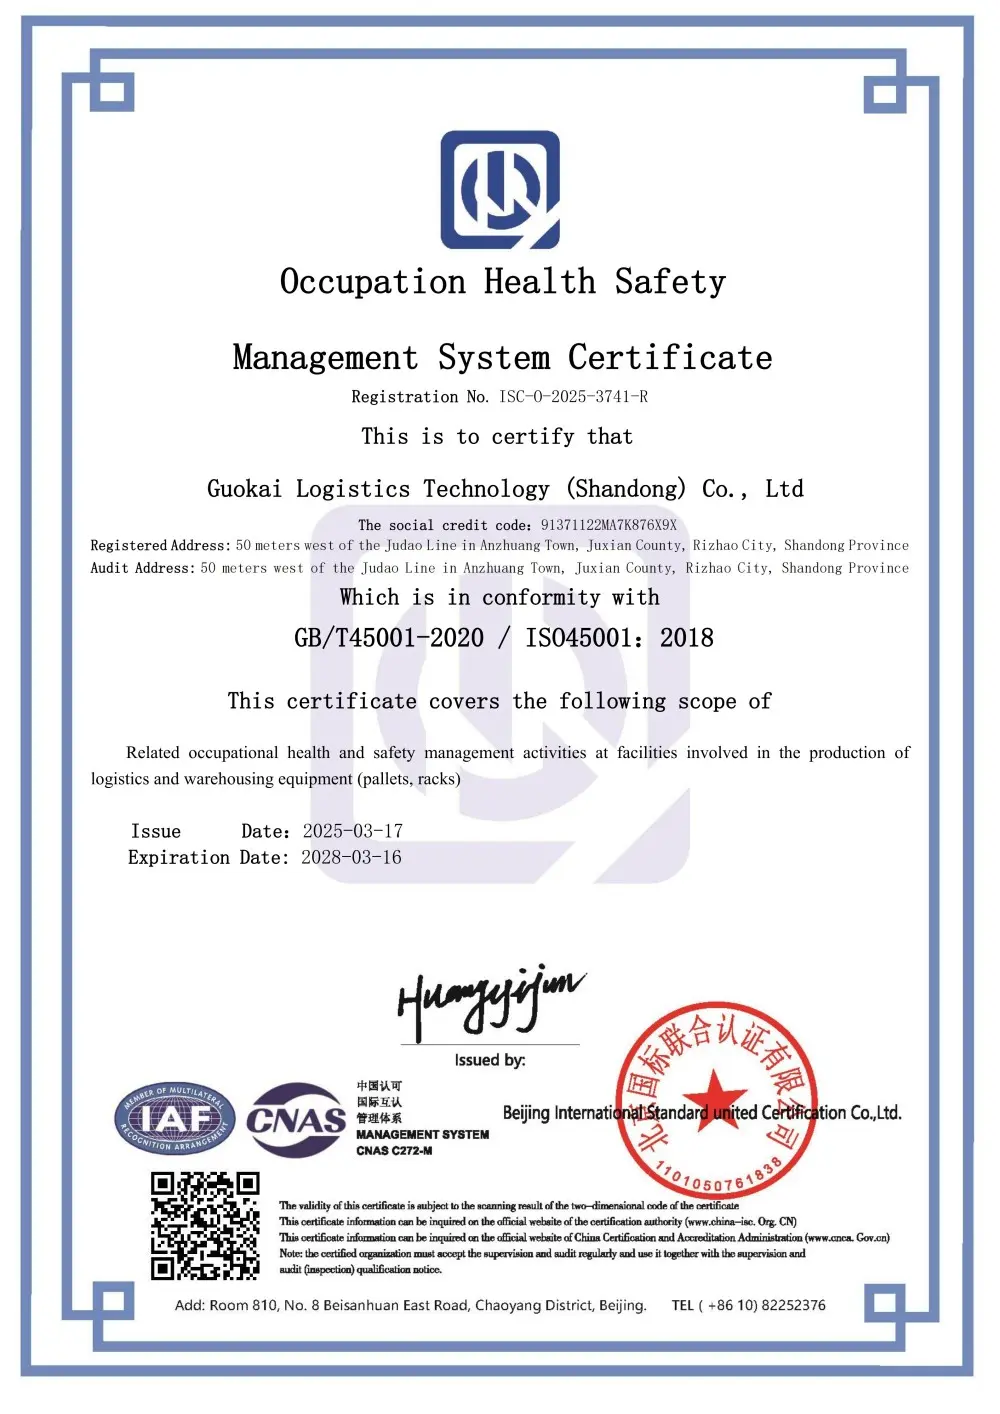
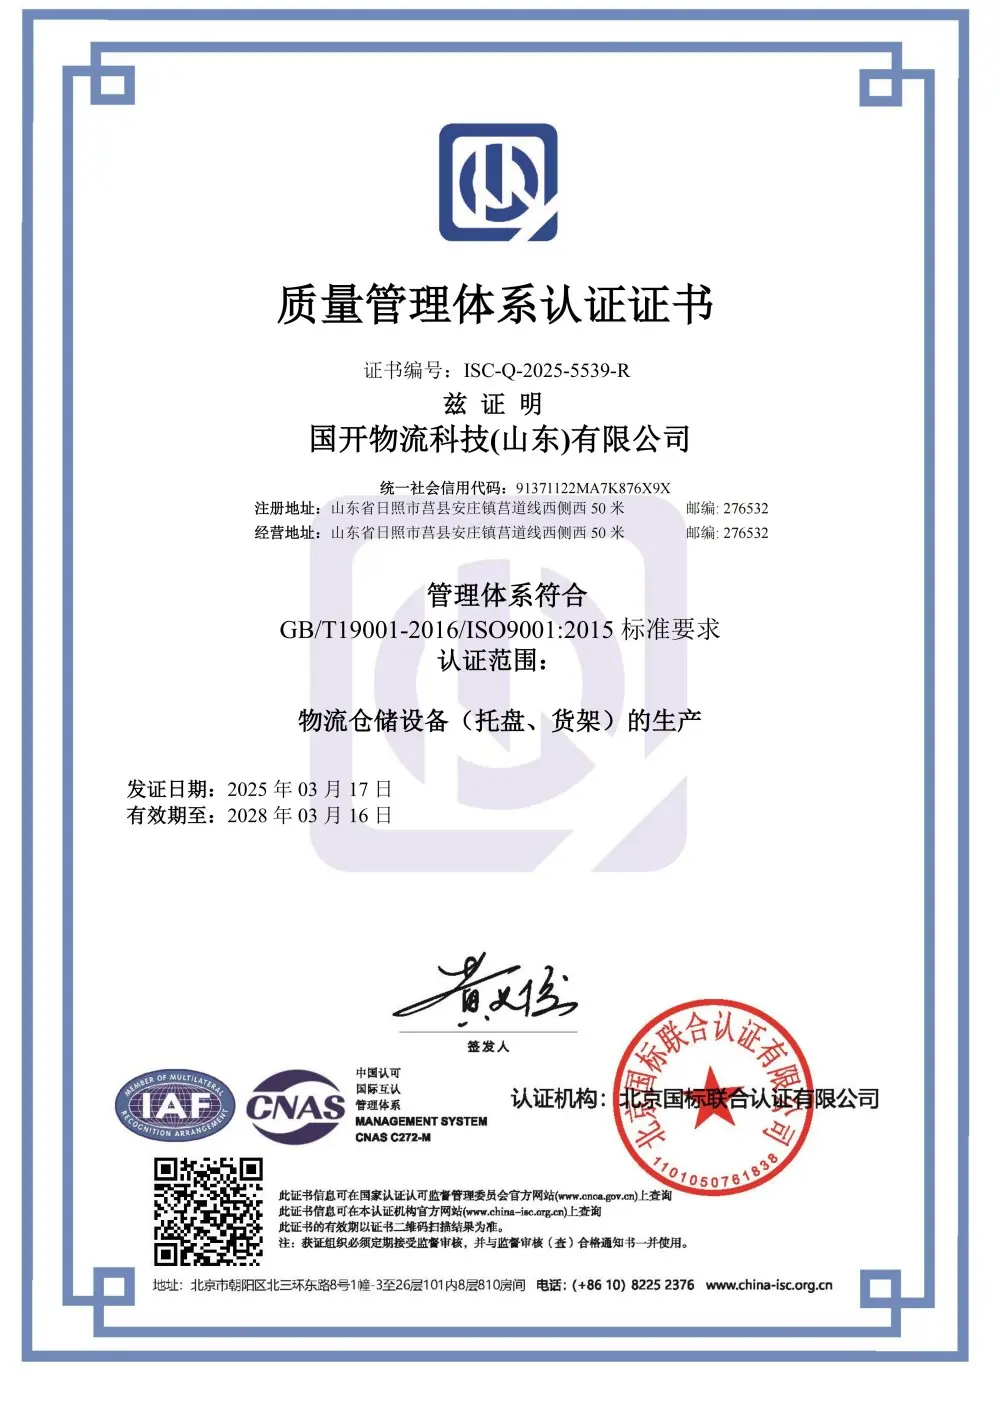
Independent quality certification and structural testing validate our commitment to safety, integrity, and long-term customer partnerships.
Technical guidance from our engineering team on spatial optimization, beam calculations, and cold storage design.
Share your warehouse floor plan, clear building height, and pallet load data with Guake Logistics Technology. Our structural engineers will generate a optimized 2D/3D layout proposal with certified structural calculations within 24 hours.