


Explore our flagship heavy-duty racking systems engineered by Guake Logistics Technology. Designed to maximize spatial volumetric efficiency, structural load capacity, and long-term operating safety.








As global supply chains realign towards omnichannel logistics, nearshoring hubs, and automated fulfillment centers, warehouse spatial optimization has evolved from a simple facility expense into a mission-critical strategic asset.
In modern industrial logistics, the physical footprint of industrial land continues to experience unprecedented valuation premiums. Facility managers worldwide face a mathematical dilemma: balancing 100% pallet selectivity against maximum cubic density utilization.
Traditional selective pallet racking provides instant access to every SKU but utilizes only 35% to 40% of available warehouse volume due to expansive forklift aisle requirements. Advanced heavy-duty engineered systems—such as Radio Shuttle, Drive-In, Push-Back, and Multi-Tier Mezzanine Platforms—allow enterprises to expand vertically and increase cubic utilization up to 85% without extending the building's physical perimeter.
Structural reliability in modern racking engineering relies on rigorous numerical calculation models. Engineering teams at Guake Logistics Technology utilize advanced Finite Element Analysis (FEA) to simulate complex stress distributions, dynamic fork-truck impacts, and seismic load accelerations (compliant with FEM 10.2.02 and ANSI MH16.1 specifications).
Through cold-formed structural steel modeling, optimized beam-to-upright lock connections, and precise sway bracing ratios, industrial rack design prevents catastrophical structural deflection, ensuring operational integrity across multi-decadal lifecycles.
Why leading global logistics operators, 3PL contractors, and industrial enterprises source heavy-duty warehouse racking directly from Shandong, China's premier steel engineering hub.
Guake Logistics Technology leverages direct supply agreements with premier Chinese steel manufacturing giants (such as SHAGANG and HBIS). We utilize premium-grade cold-rolled coils including Q235B and high-yield Q355B structural steel.
This guarantees standardized yield strength, consistent elastic modulus, and superior ductility, preventing material fatigue under high ambient load pressures.
Our Shandong manufacturing facilities operate continuous 18-stage automated cold roll-forming production lines equipped with real-time laser gauging. Upright profiles receive precise multi-pitch punching for maximum adaptability.
Robotic welding cells execute continuous automatic seam welding for beam connectors, eliminating human margin-of-error and structural void defects.
Surface finishing is performed via fully automated pre-treatment cleaning, phosphating, and electrostatic epoxy powder coating lines (film thickness regulated between 60 to 90 microns).
This provides exceptional resistance against impact scratching, chemical abrasion, and humidity-induced corrosion—essential for harsh industrial and cold-chain environments.
Detailed technical breakdown of industrial warehouse racking structures engineered by Chinese OEM supplier Guake Logistics Technology.
Designed for operations managing high volumes of homogeneous SKUs, Drive-In racking eliminates traditional work aisles by allowing counterbalanced forklifts to drive directly into deep storage channels. Pallets rest on continuous cold-formed cantilevered side rails.
Push-Back systems utilize nested dynamic carts rolling on inclined structural steel channels. When a new pallet is loaded by forklift from the front aisle face, it gently pushes the preceding pallet back into the lane face up to 2 to 6 pallets deep.
A semi-automated high-density storage solution incorporating an independent battery-powered Radio Shuttle vehicle that travels along tracks inside storage channels to place and retrieve pallets autonomously via wireless remote command.
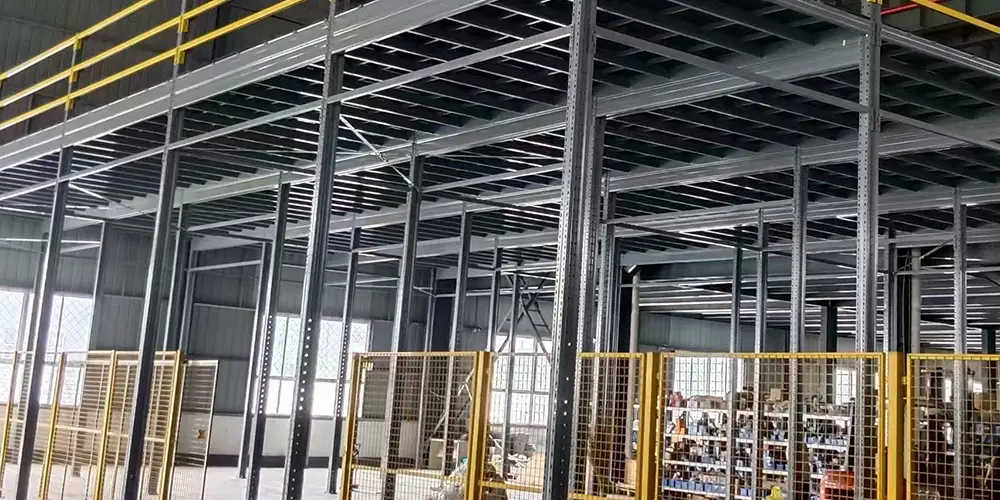
Engineered vertical space expansion structures utilizing heavy-duty rolled H-beams, cold-formed floor joists, and modular decking (steel diamond plate, bar grating, or high-density timber). Multi-tier mezzanines transform unused vertical height into productive floors.
| Racking System Type | Storage Density | Pallet Selectivity | Operating Method | Typical SKU Volume | Cold Storage Suitability |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (35-40%) | 100% Immediate | Forklift Truck | High SKU Variety | Good |
| Drive-In Racking | Very High (70-80%) | Low (Per Channel) | Forklift Drives Inside | Low SKU / High Bulk | Excellent |
| Push-Back Cart Racking | High (60-70%) | Moderate (Lane Face) | Gravity Nested Carts | Medium SKU Variety | Very Good |
| Radio Shuttle Racking | Ultra-High (80-85%) | Automated Channel | Robotic Shuttle + Forklift | High Volume Batches | Outstanding (-30°C) |
| Steel Structure Mezzanine | Vertical Doubling | 100% Floor Access | Manual / Pallet Jack / AGV | Parts Picking / E-Com | Standard |
Guake Logistics Technology customizes racking layouts to match specific operational profiles, floor slab loading limits, and handling equipment across diverse commercial sectors.
Freezer facilities (-25°C to -30°C) represent extreme real-estate operating expenses. Installing high-density Radio Shuttle racking or Mobile motorized racking minimizes wasted cubic cold space, drastically reduces thermal energy dissipation, and lowers electrical refrigeration bills.
High-turnover distribution centers utilize multi-tier mezzanine steel platforms configured with carton-flow tracks and integrated conveyor loops. Pickers fulfill thousands of individual parcel SKUs simultaneously across multi-level walkway floor plates.
Automotive OEMs and heavy equipment distributors require customized cantilever racking and heavy-duty pallet racks equipped with wire mesh decking or steel support bars to hold irregular, concentrated payload weights up to 4,000 kg per level.
How smart logistics automation, IoT telemetry, green structural steel production, and robotic integration are redefining global warehouse rack engineering.
Modern rack design is morphing into structural skeletons for fully Automated Storage and Retrieval Systems (ASRS). Structural rack uprights are manufactured with sub-millimeter tolerances to accommodate high-speed crane stackers, shuttle buses, and Autonomous Mobile Robots (AMRs).
Future-ready industrial racks incorporate IoT strain gauge sensors embedded inside critical upright bases. These digital sensors broadcast real-time telemetry to facility managers, instantly alerting operations if an accidental forklift strike exceeds safety impact thresholds.
Global enterprises demand lower Scope 3 embodied carbon footprints. Chinese rack factories, including Guake Logistics Technology, are adopting zero-emission powder coating processes, closed-loop water recycled phosphating, and certified low-carbon structural steel alloys.
Follow this engineering specification protocol when submitting Request for Quotations (RFQs) to Chinese rack manufacturers to ensure flawless structural calculations and quick project delivery.
Answers to common structural, financial, and logistical questions regarding customized warehouse rack manufacturing in China.
From light-duty boltless picking racks to heavy cantilever long-goods storage and multi-level structural platforms, Guake provides turnkey equipment manufacturing.







Partner directly with Shandong's leading industrial rack manufacturer. Send us your building floor plan, clear ceiling height, and pallet load dimensions for a complete structural proposal within 24 hours.
Contact Guake Engineering Team →