



Direct factory manufacturing of next-generation radio shuttles, high-bay structural matrices, and modular multi-tier warehousing infrastructure.





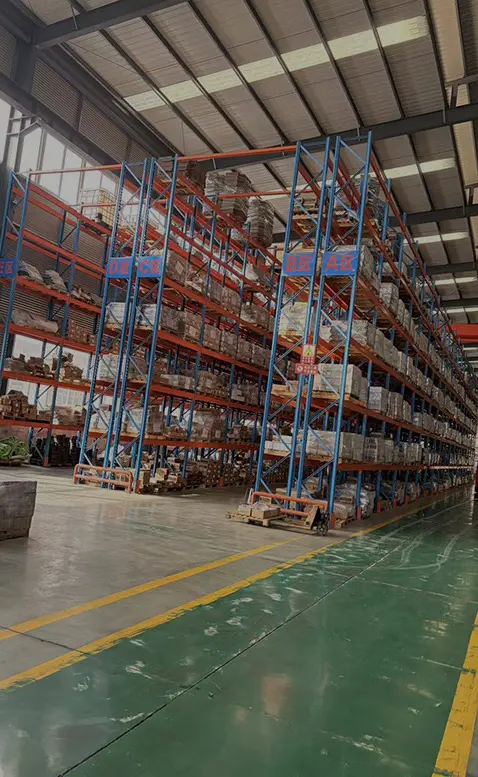
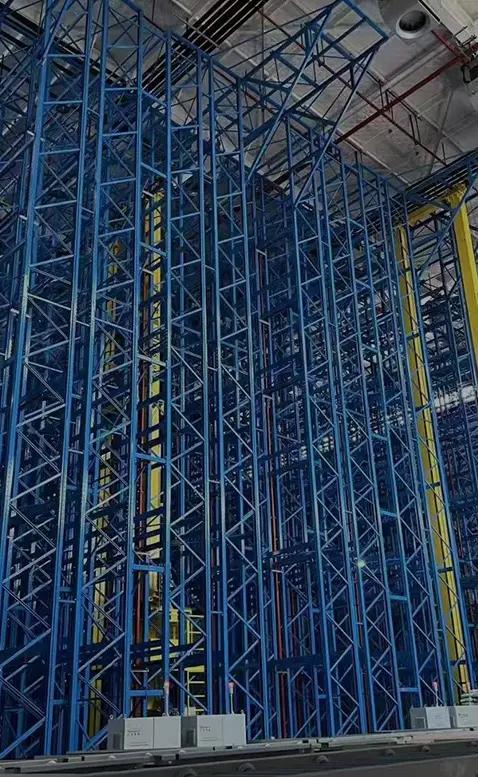
Modern industrial supply chains face unprecedented challenges: surging real estate valuations, labor scarcity, SKU proliferation, and escalating cold-chain operating expenditures. Traditional 2-way shuttle systems and static high-density solutions like drive-in racking often force operational compromises between space utilization and cycle throughput.
As a leading China wholesale manufacturer and turnkey supplier, Guake Logistics Technology introduces advanced 4-way pallet shuttle systems. By combining longitudinal travel and lateral cross-aisle transfer on integrated sub-tracks—assisted by vertical lifters—the 4-way architecture transforms static storage footprints into flexible, fully automated dynamic matrices.
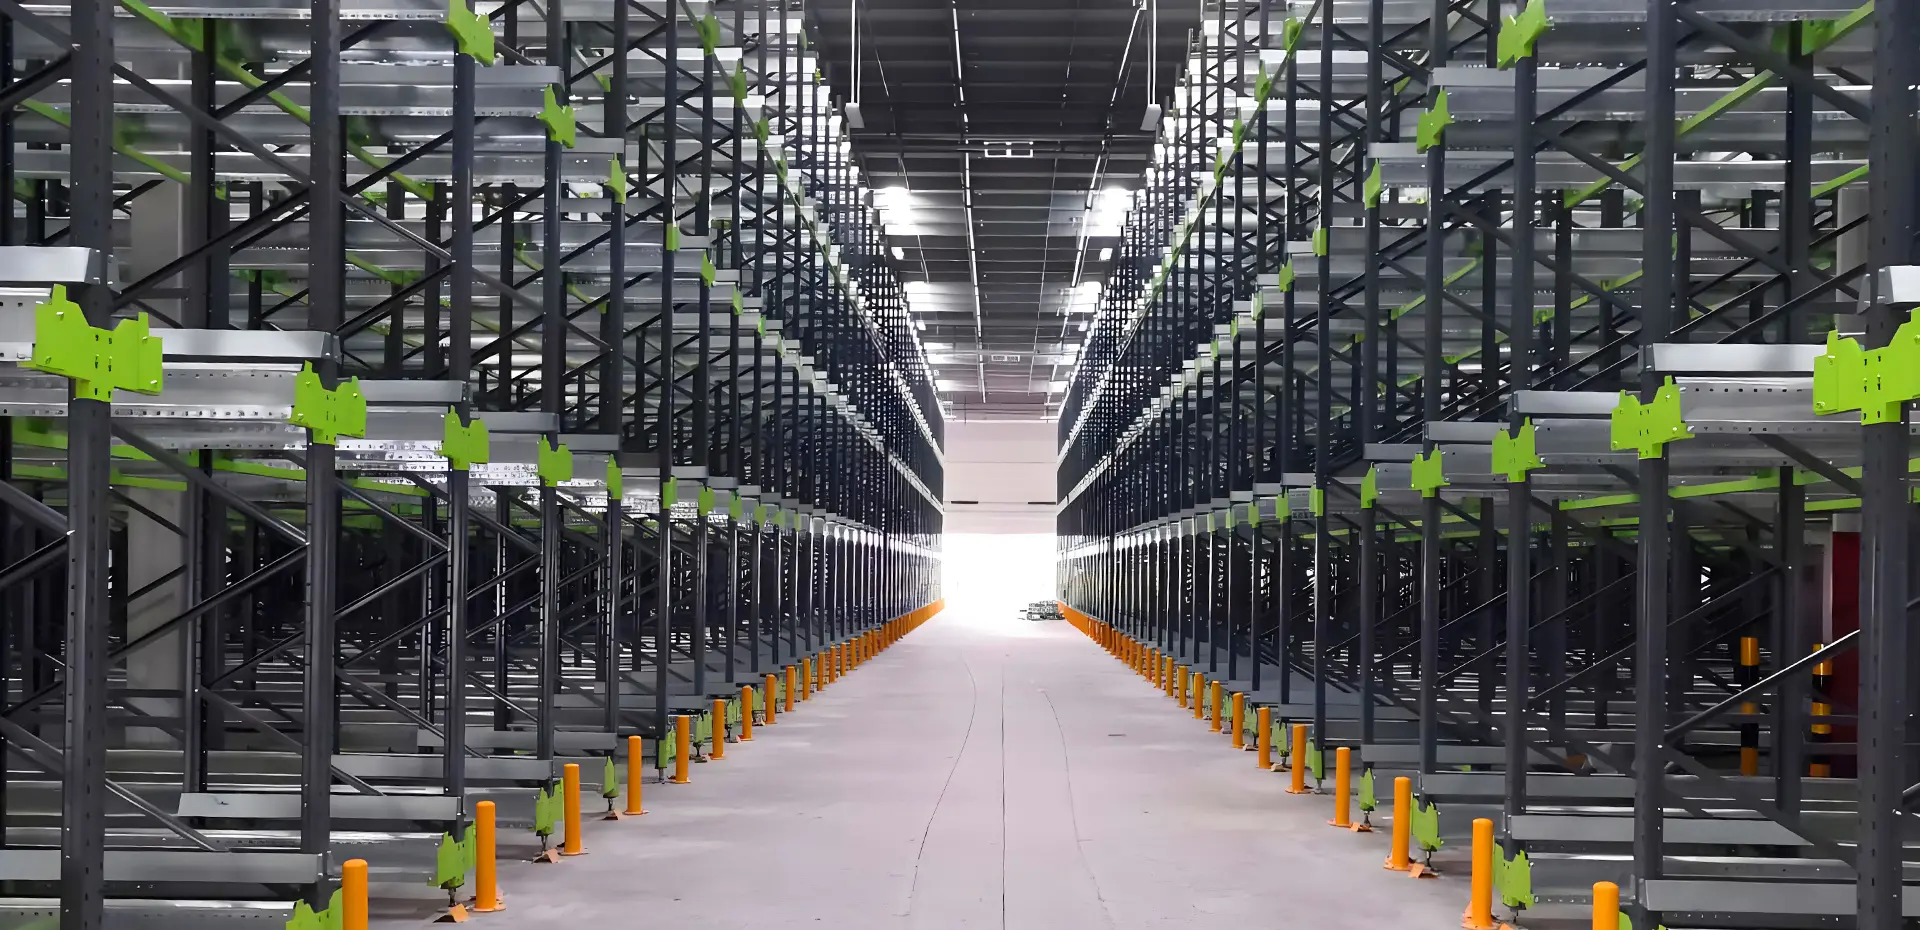
Configured specifically to solve thermal inefficiency, high pick-rates, and irregular building constraints across key economic sectors.
Operating efficiently in temperature zones down to -25°C to -30°C. Minimizes cubic air volume requirements, reduces thermal leakage through dense pack ratios, and protects equipment longevity via low-temp lithium power packs.
Enables accurate sequencing and buffering of components for just-in-time (JIT) assembly lines. The 4-way multidirectional navigation guarantees direct access to distinct palletized components without multi-depth restacking delays.
Handles extreme seasonal peak throughput via dynamic shuttle fleet reallocation. High-frequency algorithms seamlessly adjust between LIFO and FIFO execution to honor expiry tracking and bulk carton batch picking.
A rigorous engineering comparison highlighting volumetric efficiency, access speeds, and operational flexibility.
| Performance Dimension | Guake 4-Way Pallet Shuttle | 2-Way Radio Shuttle | Drive-In Racking | Standard Selective Pallet |
|---|---|---|---|---|
| Volumetric Utilization | Up to 90% (Maximum Floor & Vertical Height) | 75% - 80% (Channel Depth Dependent) | 65% - 75% (Aisle Limited) | 35% - 45% (Aisle Dominant) |
| Dimensional Travel | 4-Directional (X, Y Axes + Vertical Lifter Z) | 2-Directional (X Linear Only) | Forklift-bound Linear Entry | Manual/Forklift 2D Maneuver |
| Inventory Flow Logic | Seamless FIFO & LIFO Concurrent Processing | Restricted to Dedicated End FIFO/LIFO | Strictly LIFO (Risk of Pallet Locking) | Arbitrary / 100% Selective |
| Forklift Rack Intrusion | Zero (Dedicated Input/Output Stations) | Low (Forklift Placed at Channel Faces) | High (Frequent Collision Damage Risk) | Constant Rack Interface |
| Cold Storage Efficiency | Optimal (Minimum Volume, Zero Direct Labor) | High (Limited by Lifter Relocation) | Moderate (High Refrigeration Loss) | Poor (High Wasted Air Volume) |
Ensuring frictionless overseas deployment with strict regional structural code compliance, remote diagnostic capabilities, and robust localized maintenance pipelines.
Every structural upright, support rail, and load beam is calculated according to European EN 15512, American RMI (Rack Manufacturers Institute), and AS4084 standards. Seismic dynamics and soil-load calculations are certified before steel roll-forming.
Equipped with onboard industrial Wi-Fi/5G industrial bus gateways. Real-time fleet telemetry enables predictive maintenance, while regional partner hubs ensure mechanical spare parts dispatch within certified 24- to 48-hour SLAs.
Guake assigns an English-speaking project delivery team overseeing initial CAD/BIM floor layouts, FEA structural stress modeling, factory-acceptance testing (FAT), and comprehensive site-acceptance commissioning (SAT).
Continuous investment in artificial intelligence, ultra-capacitor power systems, and autonomous scheduling protocols.
Transitioning from standard Li-ion chemistry to hybrid supercapacitor architectures. Enables sub-3-minute opportunistic charging cycles directly within the rail channels, achieving continuous 24/7 autonomous operations without battery swapping.
Edge-computing chips mounted directly inside each 4-way shuttle allow vehicles to negotiate route priorities dynamically. Avoids bottleneck traffic jams without constant centralized server polling during multi-tier peak loads.
Direct bidirectional interfaces between physical shuttle hardware and 3D digital twin cloud monitoring. Facilitates remote preventive structural analysis, wear-factor evaluation, and instantaneous simulation of seasonal SKU shifting.
In-depth structural and software engineering guidance to support your automation investment evaluation.
A conventional 2-way shuttle travels only along a single linear rail inside a storage lane. Forklifts are required to physically lift and reposition the vehicle between different aisles or vertical tiers. In contrast, a 4-way pallet shuttle incorporates dual sets of drive wheels oriented perpendicularly. It can drive along cross-aisles without human intervention and interface with vertical lifts to change levels autonomously. This unlocks fully lights-out warehouse automation.
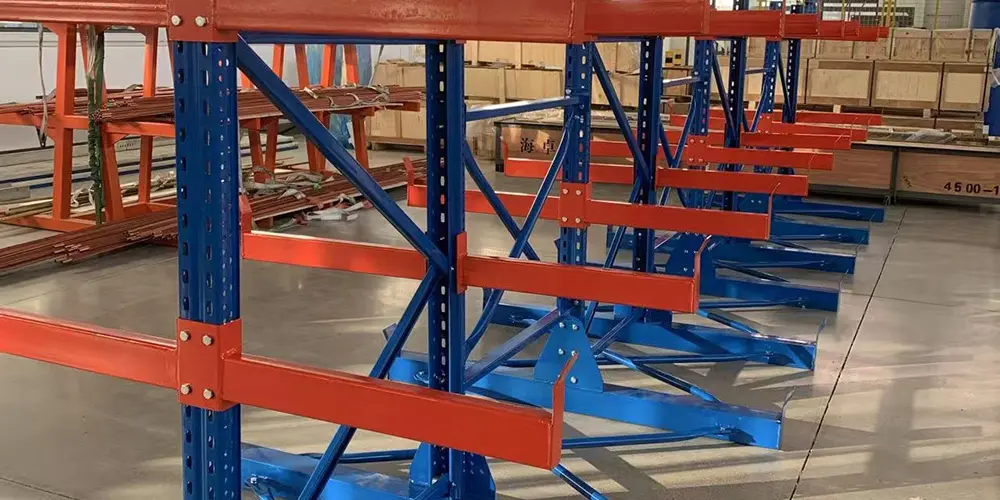
Guake Logistics Technology manufactures a full spectrum of storage equipment: Drive-in racking, Push back racking, Radio shuttle racking systems, Mobile racking, Mezzanine and steel platforms, Cantilever and special-purpose racks, Heavy-, medium-, and light-duty shelving, and structural components for automated storage and retrieval systems (ASRS).
Yes. By providing your facility CAD/PDF architectural drawings, clear clearance heights, pallet dimension matrices (length × width × height), gross unit load weights, handling equipment types, and required throughput cycles/hour, our engineering team will produce an optimized layout complete with static and seismic structural calculations.
Selection depends on throughput and selectivity goals: Drive-in racking offers dense storage at low capital cost for few SKUs, but requires forklifts to enter rack structures. Push back racking stores 2–5 pallets deep per lane with gravity return for intermediate SKU selectivity. Radio shuttle systems eliminate forklift travel inside racks, drastically increasing deep-lane throughput, operator safety, and space efficiency in cold storage environments.
All load-bearing members are manufactured from certified high-tensile hot-rolled or cold-rolled strip steel (e.g., Q235B, Q355B). Structural designs comply with EN 15512 standards for steel static storage systems, FEM 10.2.02, and certified ISO9001 quality management protocols, ensuring load safety under both uniform and seismic dynamic conditions.
Yes. Upright column profile heights, beam section thicknesses and spans, number of structural shelf levels, pallet load capacities per level (from 500 kg to over 2,000 kg per pallet), decking materials (steel decking, wire mesh, or grating), and powder-coated RAL surface color schemes are custom configured for every project.
Original structural platforms, mezzanine solutions, and custom automated storage products engineered by Guake Logistics Technology.
Browse our core industrial line, engineered for scalable load efficiency and long-term durability in high-demand environments.
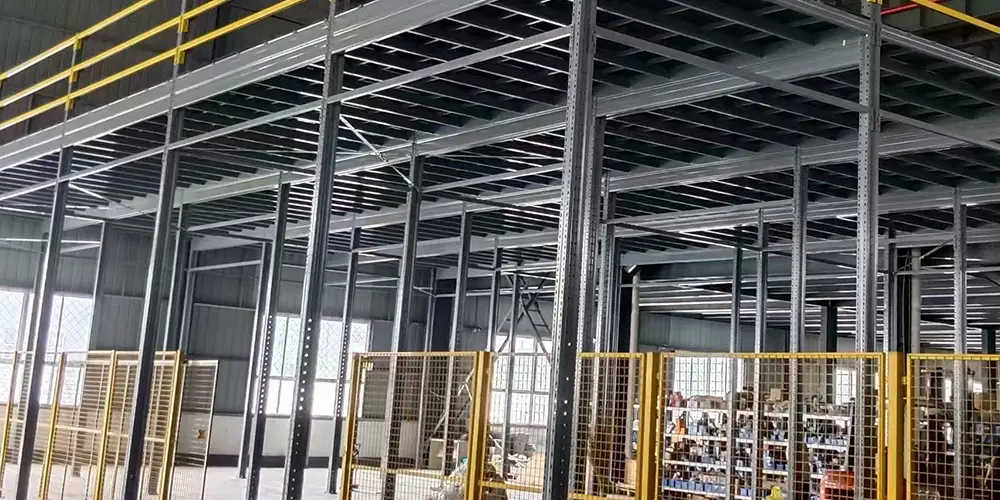





Send your warehouse CAD architectural drawing, pallet specifications, and target throughput metrics. Our engineering team will return a customized 3D design concept and structural calculation analysis.


