


Explore our top-tier heavy-duty storage racks engineered for high stackability, maximum safety factors, and low total cost of ownership across global operations.

Heavy-duty bolted structural steel mezzanine platforms expanding vertical footprint by 200%-300% without structural building expansion.
View Product Technical Specs →
Semi-automated radio shuttle high-density lane storage optimizing bulk handling speed, cold-chain safety, and warehouse volume.
View Product Technical Specs →
Integrated rack-supported multi-tier shelving floors designed for picking efficiency, e-commerce fulfillment, and small parts organization.
View Product Technical Specs →
Maximum-density LIFO pallet storage eliminating aisle space for bulk homogeneous inventory and cold storage operations.
View Product Technical Specs →
Nested cart system storing 2 to 5 pallets deep per lane, delivering dense LIFO storage with high SKU selectivity per lane face.
View Product Technical Specs →
Remote-controlled autonomous shuttle platform running inside deep channels for both FIFO and LIFO high-throughput demands.
View Product Technical Specs →
Motorized mobile bases sliding on floor rails to eliminate static aisles, offering 100% pallet selectivity with maximum space savings.
View Product Technical Specs →
Engineered heavy-duty arm storage solutions designed for long profiles, pipes, timber, steel plates, and oversized industrial goods.
View Product Technical Specs →The modern supply chain ecosystem faces unprecedented headwinds: rapidly inflating commercial warehouse real estate prices, soaring operational labor overheads, and volatile seasonal inventory fluctuations. In response, global enterprise procurement teams and logistics architects are pivoting away from rigid, permanent aisle-bound infrastructure toward modular, flexible storage systems—predominantly **industrial stacking racks** (also referred to as post racks, stackable pallet frames, or portable stacking frames).
Unlike standard selective fixed pallet racking, **wholesale industrial stacking racks** offer dynamic cubic volume utilization. When operational throughput demands spike—such as during agricultural harvest seasons, automotive model changeovers, or e-commerce peak periods—industrial stacking racks can be safely stacked 4 to 6 units high under full dynamic load capacities (up to 2,500 kg per rack). Conversely, when inventory drops, these racks can be knocked down or nested, freeing up valuable floor area for active manufacturing or material handling equipment.
This whitepaper details the structural engineering, metallurgical parameters, supply chain economics, and operational ROI framework for global buyers procuring directly from China’s leading logistics equipment manufacturers, specifically **Guake Logistics Technology (Shandong) Co., Ltd.**
Safety in multi-tier industrial vertical stacking demands uncompromising structural calculations, certified steel selection, and rigorous quality control protocols.
We exclusively source high-tensile structural steel profiles from prime state-owned mills. Q355 structural steel provides a minimum yield strength of 355 MPa, ensuring zero plastic deformation under maximum rated dynamic stacking weight.
Every custom stacking rack geometry undergoes 3D Finite Element Analysis (FEA) simulation. We test vertical deflection, corner cup shear stress, and seismic horizontal sway factor in accordance with FEM 10.2.02 and RMI specifications.
Options include heavy-duty electrostatic powder coating (60-80 microns thickness) for indoor warehousing, or Hot-Dip Galvanizing (HDG per ISO 1461) designed for extreme sub-zero (-30°C) cold storage and humid outdoor yards.
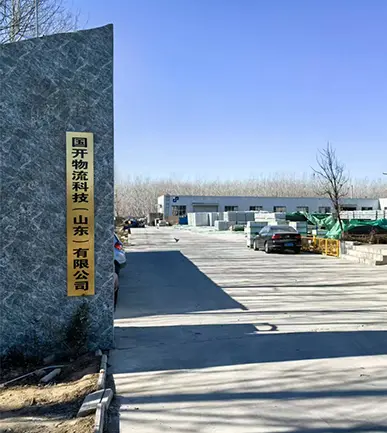
When sourcing **wholesale industrial stacking racks**, structural safety and cost-per-unit metrics dictate global competitiveness. Located in Linyi City, Shandong Province, **Guake Logistics Technology** leverages one of Asia’s largest logistics and raw material manufacturing ecosystems.
Our vertical integrated manufacturing facility mitigates intermediary markups through:
From sub-zero cold storage facilities to automotive stamping plants, our industrial stacking racks adapt seamlessly across global market environments.
Cold storage real estate is among the most expensive logistics assets. Stacking racks eliminate fixed aisles, enabling dense block-stacking of frozen meats, seafood, and dairy products down to -30°C without risk of rack collapse.
Heavy engine blocks, transmission casings, body stampings, and bulk tires require customized cradle attachments and heavy-duty steel base supports to prevent product distortion during multi-tier stacking.
Engineered with built-in spill containment pans and specialized fork pockets, allowing safe dynamic transport and multi-high vertical stacking of 55-gallon steel drums containing raw chemical agents.
Long cylindrical fabric rolls and heavy synthetic carpets are safely stored using customized long-span stacking racks with removable side bars to eliminate crush damage to delicate textile goods.
Heavy 1-ton Flexible Intermediate Bulk Containers (FIBC big bags) containing seeds, grains, or fertilizers can be nested in heavy steel frames, avoiding bag crushing while maximizing seasonal open-yard capacity.
Third-party logistics providers utilize collapsible stacking frames to transform open floor space into high-density storage during seasonal surges, easily folding them down when operations return to baseline.
Comprehensive evaluation matrix comparing structural parameters, selectivity, storage density, and capital expenditure across primary warehouse systems.
| Storage System Type | Cubic Space Efficiency | Pallet Selectivity | Flexibility & Mobility | Sub-Zero Cold Readiness | CapEx (Cost/Pallet Position) |
|---|---|---|---|---|---|
| Industrial Stacking Racks | Very High (85%+) | Lane Dependent (LIFO) | Maximum (100% Portable) | Excellent (HDG Finish) | Low - Medium |
| Selective Pallet Racking | Standard (40-50%) | 100% Direct Access | Fixed (Bolted to Floor) | Good | Low |
| Radio Shuttle Racking | Maximum (90%+) | Deep Lane FIFO/LIFO | Fixed Rack Structure | Excellent | High (Automation Investment) |
| Drive-In Racking | High (75-85%) | Strict LIFO | Fixed Rack Structure | Good | Medium |
| Steel Platform / Mezzanines | Adds Vertical Floor Area | High (Manual Picking) | Semi-Permanent Structural | Standard Indoor | Medium - High |
Global logistics directors evaluating wholesale industrial stacking racks must analyze factors beyond the initial factory FOB unit cost. Calculating the true Total Cost of Ownership (TCO) requires evaluating four critical operational phases:
Inferior non-certified steel profiles or improper wall thicknesses significantly increase structural bending risk under full stack height. Guake enforces a standard safety factor of 1.5x for static loads and 2.0x for dynamic handling impact.
Shipping empty volume is costly. Our engineering team custom-designs corner post attachment sleeves and nesting bases to ensure max weight-to-volume ratio during sea freight, fitting up to 300+ nestable stacking frames per 40ft HQ container.
Damaged corner posts or bent cup bases should be easily replaceable without discarding the entire base assembly. Standardized modular designs lower lifetime maintenance overheads.
The industrial stacking rack sector is evolving with advances in digital asset tracking, autonomous material handling, and sustainable manufacturing.
Integrating ruggedized BLE tags or passive RFID chips into rack base frames allows real-time WMS tracking of inventory locations and stack age within high-density block storage zones.
Designing precision bottom fork guide channels and optical alignment reflectors that allow Autonomous Mobile Robots (AMRs) to dock, lift, and transport heavy stacking frames automatically.
Adopting low-carbon steel profiles produced using electric arc furnace (EAF) technology combined with zero-VOC powder coating formulations to satisfy strict ESG corporate mandates.
Detailed answers addressing engineering parameters, customized manufacturing, shipping logistics, and quality assurance standards.
The maximum safe vertical stack height is governed by the structural load rating of the bottom rack base, column wall thickness, load center of gravity, floor levelness, and seismic zone factors. Under standard engineered configurations, Guake stacking racks support 4 to 6 tiers high when fully loaded (up to 1,500 kg per tier), provided floor slope does not exceed 0.5% grade.
Q235B steel offers a minimum yield strength of 235 MPa, suitable for standard light to medium-duty racking systems. Q355 structural steel provides a minimum yield strength of 355 MPa (~50% stronger), allowing thinner wall profiles while achieving higher dynamic load capacities. This reduces structural dead weight and optimizes sea freight container payload.
Yes. Over 60% of our production volume comprises fully customized racking projects. Our in-house engineering team calculates structural frames based on your exact CAD floor layout, unit dimensions, forklift pocket requirements, side mesh enclosures, and specialized decking materials (such as wire mesh, steel plate, or marine plywood).
For sub-zero cold storage environments (-18°C to -30°C) with condensation moisture risks, Hot-Dip Galvanizing (HDG) per ISO 1461 is recommended. HDG applies a 65-85 micron zinc layer that metallurgically bonds with the steel, preventing rust even if scratched by forklift tines. For standard dry warehouses, electrostatic powder coating provides durable, cost-effective surface protection.
Guake operates under certified ISO 9001:2015 Quality Management Systems and ISO 14001 Environmental Standards. Our products comply with European FEM 10.2.02 racking codes and American RMI safety standards. Every shipment includes raw material mill test certificates (MTC) and factory load test documentation.
Standard production lead time is 15 to 25 days following engineering approval of CAD drawings. Ocean freight from Qingdao Port typically takes 14-18 days to the US West Coast, 28-35 days to US East Coast, 22-30 days to main European ports, and 10-14 days to Southeast Asia.
Select from our comprehensive range of high-capacity storage platforms, heavy pallet racks, cantilever frames, and automated systems.

Heavy-duty structural mezzanine flooring engineered to support 300 to 1,000 kg/m² for expanded upper level storage and picking operations.
View Product Technical Specs →
Autonomous shuttle cart systems engineered for deep channel storage in high-volume distribution centers and cold storage operations.
View Product Technical Specs →
Versatile rack-supported floor structures designed for manual order picking, e-commerce catalog storage, and spare parts management.
View Product Technical Specs →
Classic selective beam pallet racking delivering 100% direct pallet access with fully adjustable vertical beam levels.
View Product Technical Specs →
Unobstructed arm racking designed for fast side-loading of tubing, bar stock, timber, PVC piping, and long structural profiles.
View Product Technical Specs →
Rapid-assembly interlocking steel shelf units ideal for industrial maintenance rooms, retail backrooms, and light inventory storage.
View Product Technical Specs →
Economical shelf storage configured with adjustable dividers for hand-picked small parts, bin storage, and archival boxes.
View Product Technical Specs →
Modular steel shelving designed for high point load capacities, rust resistance, and flexible workspace arrangement.
View Product Technical Specs →Contact our Senior Logistics Engineering Team today. Submit your floor plan (CAD or PDF), unit load specifications, and handling machinery parameters for a complimentary structural layout drawing and direct factory quotation.
