


Explore our precision-engineered warehouse racking components, industrial mezzanine systems, and high-bay automation platforms.








In modern industrial logistics, managing warehousing costs is inextricably tied to cubic space optimization. As global industrial real estate prices escalate, global supply chain directors, logistics 3PL operators, and procurement managers are turning toward multi-tier storage rack architectures. Partnering directly with a verified Wholesale Multi Tier Storage Rack Manufacturer like Guake Logistics Technology (Shandong) Co., Ltd. allows businesses to double or triple usable floor space without expanding their building footprint or taking on massive real estate overhead.
A multi-tier storage racking system (frequently specified as rack-supported mezzanines, multi-level shelving, or structural platform racking) relies on the structural integrity of steel uprights and heavy-duty beams to support elevated walkway floors, staircases, conveyor networks, and automated sorting infrastructure. Unlike standard single-tier selective pallet racking, multi-tier engineered structures demand absolute precision in finite element analysis (FEA), yield-strength steel Selection (Q235B vs. Q355B structural steel), dynamic live-load dynamic resistance, and strict compliance with international building codes.
Guake Logistics Technology has operated out of Linyi, Shandong—China's primary industrial manufacturing and steel processing hub—since 2010. By integrating raw coil slitting, cold-roll profile forming, automated robotic welding, and continuous electrostatic powder coating under one roof, Guake provides tier-one global logistics contractors and OEM distributors with wholesale multi-tier rack systems built directly to EN 15512, FEM 10.2.02, and ANSI MH16.1 structural standards.
Understanding the structural configurations and material choices engineered into Guake's wholesale multi-tier systems.
Utilizes medium- or heavy-duty pallet rack frames as the primary structural support columns for elevated flooring. Ideal for e-commerce picking modules and manual bin storage where high SKU density is required across multiple walkway levels.
Engineered using hot-rolled I-beams, H-beams, and heavy square tubing for wide-span column grids. Designed for heavy machinery, automated sorting conveyors, and bulk pallet staging on elevated levels.
Custom multi-tier frameworks designed for seamless integration with AS/RS stacker cranes, Radio Shuttle carts, AGV robot pathways, and vertical reciprocating conveyors (VRCs).
| System Component | Standard Material Grade | Surface Treatment & Coating | Structural Standard Compliance | Engineering Safety Margin |
|---|---|---|---|---|
| Upright Columns | Q235B / Q355B Cold-Rolled Steel | Electrostatic Epoxy Powder Coating (80-100µm) | FEM 10.2.02 / EN 15512 | 1.65 Structural Safety Factor |
| Load Beams & Joists | High-Tensile Box / Step Beam Profiles | Thermosetting Polyester Powder Coat | ANSI MH16.1 / RMI Guidelines | Deflection Limit: L/200 to L/300 |
| Walkway Steel Decking | Galvanized Steel / Perforated Grating | Hot-Dip Galvanized / Pre-Galvanized (Z120-Z275) | BS EN ISO 1461 / OSHA 1910.28 | Slip Resistance Rating: R10-R11 |
| Staircases & Guardrails | Tubular & Channel Steel Sections | Industrial Safety Yellow (RAL 1023) Coating | OSHA Walkway Standards / EN ISO 14122 | 1.1 kN Handrail Top Rail Load |
Global procurement teams selecting a wholesale multi-tier rack manufacturer must balance engineering reliability with total cost of ownership (TCO). Guake Logistics Technology leverages the unmatched industrial infrastructure of Shandong Province to deliver significant strategic advantages:
Direct supply partnerships with major domestic steel mills (BaoSteel, Shougang) ensure consistent metallurgical quality, full material traceability certificates (MTC), and raw material cost insulation passed directly to wholesale buyers.
Our 20,000m² factory features continuous automatic cold-roll forming mills, 3D fiber laser cutting units, and robotic welding arms that ensure tight dimensional tolerances across complex multi-tier beam connectors and upright columns.
Multi-tier racking systems comprise thousands of steel components. Guake's customized export bundling and protective nesting protocols maximize container space utilization by up to 35%, dramatically lowering ocean freight cost per pallet slot.
Purchasing agents, supply chain architects, and warehousing contractors globally face a changing market environment. Analysis of global multi-tier procurement data reveals several core growth drivers:
Rapid item-level picking and fast order turnarounds require massive floor footprint for bin storage and manual walk aisles. Multi-tier mezzanine racks create vast active picking space above ground-level staging areas, accelerating order processing.
Refrigerated and frozen warehouses incur high cooling energy costs per cubic meter. Installing high-density multi-tier pallet shuttle or push-back systems maximizes thermal storage efficiency and lowers per-pallet operating expenses.
Permitting delays and greenfield facility construction costs encourage companies to upgrade existing structures. Multi-tier rack integration offers a practical approach to modernizing brownfield warehouses without operational disruption.
Deploying a multi-tier storage rack internationally requires adherence to local structural codes, fire safety guidelines, and municipal building permit requirements. Guake provides comprehensive engineering support to ensure smooth local compliance:
Our structural engineering team performs FEA dynamic modal analyses for projects in high seismic regions (e.g., California IBC standards, Eurocode 8, AS4084). Heavy-duty base plates, enlarged anchor bolts, and horizontal/vertical bracing grids are engineered into the final structure.
Fire safety compliance requires open water penetration across multi-tier walkway floors. Guake supplies specialized open-mesh steel grating and perforated floor panels (with >50% open area ratios) fully compatible with Early Suppression Fast Response (ESFR) ceiling sprinkler arrays.
Every wholesale project includes stamped CAD architectural drawings, assembly elevation plans, connection node stress calculations, and structural safety documentation ready for submission to local building inspectors and code officers.
How leading industries deploy Guake's wholesale multi-tier storage racks for optimal operational workflow.
Challenge: Thousands of small-to-medium parts (filters, brake pads, sensors) require high selectivity and organized bin storage.
Solution: 3-Level Rack-Supported Mezzanine with integrated plastic tote shelving on upper floors and bulky tire/exhaust cantilever racking on the ground floor.
Challenge: High seasonal SKU rotation and labor-intensive garment picking demands multi-worker walkway access.
Solution: Multi-tier shelf module with integrated hanging garment racks, center spiral chutes, and powered takeaway belt conveyors.
Challenge: Strictly regulated temperature zones require maximum cubic pallet density and zero floor waste.
Solution: Deep-lane Radio Shuttle Multi-Tier Racking constructed from cold-resistant powder-coated structural steel operating down to -28°C.
Select from our full line of industrial shelving, heavy cantilever storage, boltless modular racks, and custom platforms.







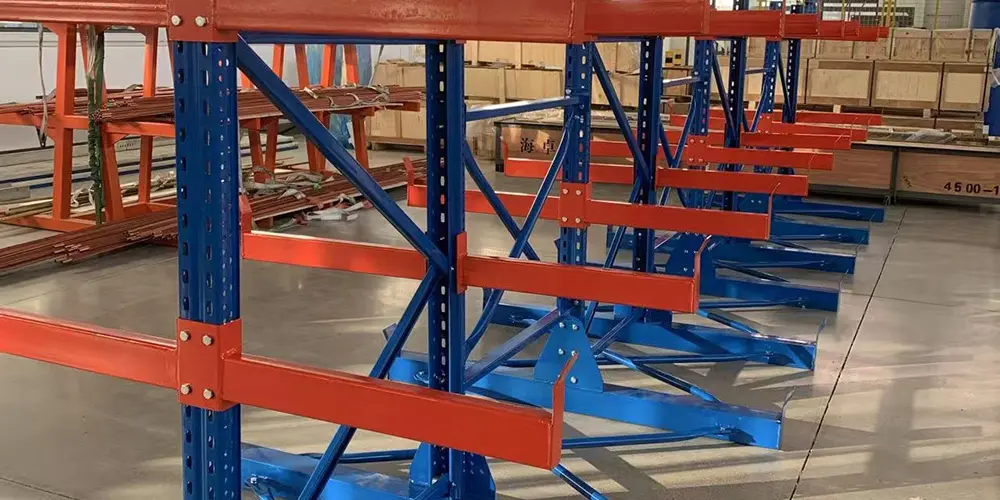
In-depth answers from Guake's chief structural engineers regarding multi-tier storage rack design, factory production, compliance, and logistics.
Contact Guake Logistics Technology (Shandong) Co., Ltd. Send us your warehouse CAD floor plan, floor-to-ceiling clear height, and load requirements. Our structural engineering team will deliver a complete 3D layout plan and factory-direct quotation within 24 hours.
