


Discover high-capacity, engineered warehouse racking frameworks engineered for global distributors, 3PL facilities, and industrial fulfillment hubs.

Eliminates aisles to maximize cubic storage volume for bulk homogenous SKUs and cold storage.
View System Details
Nested cart architecture offering 2-to-5 deep pallet storage with aisle-facing selectivity.
View System Details
Multi-tier structural floor expansion unlocking vertical overhead space without building expansion.
View System Details
Motorized mobile bases traveling on floor rails for 100% pallet access with minimal aisle footprint.
View System Details
Semi-automated deep-lane pallet management utilizing remote-controlled internal shuttles.
View System Details
Heavy-duty cantilever and specialized structural solutions for long, bulky, and irregular materials.
View System Details
Custom heavy-load modular steel platforms manufactured to EN 15512 structural standards.
View Factory Direct
Heavy-load multi-layer steel structural mezzanine systems engineered for industrial plants.
View Factory DirectAs global supply chains face escalating industrial real estate costs, supply volatility, and aggressive fulfillment timelines, enterprise warehouse engineering is undergoing a fundamental transformation. Modern logistics managers are moving away from static pallet storage toward dynamic, high-density, automated racking ecosystems engineered for structural longevity and optimal Total Cost of Ownership (TCO).
Shifting from horizontal spatial expansion to vertical cubic optimization allows warehouses to increase pallet slot capacity by up to 85% within existing footprints.
Direct structural integration with automated radio shuttles, AGVs, and high-bay crane systems dramatically accelerates throughput while eliminating forklift rack collisions.
Adherence to international structural standards (FEM 10.2.02, RMI, EN 15512) verified by Finite Element Analysis (FEA) under dynamic seismic dynamic loads.
Industrial pallet racking has evolved far beyond basic structural steel assembly. In contemporary logistics facility design, a racking layout serves as the physical backbone of an integrated material handling environment. Today's high-capacity storage demands high-yield structural steel coils (such as Q235B and Q355B grades) engineered with cold-rolled beam profile geometry that balances minimal tare weight with structural rigidity.
As enterprise procurement managers evaluate suppliers for high-density racking projects, compliance with rigorous manufacturing standards is paramount. The integration of continuous automated roll-forming lines, robotic welding stations, and automated electrostatic powder coating guarantees structural repeatability and zero-defect beam-to-upright connection tolerances.
Global enterprises purchasing heavy-duty warehouse racking solutions encounter complex international procurement challenges, including raw steel cost fluctuations, shipping container volumetric efficiency, localized seismic building code compliance, and structural installation warranties. Partnering with a direct OEM/ODM manufacturer like Guake Logistics Technology (Shandong) Co., Ltd. streamlines supply chain execution through centralized engineering accountability.
Established in 2010 in Linyi, Shandong, Guake operates over 20,000 square meters of specialized rack production infrastructure. By maintaining complete control over layout drafting, FEA structural calculations, cold roll-forming, surface finishing, and export packing, Guake ensures that overseas projects receive factory-direct wholesale pricing combined with international engineering compliance.
Tailored structural designs aligned with sector-specific operational workflows, throughput velocities, and load dynamics.
A. Cold-Chain & Temperature-Controlled Logistics: Cold storage facilities incur extreme operational overheads per cubic meter. Implementing high-density Radio Shuttle Racking or Motorized Mobile Racking systems dramatically increases pallet storage capacity while minimizing refrigerated volume loss. Fully automated shuttle units operate flawlessly in sub-zero environments down to -25°C, removing human labor from harsh climatic conditions.
B. High-Velocity E-Commerce Fulfillment & Retail Hubs: Rapid order picking demands multi-tier accessibility. Integrated Structural Steel Mezzanines and Rack-Supported Platforms create expansive secondary and tertiary picking floors above ground-level staging areas, optimizing SKU separation without requiring new facility construction.
C. Heavy Industrial Manufacturing & Raw Material Storage: Handling raw steel plates, aluminum extrusions, tubing, and heavy machinery dies requires specialized structural frames. Heavy-Duty Selective Pallet Racks engineered with roll-formed box beams and reinforced Cantilever Arms provide safe, unobstructed access for high-capacity forklifts and overhead cranes.
D. Automated High-Bay Stereoscopic Warehouses (ASRS): For facilities targeting complete digital inventory automation, rack-clad buildings and high-bay ASRS structures utilize automated stacker cranes operating at heights exceeding 30 meters. Precise structural manufacturing tolerances guarantee seamless sensor tracking and continuous 24/7 operation.
Evaluate key structural, operational, and financial metrics across core wholesale racking systems to select the optimal system for your logistics operations.
| Racking Architecture | Storage Density | Pallet Selectivity | Inventory Flow | Operating Forklift Requirements | Ideal Industry Application |
|---|---|---|---|---|---|
| Selective Pallet Racks | Standard (60%) | 100% Direct | FIFO / LIFO | Standard Counterbalance / Reach Truck | FMCG, Multi-SKU Distribution, 3PL Warehousing |
| Drive-In Racking | Ultra-High (85%) | Low (Lane-Based) | LIFO | Reach / Counterbalance (Enters Rack Lane) | Cold Storage, Seasonal Bulk Goods, Homogenous SKUs |
| Push Back Racking | High (75%) | Medium (Lane Face) | LIFO (2-5 Deep) | Standard Forklift (No Lane Entry Needed) | Medium-SKU Batch Storage, Buffer Zones |
| Radio Shuttle Racking | Ultra-High (90%) | Controlled (Automated) | FIFO or LIFO | Standard Forklift + Radio Shuttle Vehicle | Food & Beverage, Cold Chain, High-Throughput Hubs |
| Mobile Racking System | Maximum (95%) | 100% Access | FIFO / LIFO | Standard Reach Truck (Single Mobile Aisle) | High-Value Cold Rooms, Space-Constrained Facilities |
| Steel Mezzanine Platforms | Space Doubling | 100% Surface Access | Multi-Level | Manual Order Pickers, AGVs, Pallet Jacks | E-Commerce Picking, Assembly Plants, Cleanrooms |
Industrial racking safety depends on structural structural calculations, raw material traceability, and continuous quality assurance. As a specialized racking manufacturer, Guake Logistics Technology applies rigorous engineering workflows to ensure structural stability under dynamic live loads, dead loads, and environmental seismic forces.
Every racking layout designed by Guake undergoes FEA stress analysis according to internationally recognized codes:
To resist mechanical abrasion, chemical exposure, and humidity, structural components undergo a multi-stage automated surface treatment process. Components pass through ultrasonic degreasing, zinc phosphate conversion coating, and high-voltage electrostatic epoxy-polyester powder coating cured at 200°C. For extreme outdoor or high-moisture environments, Hot-Dip Galvanizing (HDG) per ISO 1461 provides lifetime rust protection.
Gathering clear ceiling height, slab load ratings, forklift turn radius, pallet dimensions, and throughput requirements.
Conducting finite element stress simulation, beam deflection modeling, and custom structural drawings.
Continuous high-precision cold roll-forming, robotic welding, automated powder coating, and export bundling.
Containerized volumetric packing, complete installation assembly drawings, and remote or field engineering supervision.
Direct technical answers to key questions regarding OEM customization, structural load validation, and overseas project delivery.
Guake Logistics Technology manufactures a complete portfolio of engineered storage equipment, including:
System selection depends on your SKU diversity, inventory turnover rate, and budget:
Yes. Our in-house engineering team provides complete turnkey architectural layout planning free of charge. Simply provide your facility CAD floor plan, clear building height under trusses, floor slab details, unit pallet load dimensions (Width x Depth x Height), total weight per pallet, and forklift model specifications. We provide a full 3D CAD design proposal accompanied by dynamic structural calculations.
Structural integrity is validated at every stage. We utilize certified prime structural steel coils (Q235B / Q355B) verified by material mill certificates. All beam connector hooks and upright profiles are sized using Finite Element Analysis (FEA) software. Furthermore, production strictly adheres to ISO 9001 quality management protocols, and completed systems comply with European FEM 10.2.02 and EN 15512 specifications.
Absolutely. As a direct OEM/ODM manufacturer, every racking system is custom-manufactured. Upright frame heights, frame depths, beam lengths, beam profile gauges, shelf panel deckings (mesh decks, steel plates, or timber), and RAL powder coating colors (such as corporate safety orange, signal blue, dark grey, or yellow) are customized to your exact requirements.
Every international order includes component marking, packaging optimized for container stuffing, comprehensive installation assembly drawings, structural component lists, and step-by-step video installation guides. For large-scale logistics hubs or automated high-bay projects, Guake can dispatch experienced installation supervisors on-site to oversee local installation, testing, and final safety commissioning.
Factory-direct warehouse storage equipment engineered for severe dynamic industrial applications.

High-density deep lane pallet shuttle storage manufactured directly in Shandong, China.
View Product Details
Versatile heavy-duty boltless steel shelving units for light industrial and archive storage.
View Product Details
Arm-supported racking for storing timber, PVC pipes, bars, and long linear inventory.
View Product Details
Rapid-assembly boltless metal shelves ideal for manual order picking and retail backrooms.
View Product Details
Heavy structural beam platforms designed to support heavy machinery or secondary picking floors.
View Product Details
Cost-effective multi-tier shelving solutions optimized for high SKU count hand-picking fulfillment.
View Product Details
Standard high-capacity selective beam racks with adjustable levels for heavy industrial pallets.
View Product Details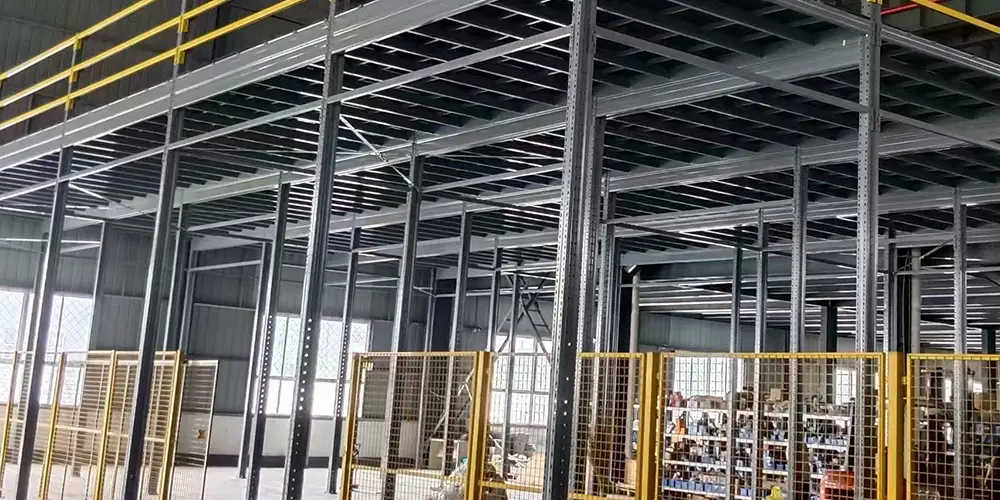
Engineered multi-level structural steel decks supporting 300 to 1000 kg per square meter.
View Product DetailsPartner with Guake Logistics Technology for engineered, factory-direct wholesale racking solutions. Submit your facility dimensions to receive a complimentary 3D layout design and factory-direct price quotation.
