


Engineered to international structural safety standards (FEM, EN, ANSI, AS4084). Discover our factory-direct heavy-duty systems below.

Heavy-duty multi-tier structural steel platforms designed to double or triple usable vertical space for warehouses & industrial facilities.
View Factory Details
Semi-automated high-density radio shuttle pallet systems optimizing FIFO/LIFO storage flow and reducing forklift handling footprint.
View Factory Details
Integrated rack-supported mezzanine shelving solutions customized for manual picking, e-commerce fulfillment, and bulk storage.
View Factory Details
Maximum cubic density racking allowing forklifts to drive directly into storage bays for high-volume, low-SKU inventory control.
Explore Drive-In Racks
Dynamic nested cart technology delivering 2 to 5 deep pallet storage per lane with immediate front-aisle selectivity.
Explore Push Back Systems
Heavy structural steel platforms offering modular, high-load capacities ranging from 300 kg/m² to over 1,000 kg/m².
Explore Mezzanines
Electric mobile bases sliding along floor tracks to eliminate fixed aisles, creating up to 85% higher volumetric utilization.
Explore Mobile Racks
High-efficiency semi-automated storage utilizing wireless lithium-battery shuttles, perfect for extreme cold-chain environments.
Explore Shuttle SystemsIn the era of modern globalized logistics, industrial warehousing infrastructure has evolved far beyond basic static storage. Today’s industrial ecosystem demands high-density, dynamically scalable, and structural safety-certified racking solutions capable of supporting extreme load requirements while streamlining intra-logistics workflows. As real estate development costs surge globally, enterprise logistics managers, 3PL providers, and industrial plant engineers face immense pressure to maximize vertical volume rather than horizontal footprint.
Evaluating potential partner factories requires moving past simple superficial price metrics toward direct technical scrutiny of metallurgical integrity, automated roll-forming accuracy, robotic welding consistency, structural engineering calculations, and strict adherence to global safety codes. Sourcing standard racking systems wholesale directly from tier-one Chinese manufacturers offers a strategic cost-to-performance ratio—provided the supplier possesses comprehensive in-house engineering and production capabilities.
Core Industry Advantage: Guake Logistics Technology (Shandong) Co., Ltd., operating from a modern 20,000+ m² manufacturing complex since 2010, bridges the gap between high-precision cold-rolled steel manufacturing and custom structural engineering for international buyers.
The structural performance of standard racking relies fundamentally on material selection, section geometry design, and precision manufacturing tolerances. Guake standard racking systems utilize high-grade certified cold-rolled structural steel, primarily Q235B and high-yield Q355B grades. These materials undergo rigorous quality verification to ensure uniform yield strength, tensile resilience, and structural elongation parameters.
Under standard industrial operating protocols, beam flexure must strictly conform to a maximum deflection limit of L/200 under full rated safe working load (SWL). Structural calculations incorporate dynamic impact factors, asymmetric pallet placement loads, and unbraced height ratios, ensuring a safety factor exceeding 1.55 in compliance with European FEM 10.2.02 and ANSI MH16.1 design specs.
Selecting the optimal racking system requires evaluating key trade-offs between storage density, direct pallet accessibility (selectivity), throughput speed, and capital equipment expenditure. Below is an engineering comparison matrix designed to guide warehouse procurement directors toward the correct technical design for their facilities:
| Racking Architecture | Volumetric Density | Pallet Selectivity | Stock Flow Mode | Handling Equipment Requirement | Optimal Industry Application |
|---|---|---|---|---|---|
| Selective Pallet Rack | Standard (40-50%) | 100% Direct Access | FIFO / LIFO | Standard Reach / Counterbalance Forklifts | 3PL, High SKU Counts, General Retail Distribution |
| Drive-In Racking | High (70-85%) | Low (Per Lane) | LIFO Standard | Drive-In Counterbalance / Reach Trucks | Cold Storage, Homogeneous Batch Goods, Raw Materials |
| Push Back Racking | Moderate-High (60-75%) | Lane Face Selectivity | LIFO | Standard Forklifts (No lane entry needed) | Buffer Storage, Food Processing, Medium SKU Volumes |
| Radio Shuttle System | Ultra-High (80-90%) | Automated Lane Control | FIFO or LIFO | Standard Forklift + Wireless Battery Shuttle | Cold Chain Logistics, FMCG, Beverage Storage |
| Motorized Mobile Racking | Maximum (85-90%) | 100% Selectivity (1 Aisle) | Flexible | Standard Forklifts + Motorized Rail Base | High-Cost Real Estate, Pharmaceutical Cold Rooms |
| Steel Platform / Mezzanine | 2x to 3x Surface Area | Direct Manual Access | Custom Flow | Staircases, Freight Lifts, Conveyors | E-Commerce Picking, Spare Parts, Integrated Offices |
Industrial storage needs vary significantly across distinct sector environments. A standard racking layout optimized for ambient dry goods retail distribution will fail if deployed without specialized modifications inside a sub-zero cold room or heavy manufacturing plant. Guake provides tailored structural adaptations aligned with specific operational demands:
Utilizes specialized steel micro-alloying to prevent cold embrittlement, combined with radio shuttle or mobile racking to minimize expensive frozen room volume.
Integrates heavy-duty beam profiles, coil cradles, and cantilever arms capable of supporting uneven point loads, heavy dies, and metal sheet bundles.
Combines multi-tier rack-supported mezzanines with pick-module walkways, integrated gravity flow tracks, and automated chute drop-offs for fast piece picking.
Operational safety is paramount in heavy storage environments. Structural failure due to under-engineered steel section sizes, improper floor anchoring, or unaccounted seismic forces can cause severe financial losses and catastrophic site risks. Guake Logistics Technology operates under ISO 9001:2015 quality management procedures, ensuring every manufactured lot meets or exceeds stringent international engineering codes.
Compliance Standards Met: EN 15512 / FEM 10.2.02 (European Steel Racking Design Code), ANSI MH16.1 (Specification for Industrial Steel Storage Racks), AS4084-2012 (Australian Steel Storage Racking Code), and relevant local seismic acceleration coefficient standards.
Every project delivered by Guake includes clear structural calculation reports detailing frame buckling analysis, beam shear and moment limits, floor slab point-load calculations, anchor bolt tension values, and dynamic sway resistance. Furthermore, upright protectors, heavy-duty frame end-guards, and safety mesh backings are integrated as standard options to protect structures against forklift impacts.
The future of industrial storage lies in the seamless convergence of static structural steel with dynamic warehouse automation and digital IoT monitoring. Standard racking is no longer an isolated asset; it serves as the physical backbone for robotic operations.
Guake’s technical engineering roadmap is focused on developing hybrid racking systems engineered for high-precision interface with Autonomous Mobile Robots (AMRs), Automated Guided Vehicles (AGVs), and Automated Storage and Retrieval Systems (AS/RS). By manufacturing high-tolerance rack structures with integrated optical reflector locations, laser positioning targets, and smart load-cell sensors, enterprise operators can transition from standard manual storage into fully automated digital warehouse operations seamlessly.
Explore our complete manufacturing spectrum for heavy, medium, and specialized warehouse storage needs.

Engineered column-and-arm systems designed specifically to hold long materials, pipes, steel bars, and timber securely.
View Special Racks
Standard heavy-duty pallet racks with adjustable beam positions, load capacities reaching up to 4,500 kg per level.
View Heavy-Duty Racks
Freestanding adjustable arm racking systems optimized for light-to-medium long goods, plastic tubing, and aluminum profiles.
View Cantilever Racks
Heavy-duty riveted boltless steel shelving units engineered for maintenance workshops, tool storage, and industrial garages.
View Garage Shelving
Quick-assembly modular metal shelving systems utilizing drop-lock keyhole slots for rapid setup without hardware.
View Boltless Shelving
Versatile steel shelf units designed for hand-pick operations, small parts bins, and light commercial storage needs.
View Multi-Layer Shelving
Custom structural H-beam platforms designed for high deck load capacities, integrated stairways, and safety railings.
View Structural Platforms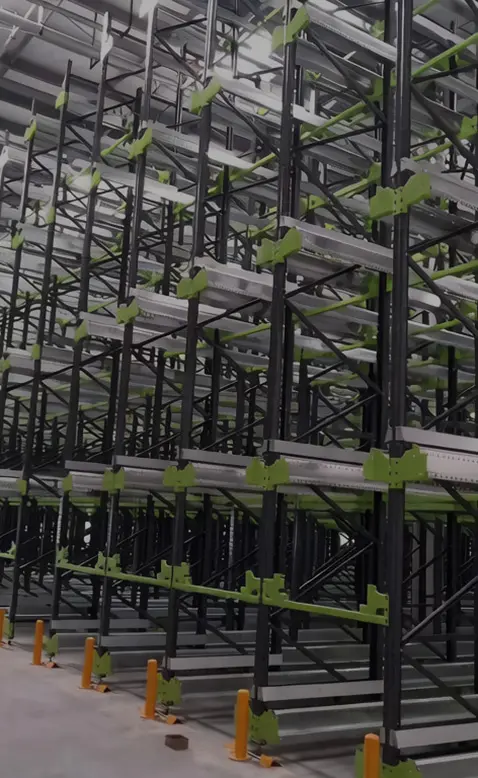
High-bay automated channel racking utilizing intelligent shuttles to maximize warehouse volume and operational throughput.
View Shuttle RacksIn-depth engineering answers to common technical queries raised by global logistics planners and structural engineers.
