


Explore our flagship heavy-duty storage solutions engineered for logistics hubs, cold storage, manufacturing plants, and e-commerce distribution centers.

Semi-automated deep-lane pallet storage powered by remote-controlled battery shuttles for maximum warehouse volume utilization.
View System Specs
Heavy-duty structural steel platforms converting clear vertical ceiling space into multi-level operational work floors.
View System Specs
Rack-supported multi-tier shelving floors designed to maximize square footage for manual order picking and small parts inventory.
View System Specs
High-density LIFO pallet storage eliminating aisle gaps, tailored for uniform bulk goods and cold room storage operations.
View System Specs
Nested cart dynamic racking allowing 2 to 6 pallet deep storage per lane while maintaining fast aisle accessibility.
View System Specs
Custom-engineered bolt-together mezzanine structures providing flexible heavy-duty load capacities up to 1000kg/m².
View System Specs
Motorized mobile pallet racks mounted on floor rails, compressing storage footprints by creating a single moving operational aisle.
View System Specs
Intelligent semi-automated warehouse solution supporting both FIFO and LIFO inventory rotation with minimal forklift collision risk.
View System SpecsAnalyzing the macro trends, economic drivers, and structural engineering advancements shaping the international wholesale industrial shelving market.
Global logistics and supply chain networks are confronting unprecedented cost pressures driven by rising commercial real estate values, surging industrial land rents, and stringent municipal zoning restrictions. According to global logistics real estate benchmarks, industrial warehouse leasing costs across North America, Western Europe, and East Asia have escalated significantly over the past decade. Consequently, logistics managers and plant directors can no longer justify horizontal facility expansion.
The primary paradigm shift in modern warehousing is clear: maximize volumetric utilization (cubic meter storage density) while maintaining flexible throughput speed. Achieving this target requires moving beyond generic static steel shelving toward precision-engineered structural industrial racking systems, custom multi-tier mezzanines, and semi-automated high-density configurations.
Warehouse efficiency is governed by the structural tension between Storage Density and Pallet Selectivity. Selective pallet racking offers 100% immediate selectivity but consumes up to 60% of floor space in dedicated operator aisles. Conversely, Radio Shuttle and Drive-In racking achieve up to 85% floor space utilization by collapsing aisles into continuous structural storage channels. Choosing the optimal wholesale manufacturer guarantees structural safety margin (FEM/RMI standard compliance) while cutting cost per pallet position by 30% to 50%.
Guake Logistics Technology (Shandong) Co., Ltd. implements rigorous finite element analysis (FEA) and international structural codes to ensure complete load integrity.
We source certified premium cold-rolled steel coils (Q235B and Q355B structural grades). Upright columns feature continuous multi-bend roll-forming profiles with structural ribbing to increase load-bearing rigidity while minimizing dead weight.
Components undergo an automated 9-stage pre-treatment wash, phosphatizing, and electrostatic epoxy powder coating cured at 200°C. Optional hot-dip galvanizing provides complete resistance against severe sub-zero cold storage condensation.
Every engineering layout undergoes structural verification using Finite Element Analysis (FEA). Beam connection locks utilize 3 to 4-claw structural safety pins, satisfying FEM 10.2.02, EN 15512, and ANSI/RMI MH16.1 seismic displacement rules.
A side-by-side engineering evaluation for warehouse planners and procurement directors specifying wholesale industrial racking systems.
| Racking Architecture | Storage Density | Pallet Selectivity | Inventory Flow | Ideal Industry Application | Structural Load Rating |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (40-50%) | 100% Direct Access | FIFO / LIFO | 3PL Warehousing, FMCG, High SKU Retail | 1,000 - 4,500 kg / Level |
| Drive-In Racking | Very High (75-85%) | Low (Per Lane) | LIFO | Cold Storage, Seasonal Stock, Bulk Goods | 1,000 - 1,800 kg / Pallet |
| Push Back Racking | High (65-75%) | Medium (2-6 Deep) | LIFO | Food & Beverage, Staging Zones, Medium SKUs | 1,000 - 1,500 kg / Cart |
| Radio Shuttle System | Ultra High (85%+) | Semi-Automated | FIFO or LIFO | Pharma, Frozen Foods, High Throughput Hubs | 1,500 kg / Pallet Position |
| Motorized Mobile Racking | Ultra High (80-90%) | 100% On-Demand | FIFO / LIFO | High-Cost Land, Cold Storage Vaults, Document Storage | Up to 24,000 kg / Bay |
| Mezzanine & Platform | Doubles Floor Area | Manual / Conveyor | Flexible | E-commerce Fulfillment, Small Parts, Workstations | 300 - 1,000 kg / m² Floor |
| Cantilever Racking | High (Unobstructed) | 100% Side Access | N/A | Pipes, Steel Tubes, Timber, Aluminum Profiles | 500 - 3,000 kg / Arm |
Tailoring industrial shelving specifications to regional building codes, climate conditions, and operational workflows.
Requirement: Rapid SKU turnaround, forklift driver safety, compliance with ANSI/RMI MH16.1 and local seismic building codes (California seismic zones).
Implemented Solution: Heavy-duty selective pallet racks engineered with teardrop punch profiles, heavy-column baseplates, structural column protectors, and wire mesh decking to maximize overhead fire sprinkler water penetration.
Requirement: Extremely high operating energy costs at -25°C require maximum pallet density inside temperature-controlled chambers.
Implemented Solution: Automated Radio Shuttle racking combined with hot-dip galvanized structural steel. The system eliminates interior forklift aisles, preventing thermal loss and protecting workers from sub-zero conditions.
Requirement: High ambient humidity, dusty environments, and multi-category raw material handling in fast-growing manufacturing zones.
Implemented Solution: Multi-tier structural steel platforms paired with heavy-duty cantilever racking for raw steel bar storage. Finished with thermosetting epoxy powder coating resistant to humidity corrosion and mechanical abrasion.
Leveraging Linyi's advanced steel manufacturing ecosystem, automated production lines, and export logistics infrastructure.
Operating out of Linyi, Shandong, Guake Logistics Technology manages raw steel coil procurement, continuous automated roll-forming, robotic welding, surface finishing, and export container packing under one roof. This minimizes intermediary markups and guarantees project delivery schedules.
Our 20,000+ m² facility is equipped with automated CNC punch presses, multi-stage continuous roll-forming lines, and robotic welding arms. Standardized pitch hole accuracy (50mm/75mm adjustment pitch) ensures seamless job-site assembly without field modification.
We provide full engineering CAD structural layouts, 3D visualization, detailed bill of materials (BOM), and step-by-step installation manuals. For large-scale projects, remote video commissioning and field installation guidance ensure zero setup delay.
How physical steel storage architecture integrates with AI, AGVs/AMRs, and automated storage systems (ASRS).
Traditional static racks are adapting to accommodate Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs). Bottom beam clearances, rack leg shielding, and precision guidance trackways are designed directly into structural uprights to enable seamless multi-directional robotic travel.
Next-generation high-bay racking systems feature embedded strain gauges and shock-impact sensors attached to critical load-bearing columns. Real-time telemetry alerts facility operators to accidental forklift strikes or structural load imbalances before failure occurs.
High-bay Automated Storage and Retrieval Systems (AS/RS) are shifting toward "rack-clad" building designs. In these systems, the steel racking matrix itself serves as the structural frame for the building's roof and external side walls, reducing facility construction costs by up to 30%.
Adhering to strict international standards for material composition, weld integrity, and safe load distribution.
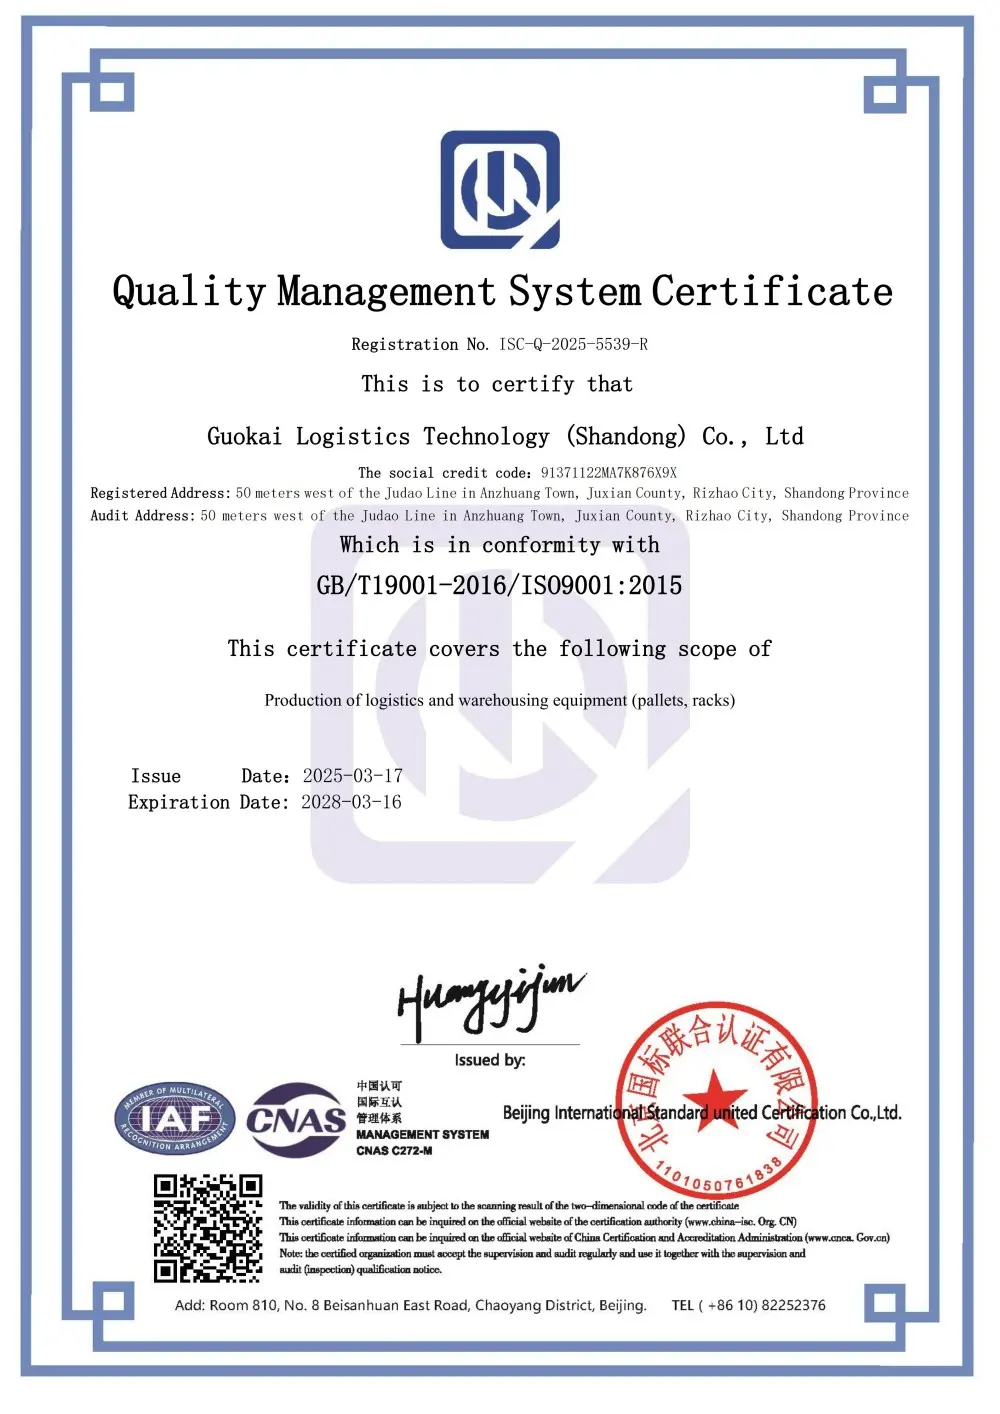
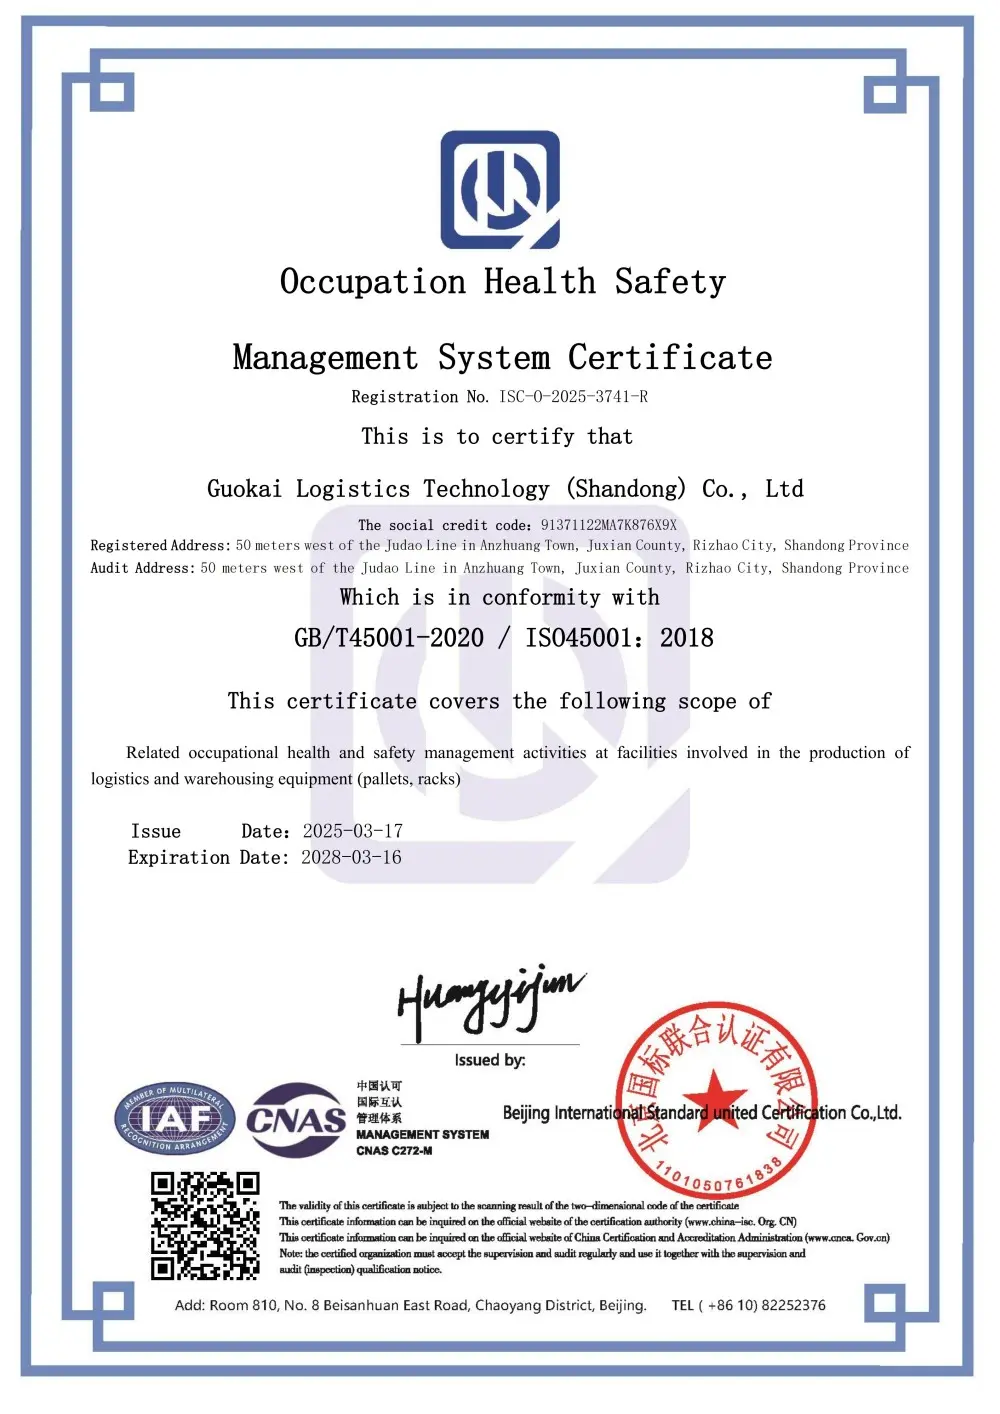
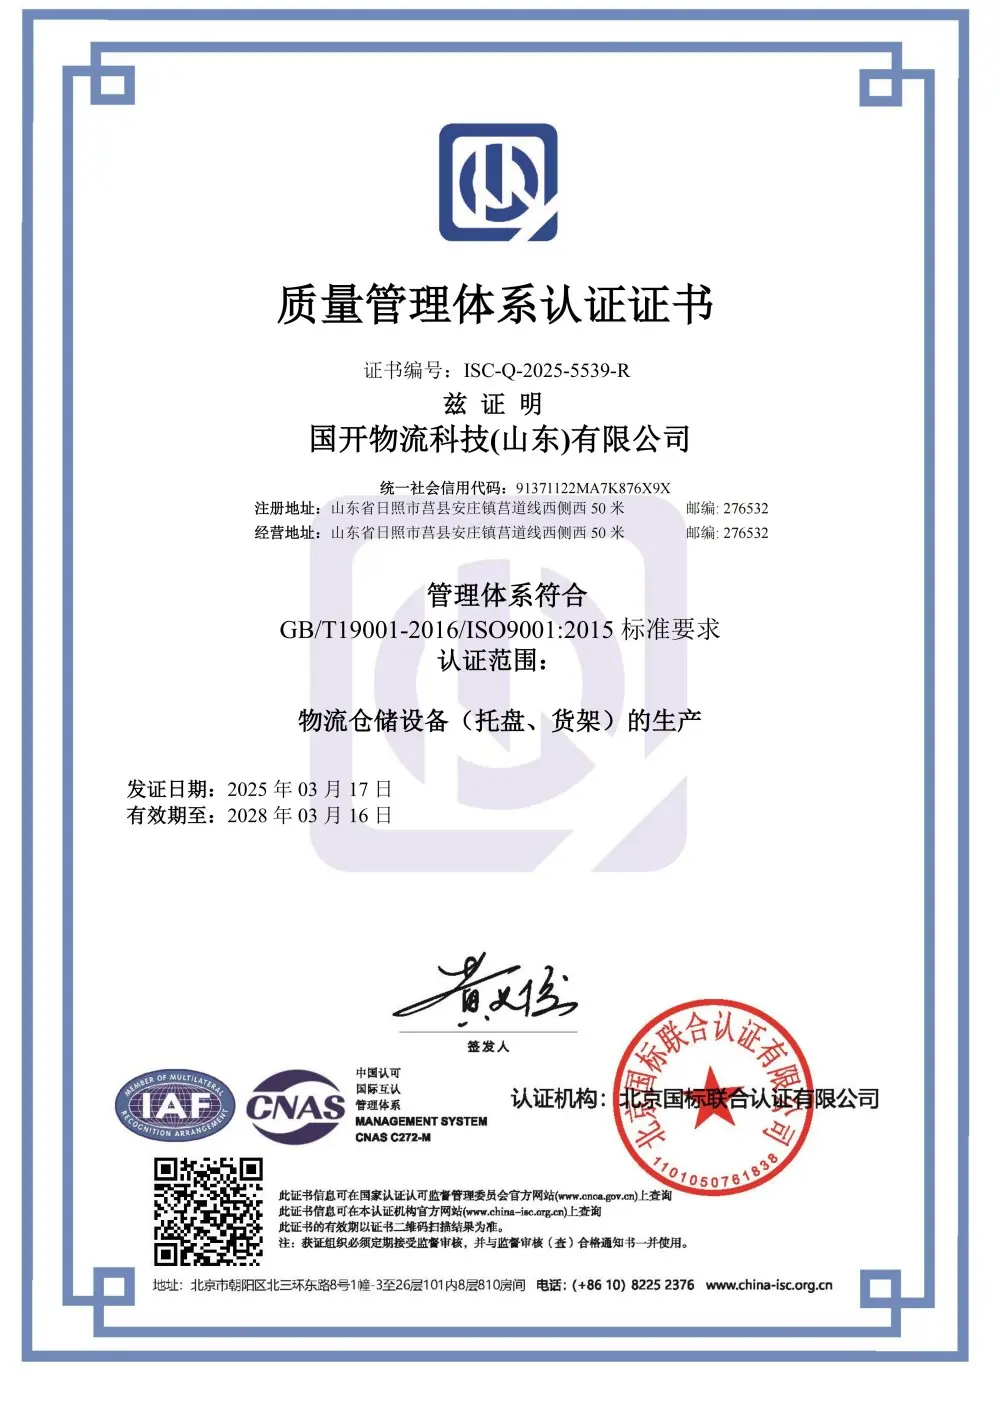
Guake Logistics Technology enforces quality checks at every production stage. From raw material mill test certificates (MTC) to ultrasonic weld inspections and powder coating adhesion tests (cross-hatch testing), our storage products satisfy international standards including ISO 9001 quality management benchmarks.
Explore specialized industrial storage racking, boltless shelving units, and heavy cantilever systems for specialized material handling.

Heavy-duty steel boltless shelving units for commercial garages, workshops, and light industrial storage.
View System Specs
Unobstructed arm storage designed for storing long pipes, aluminum tubing, and timber profiles.
View System Specs
Quick-assembly snap-in boltless steel shelving suitable for high-density manual order fulfillment centers.
View System Specs
Heavy-duty structural mezzanine systems engineered for multi-tier warehouse expansion and office spaces.
View System Specs
Flexible steel shelf units configured for small bin storage, archive document holding, and spare parts picking.
View System Specs
Robust structural steel column and arm racking for extreme load storage of steel coils, beams, and heavy pipes.
View System Specs
Standard selective pallet racks engineered with high-strength beam locks for heavy industrial unit loads.
View System Specs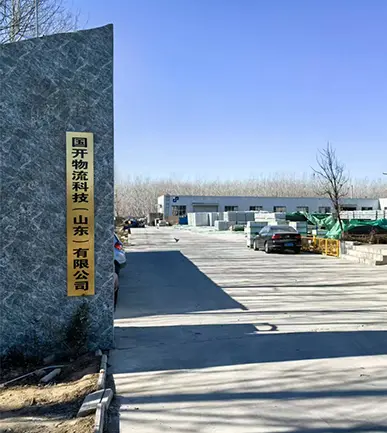
Tailor-made multi-zone industrial racking layouts combining automated shuttle storage, selective bays, and mezzanines.
View System SpecsDetailed engineering and procurement insights answered directly by Guake Logistics Technology engineers.
Guake manufactures a comprehensive range of industrial storage equipment, including:
To receive a free tailored CAD layout drawing and engineered proposal, please provide our technical team with the following project parameters:
Each high-density storage configuration serves specific operational profiles:
All Guake industrial shelving systems are engineered using cold-rolled high-tensile structural steel (Q235B / Q355B). Structural designs conform to European FEM 10.2.02 and EN 15512 standards as well as American ANSI/RMI MH16.1 specifications. Our manufacturing facilities are ISO 9001 certified, ensuring traceable material quality, certified robotic welds, and reliable load safety factors.
Yes. Guake provides complete export container loading services, utilizing specialized bundling and protective wrapping to prevent transit damage. Every shipment includes detailed assembly blueprints, component piece lists, and installation instructions. For international projects, we offer video support or on-site engineering installation supervision.
Contact our structural engineering team in Shandong, China today for expert layout recommendations, structural calculations, and factory-direct wholesale pricing.
Guake Logistics Technology (Shandong) Co., Ltd.
Address: 200 meters west of the intersection of Kunming Road and Xiamen Road, Linyi City, Shandong Province, China
