


Explore structural pallet racking, high-density automated shuttle tracks, and steel mezzanine systems built directly in Shandong, China.

Heavy-duty steel structure platforms designed for multi-tier spatial utilization and mezzanine industrial expansion.
View Platform Specifications
Integrated rack-supported mezzanines providing high floor load capacities (300–1000 kg/sqm) for e-commerce and 3PL hubs.
View Mezzanine Specs
Semi-automated pallet shuttle systems for ultra-dense cold-chain storage and high-frequency bulk cargo logistics.
View Shuttle Specs
Maximum volumetric density storage removing aisle requirements for homogeneous inventory and seasonal goods.
View Drive-In Specs
Nested cart dynamic push-back systems allowing 2-to-5 deep pallet storage per lane with immediate aisle access.
View Push Back Specs
Custom structural steel elevated platforms creating additional floor space for order fulfillment and office expansion.
View Mezzanine Systems
Motorized mobile racking bases eliminating fixed aisles to save up to 85% of warehouse floor footprint.
View Mobile Specs
Fully engineered shuttle tracks with lithium-battery automated shuttles supporting both FIFO and LIFO operational modes.
View Shuttle RackingIn modern logistics engineering, warehouse racking is no longer static metal furniture; it is a structural force-bearing system engineered for physical strain, dynamic impact, seismic stability, and maximum volumetric return on investment.
Procuring wholesale warehouse racking systems requires an intricate evaluation of cold-formed thin-walled steel mechanics, structural connection geometry, dynamic beam deflection standards, and localized floor loading mechanics. As global supply chains transition toward high-bay vertical storage, automated material handling, and sub-zero cold storage facilities, structural specifications dictate facility safety, operational throughput, and capital risk mitigation.
This technical whitepaper outlines the structural parameters, manufacturing standards, material grades, and procurement methodologies for global logistics operators, structural engineers, and supply chain directors sourcing directly from Chinese manufacturing hubs like Shandong Guake Logistics Technology Co., Ltd.
Warehouse racking design must strictly conform to global engineering codes to prevent catastrophic structural failure. The primary international standards governing cold-rolled steel racking specifications include:
Detailed dimensional metrics, steel grades, section modulus attributes, and surface finishing protocols for heavy-duty warehouse racking assemblies.
| Racking Component | Raw Material Grade | Profile Standard Sizes (mm) | Thickness Range | Rated Load Capacity | Key Engineering Feature |
|---|---|---|---|---|---|
| Upright Frames (Columns) | Q235B / Q355B Structural Steel | 80x60, 90x70, 100x70, 120x95, 140x100 | 1.5mm - 3.0mm | Up to 24,000 kg / frame | Omega profile with 11-fold continuous cold roll-formed strength bends. |
| Box Beams (Step Beams) | Q235B Cold-Rolled Steel | 80x50, 100x50, 120x50, 140x50, 160x50 | 1.2mm - 2.0mm | 500 kg - 4,500 kg / pair | Dual-C profile interlocking weld with 3 or 4-hook claw connectors. |
| Radio Shuttle Tracks | Q355B High Strength Steel | Custom C/Z Profile Rails | 2.5mm - 4.0mm | Up to 1,500 kg / pallet | Integrated guide rails for lithium-shuttle alignment with auto-positioning. |
| Steel Platform Mezzanines | Q235B / Q355B H-Beam & Steel Deck | H200/H250/H300 Main Beams | Floor Decks: 2.0-4.0mm | 300 kg - 1,200 kg / sqm | Bolted heavy structural steel beam framing with anti-skid embossed plates. |
| Cantilever Arms | Q235B Heavy C-Profile / Pipe | 100x60, 120x80, 140x90 Arms | 2.0mm - 5.0mm | 300 kg - 1,500 kg / arm | Pin-connected height-adjustable arms for non-palletized long bundle goods. |
| Mobile Racking Bases | Guaranteed Q355 Steel Base Frames | Motorized Rail-Guided Chassis | 4.0mm - 8.0mm Structural | Up to 36,000 kg / trolley | Siemens PLC controlled gear-motor driven movement with laser safety curtains. |
Components undergo a rigorous 7-stage chemical pretreatment wash (degreasing, descaling, phosphating) followed by an automated electrostatic epoxy powder coating ($70\text{--}90\,\mu\text{m}$ thick) cured at 200°C. Hot-dip galvanizing ($60\text{--}80\,\mu\text{m}$) is available for sub-zero cold rooms (-30°C) and corrosive chemical store environments.
Every beam-to-upright connection utilizes automatically engaging spring-loaded safety locking pins that resist accidental forklift dislodgement. Beam claws feature multi-tooth hook engagement (3 to 4 claws) to evenly distribute bending moment forces into column walls.
Our structural design team enforces a maximum beam deflection ratio of $L/200$ under full rated static load. All frame buckling calculations incorporate an overall safety factor multiplier of 1.65 against yield strength based on FEA (Finite Element Analysis) simulation stress testing.
Analyzing warehouse spatial economics, regional procurement priorities, and structural demands across major international logistics hubs.
In North America, high real estate costs drive demand toward VNA (Very Narrow Aisle) selective racking and tall rack-supported structures exceeding 12 meters clear height. Buyers prioritize Teardrop pitch compatibility, high floor slab load distribution, and strict ANSI MH16.1 compliance for insurance and OSHA safety certification.
European logistics hubs across Germany, Netherlands, and Poland mandate EN 15512 design verification. With rapid expansion in cold-chain food distribution and pharmaceutical storage, demand is surging for automated Radio Shuttle systems and Mobile Racking on motorized rails to minimize heated or refrigerated volume consumption.
In the Middle East, Southeast Asia, and Australia (AS4084 standard), logistics giga-projects demand high-capacity heavy-duty pallet racking and custom mezzanine platforms capable of withstanding extreme ambient temperatures, dusty environments, and high seismic dynamic stress factors (UBC Zone 4 design specs).
Why international buyers and logistics engineering contractors choose Shandong direct-factory manufacturing for high-yield steel racking projects.
Located in Shandong Province—one of China's premier heavy industrial steel production centers—Guake Logistics Technology leverages direct supply agreements with premier steel mills (such as ShanSteel and BaoSteel). This ensures immediate access to prime hot-rolled coil stock (Q235B and Q355B grades) with fully traceable Mill Test Certificates (MTC), eliminating raw material middleman surcharges and mitigating global steel price volatility.
Our 20,000 m² facility operates automated multi-stage roll-forming production lines. Continuous cold-rolling machines shape complex column geometries with 11 structural bends, maximizing the section modulus and torsional rigidity while preserving steel molecular integrity. Automated CNC punching dies ensure sub-millimeter hole pitch accuracy (50mm, 75mm, and teardrop centers).
All beam connectors, cantilever arms, and mobile racking chassis components are welded using multi-axis IGM robotic welding stations. Robotic MIG/MAG welding provides continuous, deep-penetration weld seams free of porosity or slag inclusions, guaranteeing structural strength under heavy dynamic forklift impact loads.
By streamlining raw material procurement, fully automating cold roll-forming, and utilizing vertical factory integration in Shandong, Guake delivers export-grade racking systems at a 30% to 40% lower cost per pallet position compared to Western regional manufacturers, without compromising certified load capacity or EN/RMI structural engineering compliance.
Tailored structural rack configurations engineered for specific industry operational workflows and environmental conditions.
Deployment: Multi-Tier Mezzanine Platforms & Heavy-Duty Selective Pallet Racks.
Operational Impact: Combines high-density pallet storage on upper tiers with manual bin picking walkways on lower mezzanine levels. Integrated with gravity flow chutes, barcode scanning walkways, and vertical freight lifts to maximize pick frequency across tens of thousands of active SKUs.
Deployment: Automated Radio Shuttle Racking & Motorized Mobile Racking Systems.
Operational Impact: Cold storage energy costs demand maximum cubic density. Shuttle racking eliminates forklift aisles inside sub-zero chambers, while hot-dip galvanized structural profiles protect steel against moisture condensation, thermal contraction brittleness, and zinc flake oxidation.
Deployment: Heavy-Duty Cantilever Racking & Special Purpose Storage.
Operational Impact: Eliminates front vertical columns, providing uninterrupted linear storage arms for aluminum extrusions, steel piping, timber packs, and sheet metal plates. Arms feature safety retaining end-stops and height-adjustable pivot joint locking pins.
Deployment: Drive-In & Push-Back Pallet Racking (LIFO Flow).
Operational Impact: Tailored for high-turnover batch manufacturing (beverages, packaged foods, paper goods). Drive-in rails support up to 10-deep pallet lanes, cutting forklift travel distance by 50% while maximizing volumetric warehouse cube usage.
In-house engineered storage equipment designed and manufactured in Shandong, China since 2010. Engineered for structural reliability, modular expansion, and long-term operating safety.
Forklifts drive directly into storage lanes to stack pallets on continuous side rails. Eliminates conventional working aisles to deliver extreme volumetric storage density for bulk homogeneous inventory.
Explore Drive In Systems
Pallets rest on nested wheel carts riding along inclined steel channels. When a new pallet is loaded, it gently pushes back existing pallets. Holds 2 to 5 pallets deep per lane with LIFO operational flow.
Explore Push Back Systems
Creates elevated structural steel floor levels over existing warehouse space for order picking, light assembly, carton storage, or office use without expanding the physical building perimeter.
Explore Mezzanine Platforms
Heavy-duty racking banks mounted onto electronically driven motorized bases traveling on floor-embedded steel rails. Opens only one single operating aisle at a time for 100% pallet selectivity.
Explore Mobile Racking
Remote-controlled battery-powered shuttle vehicles transport pallets within deep rack channels. Keeps forklifts outside the rack structure to increase throughput speed and reduce structural damage risk.
Explore Radio Shuttle
Custom-engineered cantilever racks, long-span shelving, and specialized steel fixtures for pipes, steel bars, timber, furniture, roll materials, and heavy non-standard industrial loads.
Explore Special Purpose





Evaluate structural storage efficiency, inventory rotation mechanics (FIFO/LIFO), and investment parameters before finalizing layout blueprints.
| Racking System | Storage Volume Density | Pallet Selectivity | Inventory Flow | Forklift Operating Requirements | Primary Industrial Use Case |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (40-50%) | 100% Immediate Access | FIFO / LIFO (Any) | Standard Counterbalance / Reach Truck | High SKU variety, fast-moving distribution centers, 3PL hubs. |
| Drive-In Racking | Very High (75-85%) | Low (Per Lane Face) | LIFO Only | Standard Forklift drives into rack lanes | Homogeneous bulk inventory, seasonal agricultural stock, cold rooms. |
| Push-Back Racking | High (65-75%) | Medium (2–5 deep lane) | LIFO Flow | Standard Forklift operates at aisle face only | Medium SKU counts requiring high density with fast pallet insertion. |
| Radio Shuttle Racking | Maximum (80-90%) | High (Lane Controlled) | Configurable FIFO or LIFO | Forklift deposits onto shuttle; zero rack entry | Cold storage, food & beverage processing, high-volume manufacturing. |
| Mobile Racking System | Ultra High (85-90%) | 100% (Single open aisle) | FIFO / LIFO (Any) | Reach Truck / VNA operates in open mobile aisle | High floor cost facilities, archival storage, sub-zero cold stores. |
| Steel Mezzanine Platform | Floor Multiplier (+100-200%) | 100% Floor Access | Manual / Conveyor | Stairs, Freight Elevator, Pallet Drop Gate | E-commerce bin picking, packing zones, office space expansion. |
Rigorous raw material testing, structural finite element modeling, and factory audit verifications ensure long-term structural integrity.
Every batch of cold-rolled steel coils received from top steel mills undergoes tensile strength testing, yield point verification, and chemical composition analysis. Full EN 10204 3.1 Mill Test Certificates accompany all wholesale orders.
Custom structural rack layouts are analyzed using advanced FEA software to model column buckling, torsional strain, dynamic seismic loading, and joint rigidity. Structural designs are calculated to withstand localized seismic zone forces (UBC Zone 4).
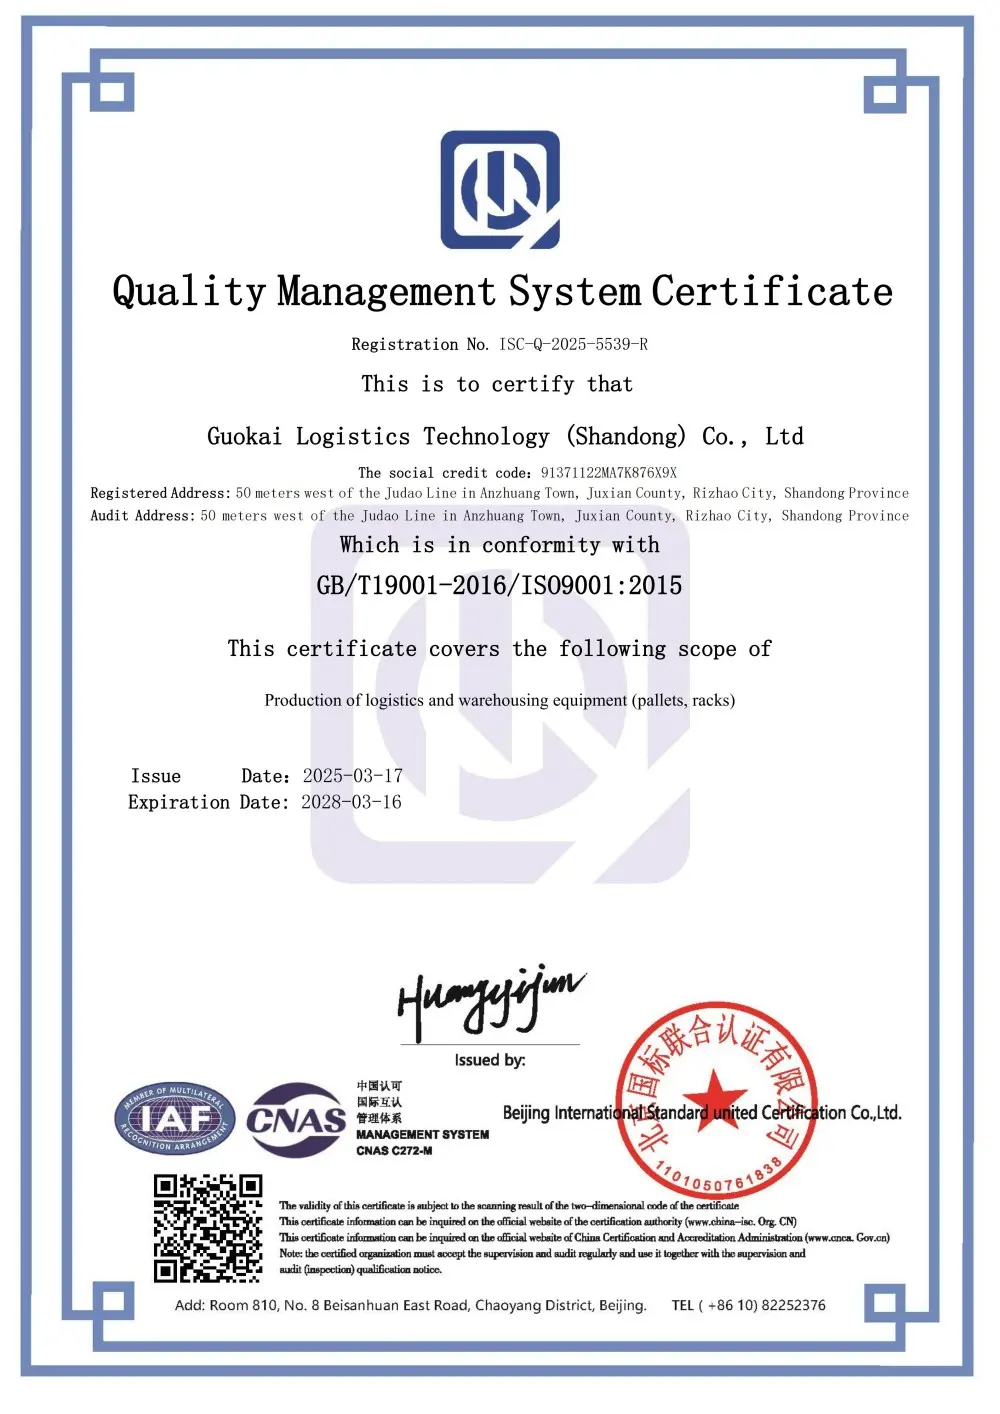
Guake Logistics Technology operates under ISO9001 certified quality management systems. Our structural welding processes, powder coating thickness checks, and dimensional tolerances are verified by independent third-party inspection agencies (SGS / TUV).
Direct technical answers to critical engineering, layout design, structural load calculation, and shipping questions asked by enterprise procurement teams.
Guake Logistics Technology manufactures a comprehensive portfolio of industrial warehousing systems at our Shandong factory, including:
Yes. Our in-house structural engineering team provides complete AutoCAD and 3D layout planning free of charge. To produce a verified structural proposal and load engineering calculation, submit the following site metrics:
Selection depends on your required balance between SKU selectivity, throughput speed, and capital budget:
Yes. Every wholesale project shipped internationally includes comprehensive 3D installation drawings, exploded component assemblies, piece-mark schedules, and step-by-step guidance manuals. For large-scale projects, Guake can dispatch experienced installation engineers or provide remote video commissioning support. Visit our Global Service page for project case details.
Structural safety is controlled through finite element structural modeling, rigorous material grade selection (certified Q235B/Q355B steel), automated continuous cold-roll forming, and strict adherence to FEM 10.2.02 and RMI ANSI MH16.1 design formulas. Frame load ratings include a minimum safety multiplier of 1.65 against structural yield stress under rated design loads.
Absolutely. As a direct manufacturer, every dimension of your racking system is customizable. We tailor upright column height (up to 15+ meters), beam length (up to 4.5+ meters), beam level quantities, decking material (wire mesh, steel plates, wood), upright punch pitch (50mm, 75mm, teardrop), and electrostatic powder coating RAL colors to match your corporate brand identity.
Practical insights from Guake's senior racking engineers on structural density, cold-chain physics, and automation upgrades.
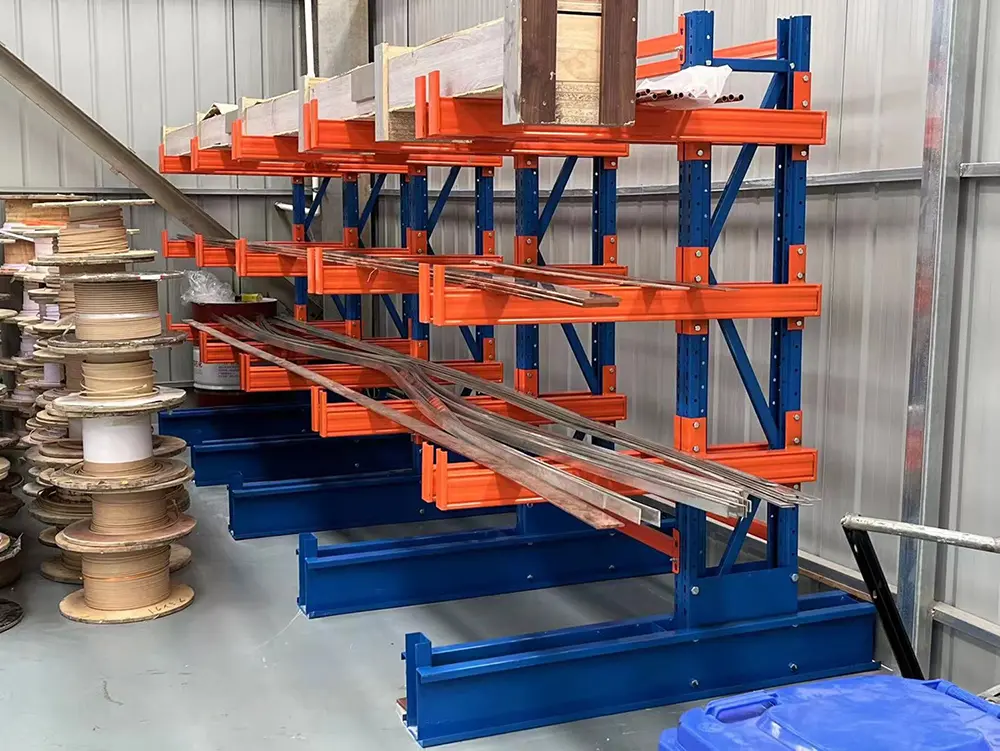
Why modern logistics operators are combining deep-lane dense racking with gravity flow channels to optimize SKU picking speed and volumetric utilization.
Read Whitepaper Article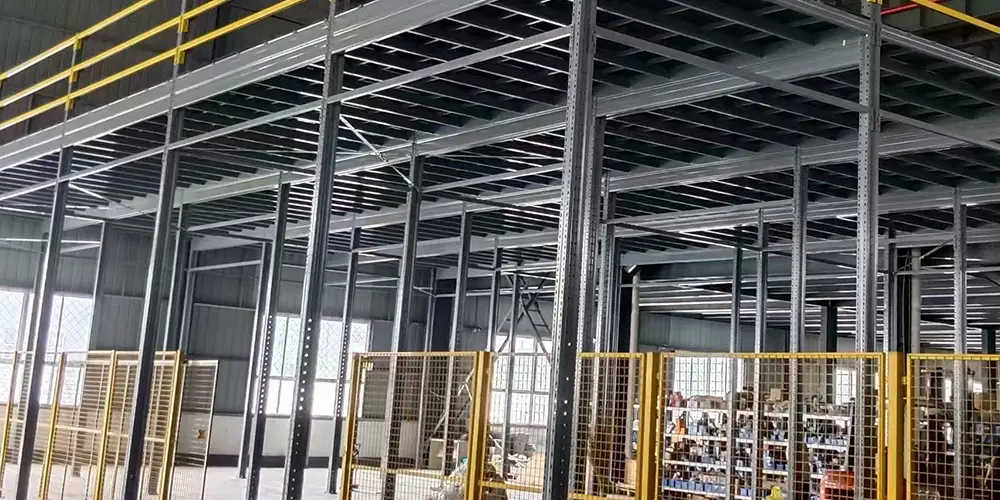
How combining elevated steel mezzanine platforms with heavy cantilever arm racking unlocks vertical floor area without extending physical building perimeters.
Read Whitepaper Article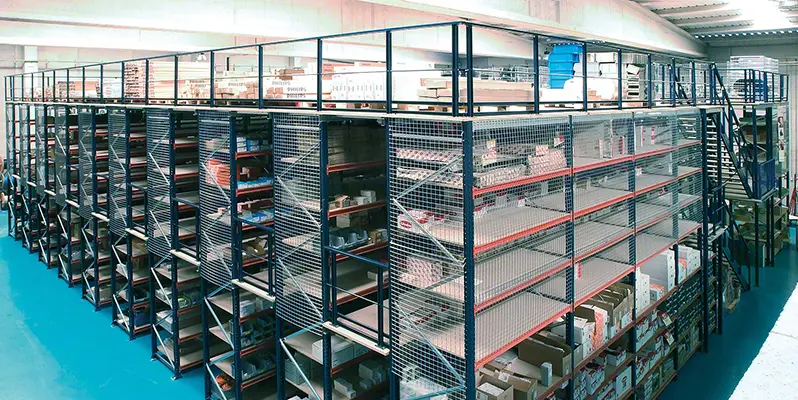
Key structural engineering considerations for steel racking operating down to -30°C, where thermal contraction and sub-zero humidity demand specialized powder coatings and steel grades.
Read Whitepaper Article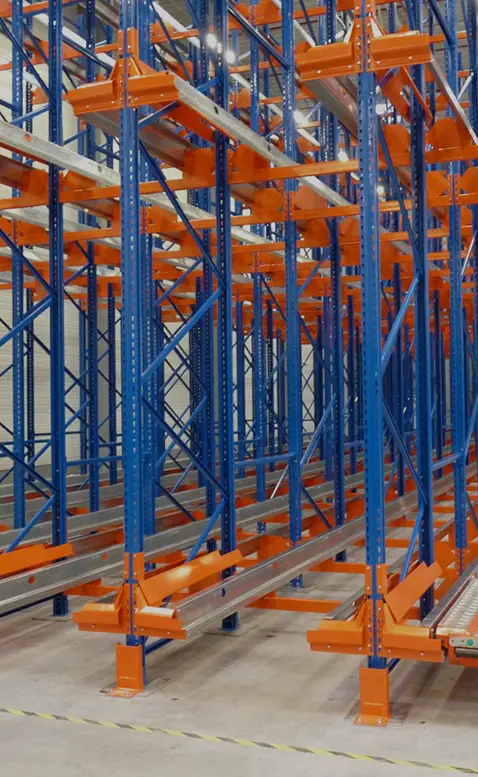
Engineering specialized high-bay roll racking structures for textile rolls, coil inventory, and cylindrical heavy goods utilizing vertical building height.
Read Whitepaper Article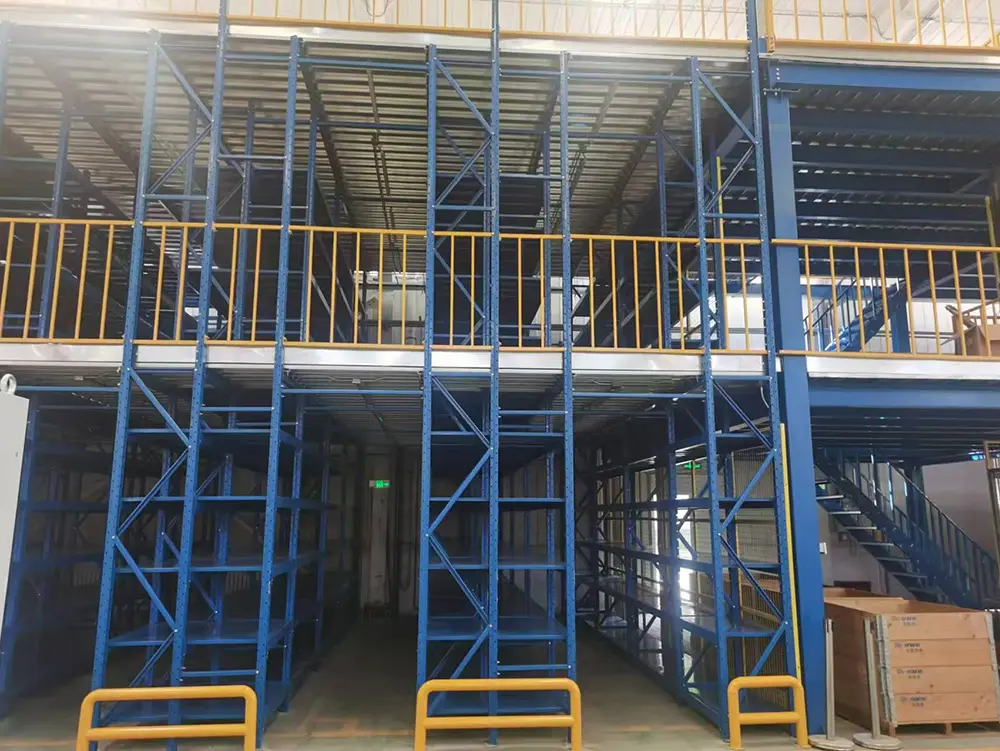
Analyzing box beam profile geometries, connector hook mechanics, and lane depth slope angles for maximum push-back rack operational safety.
Read Whitepaper Article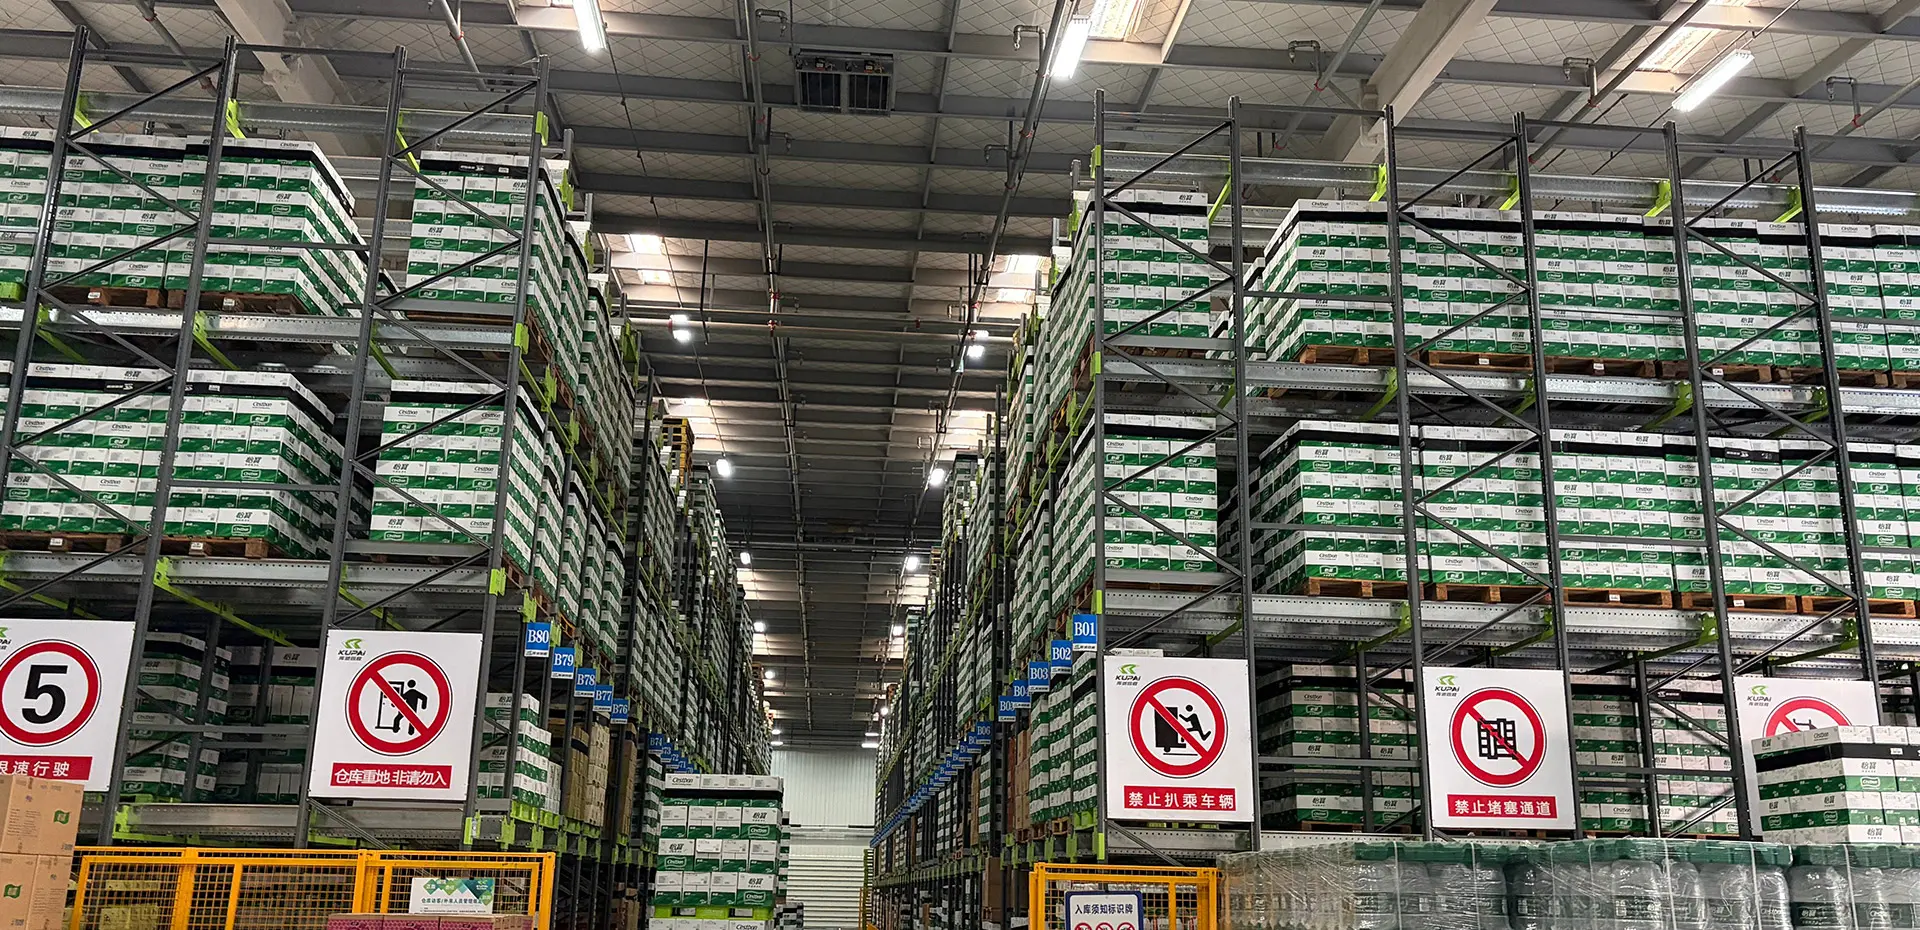
When automated storage and retrieval systems (AS/RS) justify capital investment, and how to execute a phased migration from static racking to automated cranes.
Read Whitepaper ArticleDirect factory wholesale procurement for logistics contractors, racking distributors, and warehouse operators worldwide.
Structural platform racks engineered for maximum floor capacity and vertical space expansion.
Request Platform Quote
Multi-tier rack-supported platforms providing heavy-duty upper floor load capacity.
Request Mezzanine Quote
High-density automated pallet shuttles engineered for deep-lane cold-storage logistics.
Request Shuttle Quote
High-volume LIFO storage system removing interior aisles for maximum volumetric utilization.
Request Drive-In Quote
Dynamic nested cart racking allowing 2-to-5 deep pallet loading per lane.
Request Push Back Quote
Elevated steel platforms creating second and third working floors over existing footprint.
Request Steel Floor Quote
Electrically driven mobile rack chassis eliminating fixed aisles for 100% pallet access.
Request Mobile Quote
Semi-automated shuttle channels built with high-tensile Q355 steel profile tracks.
Request Shuttle Track QuoteConnect with Guake's senior racking engineers in Shandong, China to review floor plans, structural load specs, and container export logistics.
Founded in 2010 in Linyi City, Shandong Province, Guake provides end-to-end warehouse rack engineering—from initial CAD spatial design and structural load calculation to automated factory rolling, container loading, export documentation, and installation guidance.
Factory Address: 200 meters west of the intersection of Kunming Road and Xiamen Road, Linyi City, Shandong Province, China.
Direct Sales Hotline: +86-186 5395 0055
Engineering Inquiry Email: [email protected]
Send your facility DWG/PDF drawings and unit load details to receive an optimized structural layout plan with structural calculations within 24 hours.
