


Factory-direct high-density racking configurations custom-tailored for Qatar's industrial zones and logistics parks.

Multi-tier heavy-duty steel platforms engineered for maximum vertical floor area multiplication in Qatar facilities.

Semi-automated radio shuttle high-density systems optimized for deep lane storage and cold chain efficiency.

Integrated mezzanine shelving platforms utilizing structural columns for high-capacity manual picking zones.

Continuous pallet rails allowing forklifts to drive into lanes, eliminating aisles and increasing cubic density by up to 85%.
Aligning structural warehouse engineering with Qatar National Vision 2030 and local climate dynamics.
Driven by economic diversification initiatives under Qatar National Vision 2030, Doha has transformed into a premier logistics nexus in the Middle East. The expansion of Manateq Logistics Parks—specifically across Ras Bufontas, Um Al Houl, and Al Wukair—alongside the state-of-the-art infrastructure at Hamad Port Logistics Zone, has elevated the demand for spatial efficiency in industrial warehousing.
Warehouse floor space in Doha commands premium financial investment. With ambient summer temperatures frequently exceeding 45°C–50°C and relative humidity levels reaching extreme spikes, the operational cost of climate-controlled, cold storage, and deep-freeze logistics is exceptionally high. Standard selective pallet racking—which dedicates up to 60% of warehouse volume to access aisles—is economically unviable for homogeneous SKU storage.
Custom-engineered Drive-In Racking Systems provided by elite Chinese manufacturers offer the optimal structural solution. By eliminating traditional service aisles, Drive-In systems maximize cubic spatial utilization up to 85%, dramatically reducing the refrigeration footprint and operational energy costs for Qatar’s cold chain operators.
A rigorous breakdown of China-engineered Drive In Racking systems designed for structural safety and heavy loading.
Manufactured from high-grade Q355B steel coil profiles with continuous omega cross-sections. Column widths range from 90mm to 120mm with steel thicknesses up to 2.5mm, engineered according to FEM 10.2.02 and EN 15512 static calculation standards.
Heavy-duty stamped single and double-sided support arms provide rigid cantilever anchoring. Heavy-gauge galvanized pallet guide rails feature tapered entries to facilitate smooth, safe forklift entry and pallet positioning inside deep storage lanes.
Because Drive-In systems lack traditional cross-beams within lanes, structural stability relies on robust top horizontal bracing and rear vertical X-bracing frames. This structural matrix effectively transfers horizontal sway loads safely to the building floor slab.
| Racking Architecture | Cubic Density Efficiency | Access Methodology | Forklift Operation Mode | Best Suited Application in Doha |
|---|---|---|---|---|
| Drive In Racking | 80% - 85% | LIFO (Last-In-First-Out) | Enters structural lanes directly | Cold storage, beverage, chemical batch inventory |
| Selective Pallet Racks | 40% - 50% | 100% Direct Selectivity | Operates strictly in service aisles | High SKU diversity, 3PL retail fulfillment hubs |
| Radio Shuttle Racking | 85% - 90% | LIFO / FIFO Automated | Shuttle car moves deep inside lanes | High-throughput frozen distribution centers |
| Push Back Racking | 65% - 75% | LIFO (2 to 5 pallets deep) | Operates outside at lane face | Medium SKU counts requiring rapid lane access |
How Shandong’s advanced automated manufacturing delivers unmatched quality, structural integrity, and cost savings to Qatari EPC contractors.
Our state-of-the-art manufacturing facilities in Shandong, China, operate continuous automated cold-roll forming production lines, CNC laser cutting stations, and robotic welding cells. Upright profiles and support arms are fabricated with strict tolerances (under ±0.5mm), ensuring flawless bolt alignment during complex on-site installation in Doha.
To withstand Qatar’s saline coastal humidity and high chemical exposure, components undergo rigorous pre-treatment cleaning, phosphating, and automatic electrostatic thermosetting powder coating. The resulting surface finish complies with C4-H / C5-M anti-corrosion standards, preventing rust, flaking, or structural degradation over decades.
By bypassing local trading intermediaries and sourcing directly from established Shandong manufacturing plants, Qatari logistics developers achieve direct procurement cost reductions of 25% to 40%. Direct factory involvement provides structural engineering sign-offs, customized CAD design adaptations, transparent production tracking, and direct container shipping options routed directly into Hamad Port.
Custom engineering applications supporting key economic sectors across Doha and regional Qatari municipalities.
Designed for temperature ranges from -25°C to +4°C in Doha food distribution centers. Maximizes refrigeration density, reduces lost cold air volume, and supports strict LIFO stock rotation for bulk frozen imports.
Heavy-duty load rail engineering capable of supporting palletized resin drums, raw polymers, and industrial chemicals in Mesaieed and Ras Laffan industrial complexes.
High-density storage for seasonal goods, fast-moving beverages, and high-volume retail stock supplying major hypermarket networks across Metropolitan Doha.
Ensuring full adherence to Qatar Civil Defence Department (QCDD) fire safety codes and floor slab stress requirements.
Drive-In racking layouts intended for Doha warehouses undergo rigorous review to ensure strict compliance with Qatar Civil Defence fire mitigation standards. Engineering designs integrate mandated vertical flue spaces and top clearance distances (minimum 1,000mm from sprinkler heads to pallet tops) to facilitate uninterrupted ESFR overhead fire suppression.
Because heavy pallet loads inside drive-in lanes concentrate high point loads on upright footplates, our structural engineers issue detailed slab punch calculations. We specify enlarged steel baseplates and anchor bolt patterns to ensure floor stress distribution meets local concrete slab tolerances.
Modernizing static drive-in structures into intelligent, IoT-monitored high-density storage systems.
Traditional manual forklift entry into racking lanes. Lowest initial capital cost; ideal for stable, long-term homogeneous stock handling.
Retrofitting drive-in lanes with shuttle rails and battery-operated pallet carts. Forklifts remain outside the rack, eliminating impact damage risk and increasing handling speeds by 40%.
Integrating strain-gauge wireless impact sensors along critical upright columns. Real-time impact logging alerts facility managers of structural damage before catastrophic failure occurs.
Explore our full line of engineered heavy-duty storage equipment, mezzanines, and automated systems.

100% direct pallet selectivity for high-SKU distribution hubs across Qatar.
Nested cart systems storing 2 to 5 pallets deep per lane with LIFO access.

Multi-tier structural floor platforms doubling usable operational surface area.

Heavy-duty racks mounted on motorized bases to eliminate fixed aisles.

Semi-automated deep lane pallet shuttle systems for fast cold-chain operations.

Unobstructed arm storage for long pipes, aluminum profiles, and timber stocks.
Heavy industrial steel platforms designed for overhead storage and office integration.
High-bay automated vertical storage driven by stacker cranes and WMS software.
Expert technical responses to common engineering and purchasing inquiries regarding Drive In Racking imports.
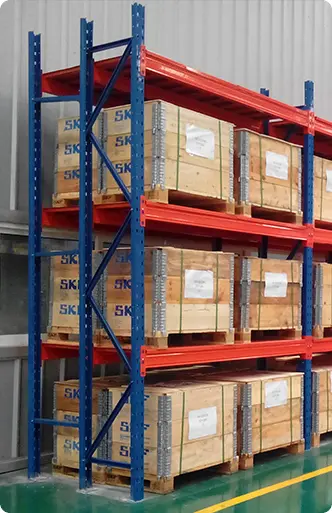
Drive In Racking eliminates internal work aisles by allowing counterbalanced or reach forklifts to drive directly into continuous structural lanes. Pallets rest on cantilevered support rails attached to vertical upright frames. This layout increases volumetric storage utilization from 45% (standard selective racking) to over 80-85%, directly cutting energy overhead per pallet position in high-cost refrigerated warehouses in Doha.
Our Drive In Racking systems are engineered strictly in accordance with European FEM 10.2.02 and EN 15512 static structural calculation codes, as well as American RMI specifications. Uprights are cold-rolled from high-tensile Q355B structural steel, ensuring structural stability under full design loads and resistance against minor forklift impacts.
Components receive an advanced multi-stage pre-treatment wash followed by an automated electrostatic powder coating. The resulting thermosetting epoxy finish provides a durable C4-H to C5-M anti-corrosion layer rated to withstand humidity, saline atmospheric exposure near Doha port regions, and temperature variations without peeling or cracking.
Standard manufacturing timelines range from 20 to 30 days depending on total tonnage. Containerized ocean transport from Qingdao or Shanghai port directly to Hamad Port in Doha typically takes 18 to 22 transit days. We provide comprehensive shipping documentation, origin certificates, and structural calculation reports for seamless Qatari customs clearance.
Yes. Our engineering department develops full 2D CAD floor plans, 3D BIM models, and structural calculation dossiers tailored to your warehouse dimensions, forklift turning radii, slab load ratings, and Qatar Civil Defence Department (QCDD) sprinkler clearance regulations.
Partner with a trusted Shandong racking manufacturer to design, engineer, and import high-density Drive In Racking systems for your Doha industrial facilities.
