

Heavy-Duty Mezzanine Racking & Multi-Tier Platforms
Multi-level structural steel platform systems designed for high-density auto-parts picking, e-commerce hubs, and industrial archives across India.
View Mezzanine Systems


Direct-from-factory high-yield steel platforms, semi-automated shuttles, and custom multi-tier heavy storage solutions designed to optimize high clear-height warehouses.
Multi-level structural steel platform systems designed for high-density auto-parts picking, e-commerce hubs, and industrial archives across India.
View Mezzanine Systems
Deep-lane radio shuttle racking optimized for Indian cold-chain operations, pharmaceutical cold stores, and high-throughput FMCG facilities.
View Shuttle Racking
Heavy-load steel structure platforms engineered to double operational floor space in assembly plants across Pune, Sanand, and Chennai.
View Steel Platforms
Maximum cubic volume storage eliminating working aisles, perfect for homogeneous batch manufacturing and bulk chemical storage.
View Drive-In SystemsIndia is undergoing a structural transformation in logistics infrastructure. Driven by national economic initiatives such as PM Gati Shakti National Master Plan, the National Logistics Policy (NLP), and the Production-Linked Incentive (PLI) schemes, the country's warehousing footprint is transitioning rapidly from unorganized, low-height godowns to modern Grade-A logistics parks featuring 12m to 15m clear heights.
Key industrial corridors—including the Delhi-Mumbai Industrial Corridor (DMIC), the Chennai-Bengaluru Industrial Corridor (CBIC), and major logistics hubs like Bhiwandi (Mumbai), Chakan-Talgawade (Pune), Oragadam-Sriperumbudur (Chennai), Dharuhera-Gurgaon (NCR), and Changodar (Ahmedabad)—demand advanced structural storage equipment capable of withstanding heavy dynamic loads, intense operational duty cycles, and regional environmental stresses.
Key industry indicators driving the demand for specialized racking and heavy structural platforms across Indian industrial corridors:
Generic selective racking fails when handling irregular loads, high-density cold storage, or specialized industrial manufacturing components. Guake engineers purpose-built storage architectures tailored to India’s key industrial sectors.
Serving automotive clusters in Pune (Pimpri-Chakan), Sanand, and Sriperumbudur. We manufacture custom heavy-duty cantilever racks for metal sheet rolls, heavy stamping die storage racks (up to 5 tons per shelf level), and specialized battery module flow systems.
Engineered for major pharma hubs in Hyderabad, Ahmedabad, and Baddi. Smooth, non-porous powder-coated or stainless-steel racking systems resistant to chemical washdowns, humidity, and volatile ambient conditions.
Operating down to -30°C in sea-food and agro cold stores near JNPT Mumbai, Mundra, and Kochi ports. High-density shuttle racking and mobile racking maximize volume, reducing energy consumption per pallet position.
Supporting dark stores and fulfillment centers in Bengaluru, Delhi NCR, and Mumbai. Multi-tier mezzanine structures integrated with gravity chutes, belt conveyors, and high-density carton pick shelving.
Custom storage for steel pipes, aluminum extrusions, long bars, and heavy machinery parts in industrial heartlands like Jamshedpur, Raipur, and Bellary.
When standard catalog dimensions fail your building layout or handling machinery. Tailor-made pitch sizes, beam profiles, color-coded uprights, and dynamic loading specs manufactured precisely to CAD drawings.
When procurement directors and supply chain VPs in India source heavy-duty special purpose racking, evaluating the initial price per bay is insufficient. Real economic value lies in evaluating the Total Cost of Ownership (TCO) over a 15 to 20-year structural lifespan.
By partnering directly with Guake Logistics Technology—an established OEM racking manufacturer with integrated steel roll-forming, robotic welding, and automated surface treatment facilities—Indian enterprises secure a distinct operational and financial advantage:
Unlike commercial grade IS 2062 steel often used in local unorganized fabrications, Guake utilizes certified high-tensile Q355B steel (equivalent to S355JR / ST52-3). This yields a significantly higher strength-to-weight ratio, allowing slimmer structural profiles that handle heavier pallet loads without elastic deformation.
India’s varied environment—ranging from high coastal humidity in Mumbai and Chennai to extreme thermal cycles in Rajasthan and North India—accelerates structural oxidation. Our 9-stage pre-treatment wash followed by 80-120 μm thermosetting epoxy-polyester powder coating guarantees superior scratch and humidity resistance.
Bypassing domestic intermediaries and trading agencies reduces capital expenditure (CAPEX) by 20% to 35%, even after factoring in international sea freight, customs duties, and local port clearance into India.
Our manufacturing process eliminates human margin of error through state-of-the-art continuous cold-roll forming lines and robotic welding workstations.
Uprights feature precise, computer-controlled punching pitch (50mm / 75mm) for effortless beam level adjustability.
Full-penetration robotic welds on beam connectors and baseplates eliminate structural fatigue and localized joint failure.
Certified factory management under ISO 9001, ISO 14001, and ISO 45001 ensures strict quality traceability for every shipment.
India is divided into four seismic risk zones (Zone II to Zone V). High-bay racking structures installed in seismically active industrial areas—such as NCR Delhi (Zone IV), Gujarat (Zone IV/V), or Assam/Northeast (Zone V)—require rigorous structural dynamic modeling.
Guake’s structural engineering team performs computer-simulated Finite Element Analysis (FEA) on racking layouts to ensure dual compliance with both international and Indian engineering codes:
Key structural safety design parameters embedded into Guake Special Purpose Racking systems for Indian installations:
Compare structural profiles, load densities, and operational characteristics to select the optimal racking architecture for your facility in India.
| Racking Architecture | Load Capacity (Per Level/Arm) | Cubic Volume Utilization | Seismic Rating (IS 1893) | Primary Industrial Application in India |
|---|---|---|---|---|
| Heavy-Duty Mezzanine Platform | 300 kg/m² – 1,200 kg/m² | 180% – 250% Space Expansion | Zone II to Zone IV | Auto-component kitting, E-commerce pick modules, Spare parts depots |
| Radio Shuttle Racking | 1,000 kg – 1,500 kg / Pallet | Up to 85% Density | Zone II to Zone V (Custom Bracing) | Cold stores (-30°C), Food & Beverage, FMCG high-velocity SKU distribution |
| Heavy Cantilever Racking | 500 kg – 4,500 kg / Arm | 70% – 80% (Long Goods) | Zone II to Zone IV | Steel pipes, extrusions, timber, copper rods (Jamshedpur / Gujarat industrial belts) |
| Steel Structure Platform | 500 kg/m² – 2,000 kg/m² | 200% Floor Area Double | Zone II to Zone V | Overhead assembly machinery, office mezzanine, heavy industrial processing |
| Drive-In Racking System | 800 kg – 1,200 kg / Pallet | Up to 75% Density | Zone II to Zone IV | Homogeneous batch manufacturing, seasonal chemical bulk storage |
| Automated AS/RS Structure | 1,000 kg – 2,000 kg / Bay | Up to 90% (Vertical Height >25m) | Zone II to Zone V (FEA Modeled) | Smart logistics parks, high-bay automated distribution hubs |
Importing large-scale structural steel equipment into India requires a supplier with deep experience in international freight logistics, customs documentation, and regional Indian site execution protocols.
Guake provides end-to-end support, ensuring zero hassle for Indian procurement teams and plant engineering heads:
Regular containerized shipments (40ft HQ / Open Top for long beams) direct to Nhava Sheva (JNPT Mumbai), Mundra, Hazira, Chennai Port, and Kolkata/Haldia.
Provision of complete shipping manifests, Mill Test Certificates (MTC EN 10204 3.1), Certificate of Origin, and Harmonized System (HSN Code 9403) declarations for smooth Indian Customs clearance under GST framework.
Complete 3D installation CAD assembly manuals, bolt-torque specifications, and remote video commissioning—or dispatched installation supervisors to lead local Indian rigging crews.
Every project delivered to India is accompanied by a transparent engineering documentation file to facilitate local structural safety audits and WDRA (Warehousing Development and Regulatory Authority) warehouse registration:
Direct technical answers for logistics directors, plant managers, and procurement specialists planning racking investments in India.
Guake’s structural engineering department incorporates regional seismic hazard coefficients based on the installation site in India (Zone II through Zone V). We perform Finite Element Analysis (FEA) modeling to determine upright profile thickness, horizontal and diagonal frame bracing patterns, oversized heavy baseplate dimensions, and chemical anchor bolt embedment depths into the warehouse floor slab to ensure total stability during seismic disturbance.
For standard heavy-duty selective or shuttle racking (up to 9 meters height), a reinforced concrete slab of grade M25 or M30 with a minimum thickness of 175mm to 200mm is recommended. For high-bay ASRS or heavy structural mezzanines with point loads exceeding 6 tons per post, M30/M35 grade concrete with fiber reinforcement and a minimum slab depth of 250mm is required. Floor flatness should meet FM2 or TR34 Class 1 specifications for narrow-aisle forklift operations.
Production lead time at our factory typically ranges from 15 to 25 days depending on the structural volume and custom powder-coating specifications. Sea transit time from Qingdao or Lianyungang port to major Indian seaports (Nhava Sheva / JNPT Mumbai, Mundra, Hazira, or Chennai) takes approximately 14 to 20 days. End-to-end delivery from order confirmation to site arrival in India is generally achieved within 35 to 45 days.
Yes. As a direct OEM manufacturer, all structural components—including upright profile geometry, beam length, shelf decking type (steel panel, wire mesh, or particle board), and electrostatic powder coating colors—are 100% customizable. You can specify any RAL color palette (such as RAL 5005 Signal Blue, RAL 2004 Pure Orange, or RAL 7035 Light Grey) to match your corporate branding or warehouse safety zone coding.
Our radio shuttles and steel racking structures are specially engineered for cold environments down to -30°C. We utilize cold-resistant high-tensile steel, specialized low-temperature lithium battery packs, IP65-rated moisture-sealed electronics, and sub-zero synthetic lubricants. This prevents condensation freezing, electronic failures, and metal embrittlement common in standard storage equipment.
We supply a complete export documentation suite, including Commercial Invoice, Packing List (itemized per container), Bill of Lading (B/L), Certificate of Origin, Mill Test Certificates (MTC EN 10204 3.1), and accurate HSN classification (typically HSN Code 9403.20 - Other metal furniture / steel racking) to ensure smooth customs clearance and GST input tax credit claim for Indian importers.
Yes. Every order includes exhaustive 3D assembly CAD blueprints, component identification tags, and installation video tutorials. For large-scale projects (mezzanines, ASRS, or multi-tier logistics parks), Guake can dispatch experienced structural installation engineers to supervise local Indian rigging crews, oversee anchor torque testing, and certify final rack alignment and safety.
All Guake structural steel components (uprights, beams, bracing, and platforms) come with a standard 5-year structural warranty against manufacturing defects. Dynamic components such as radio shuttles include a 1-year electronics and drive warranty. We maintain replacement parts inventory (beams, upright protectors, shuttle motors, and sensors) for rapid air-freight dispatch whenever required.
Comprehensive warehouse storage systems engineered to maximize vertical volume, operational throughput, and structural safety across all industrial sectors.

Nested cart systems operating on inclined rails. 2 to 5 pallet deep LIFO storage with high aisle selectivity.
View Push Back Racking
Semi-automated deep lane pallet storage utilizing wireless battery shuttles. Ideal for high-density FIFO/LIFO warehouses.
View Radio Shuttle
Heavy pallet racks mounted on motorized floor-guided bases. Opens a single working aisle on demand to save 80% floor area.
View Mobile Racking
Custom engineered multi-tier steel mezzanine platforms adding second and third floors for office, picking, or assembly use.
View Mezzanine Systems
Unobstructed arm storage for long, bulky materials including steel pipes, timber, metal profiles, and heavy plastic tubes.
View Cantilever Racking
Standard selective pallet racking with 100% direct access to every pallet position. Fully adjustable beam levels for mixed SKUs.
View Heavy-Duty Racks
Heavy industrial steel floor structures designed for high load capacities up to 2,000 kg/m² for overhead machinery placement.
View Steel Platforms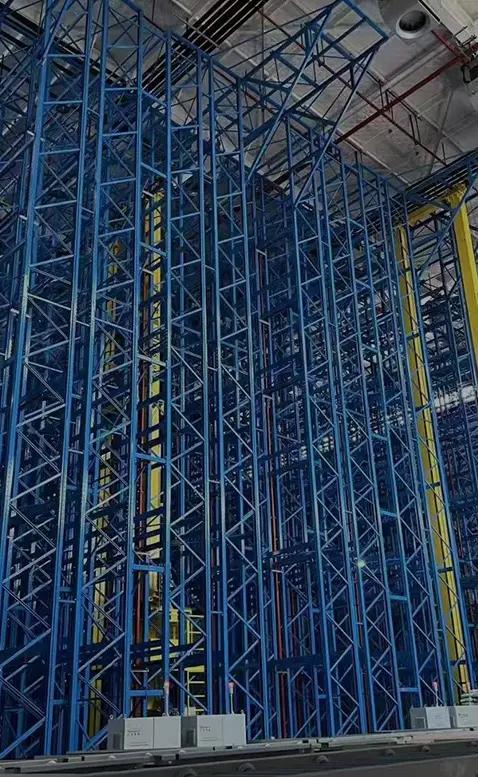
Ultra-high precision high-bay rack structures designed for automated stacker cranes and computerized warehouse management systems.
View AS/RS RackingShare your CAD warehouse floor plan, clear building height, pallet dimensions, and target load capacity with our structural engineering team. Receive a custom 2D/3D layout proposal and direct-factory quotation within 24 hours.